Club Meeting 24 June 2020 Report by : Janet McDonald
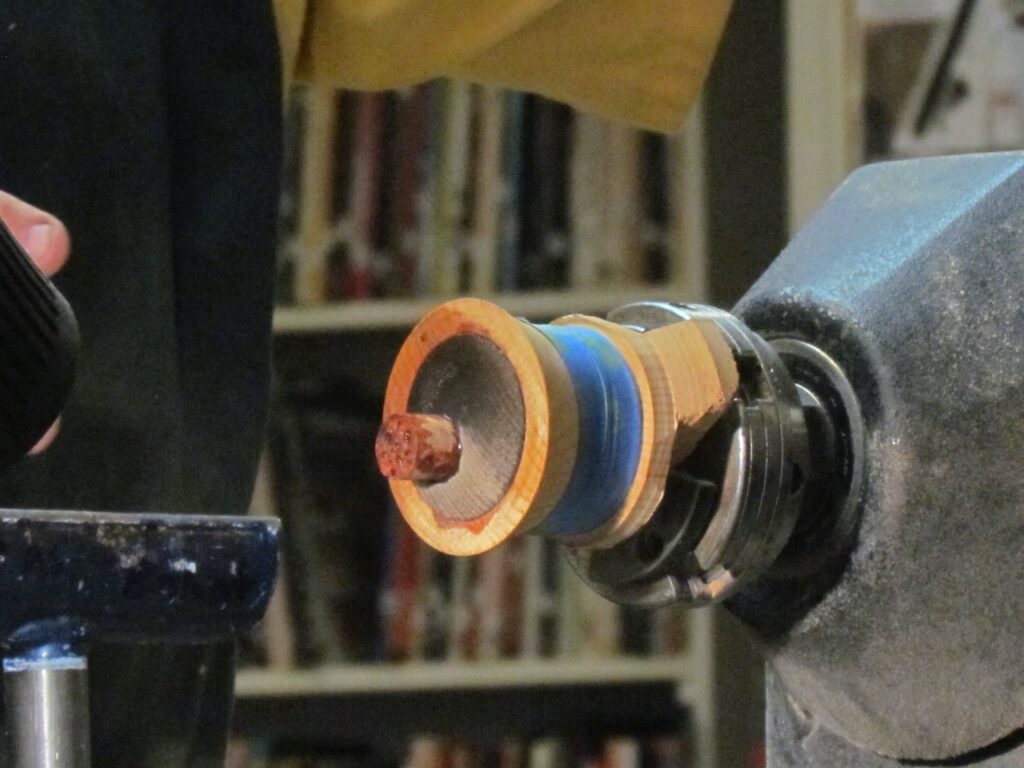
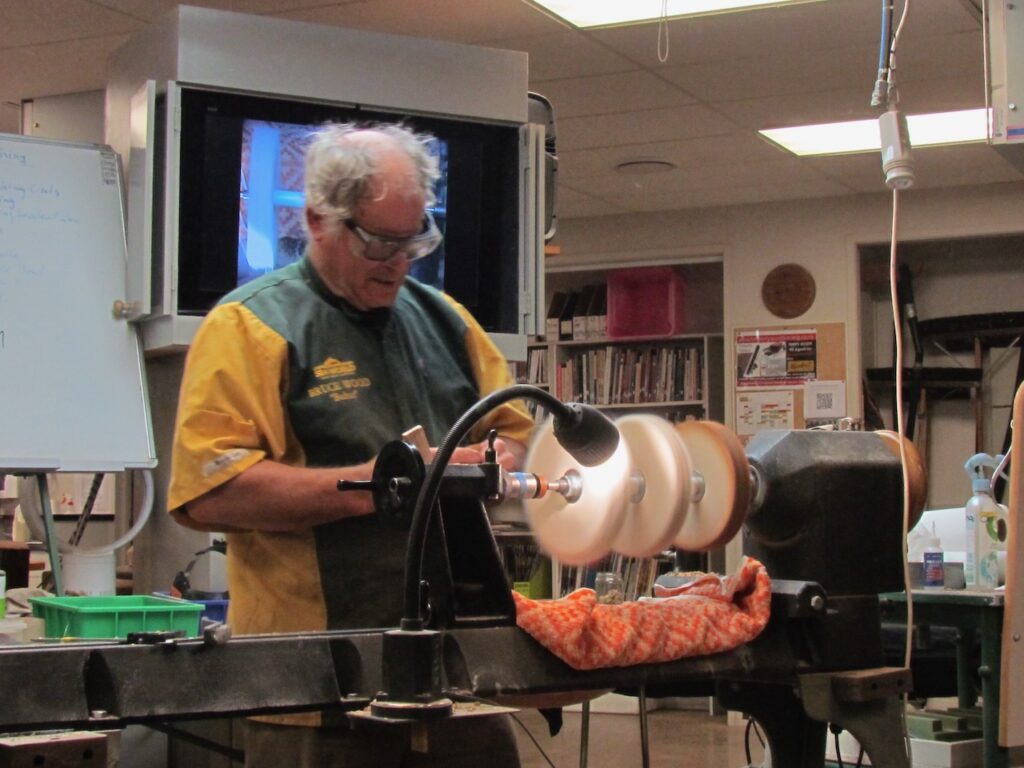
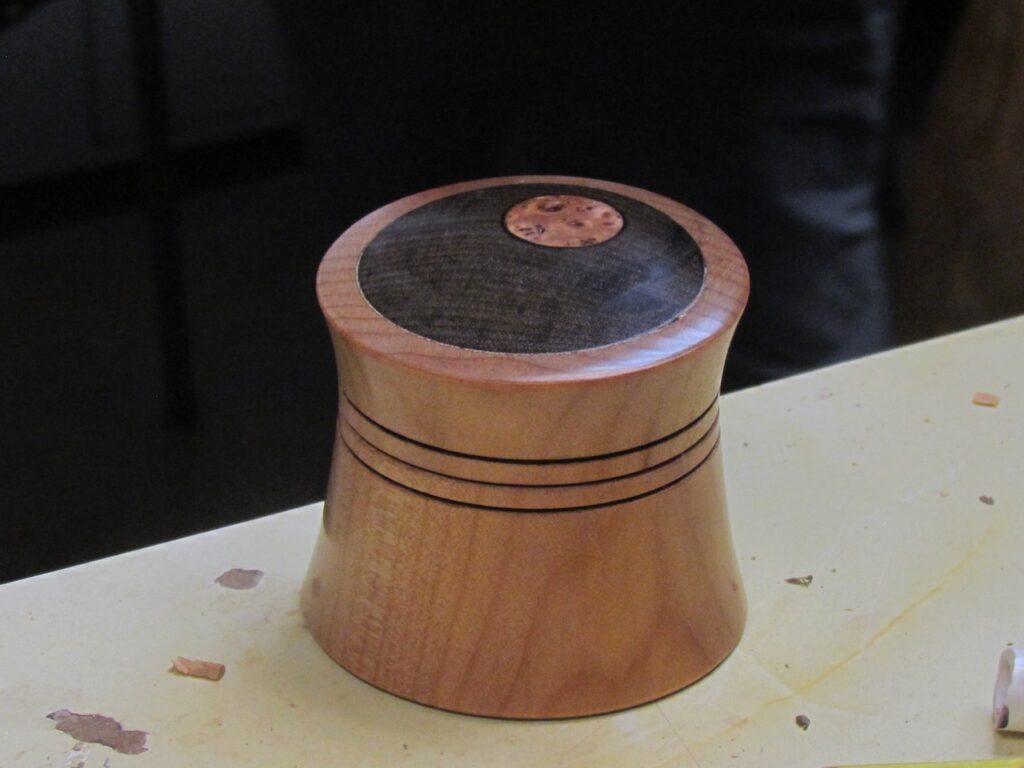
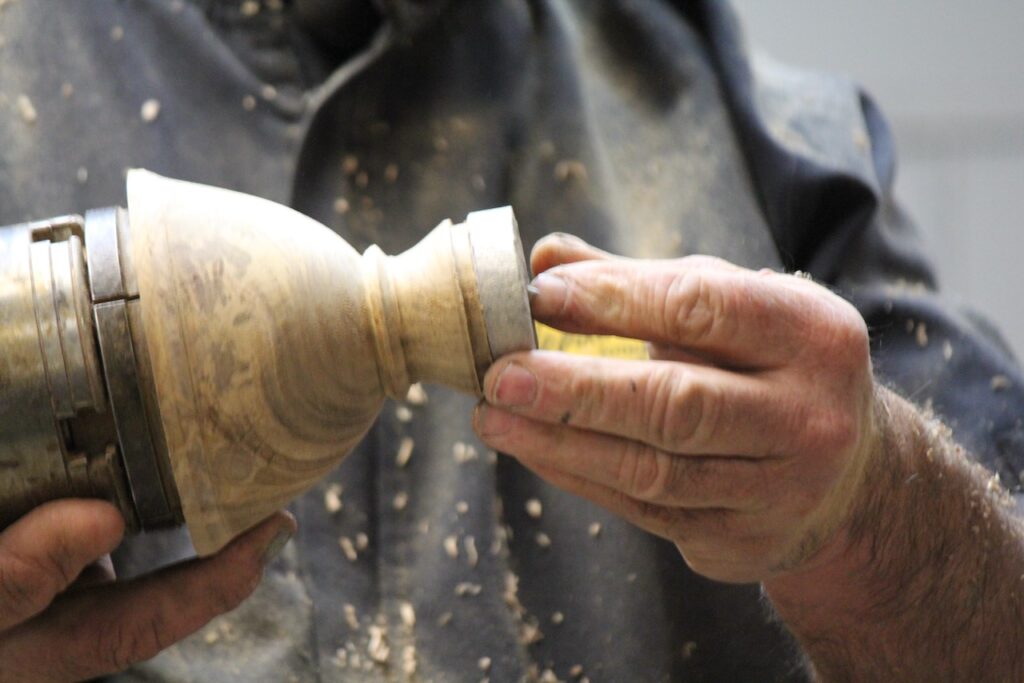
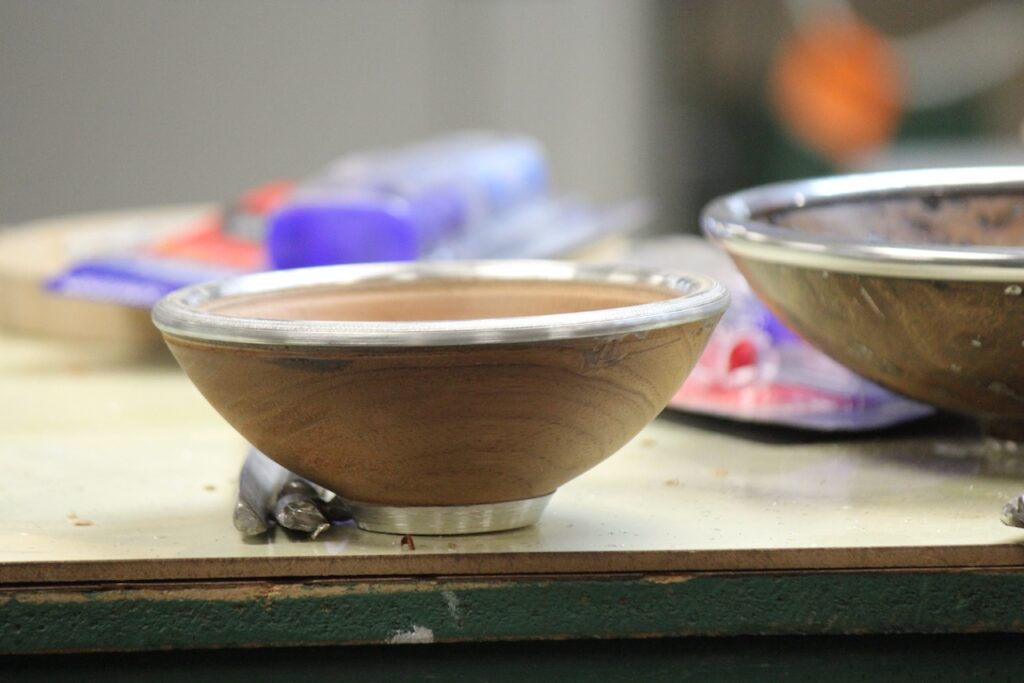
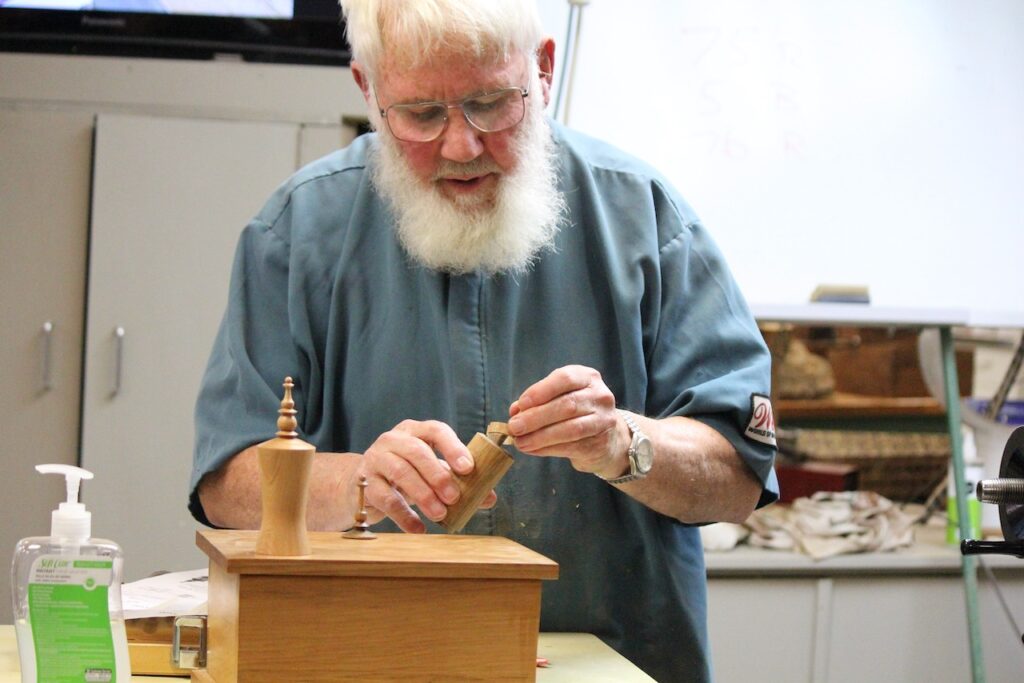
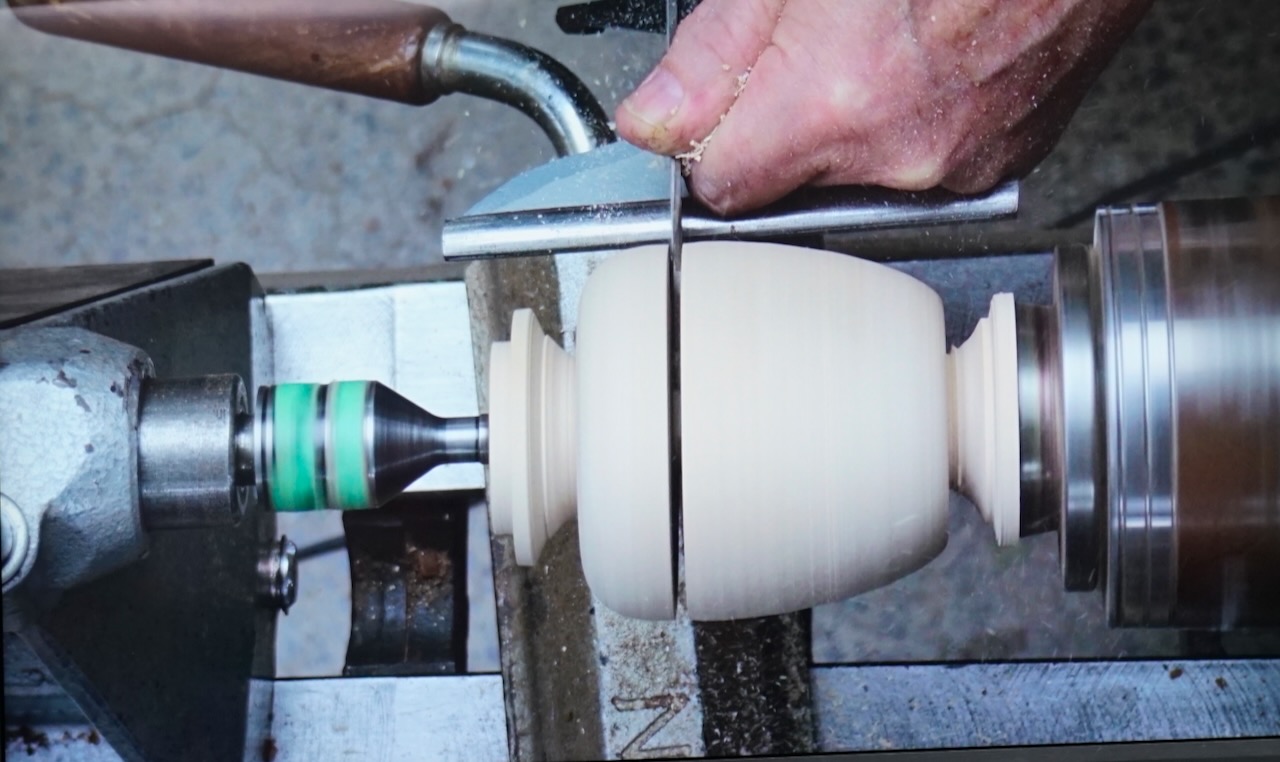
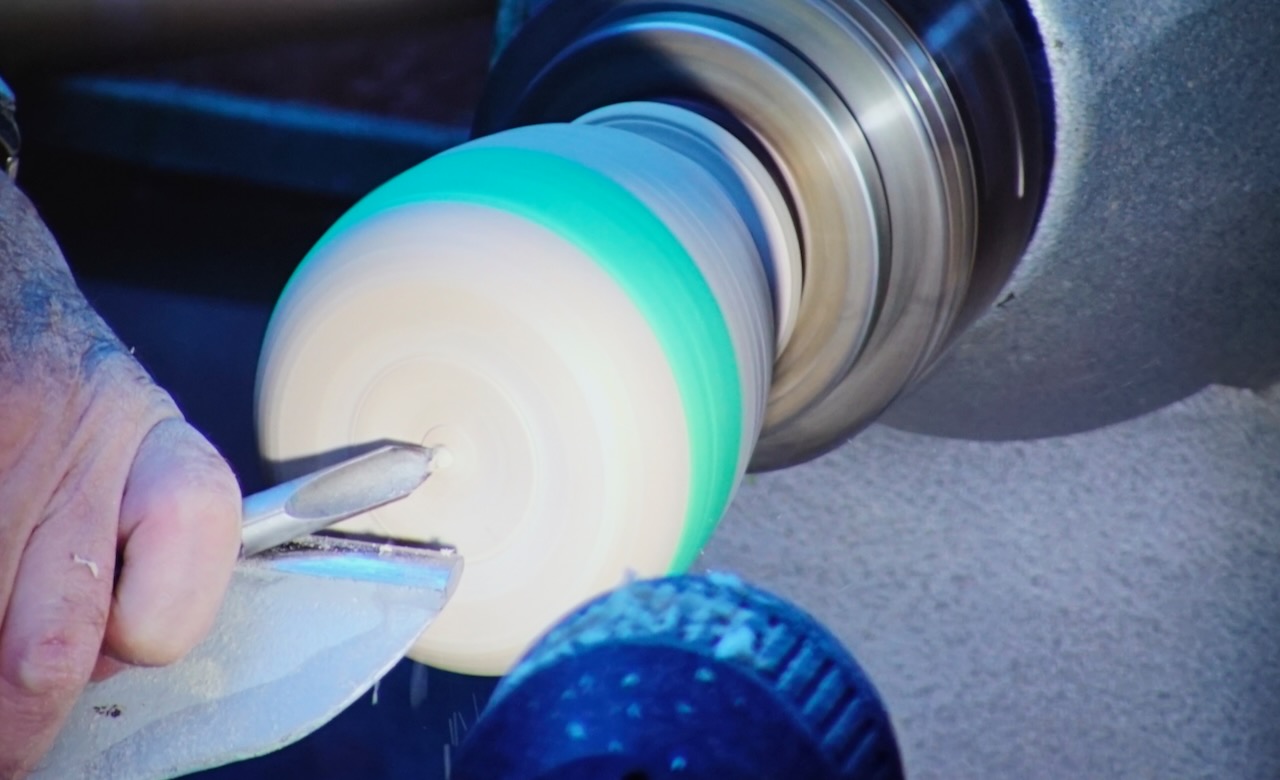
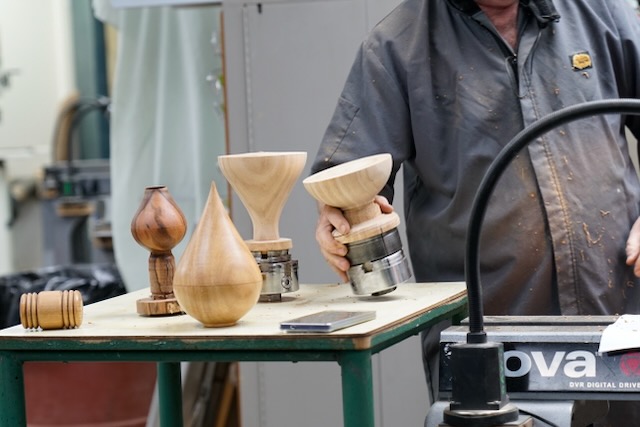
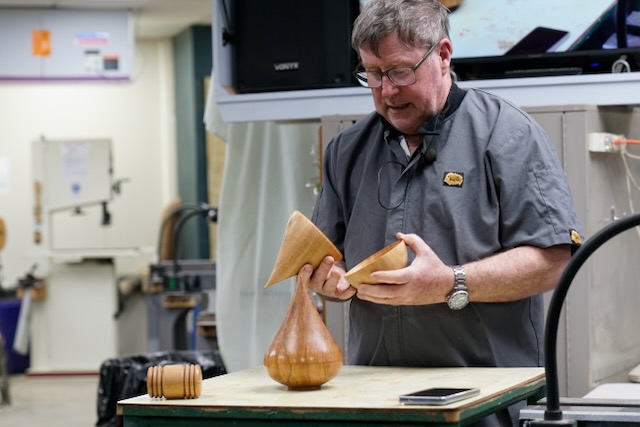
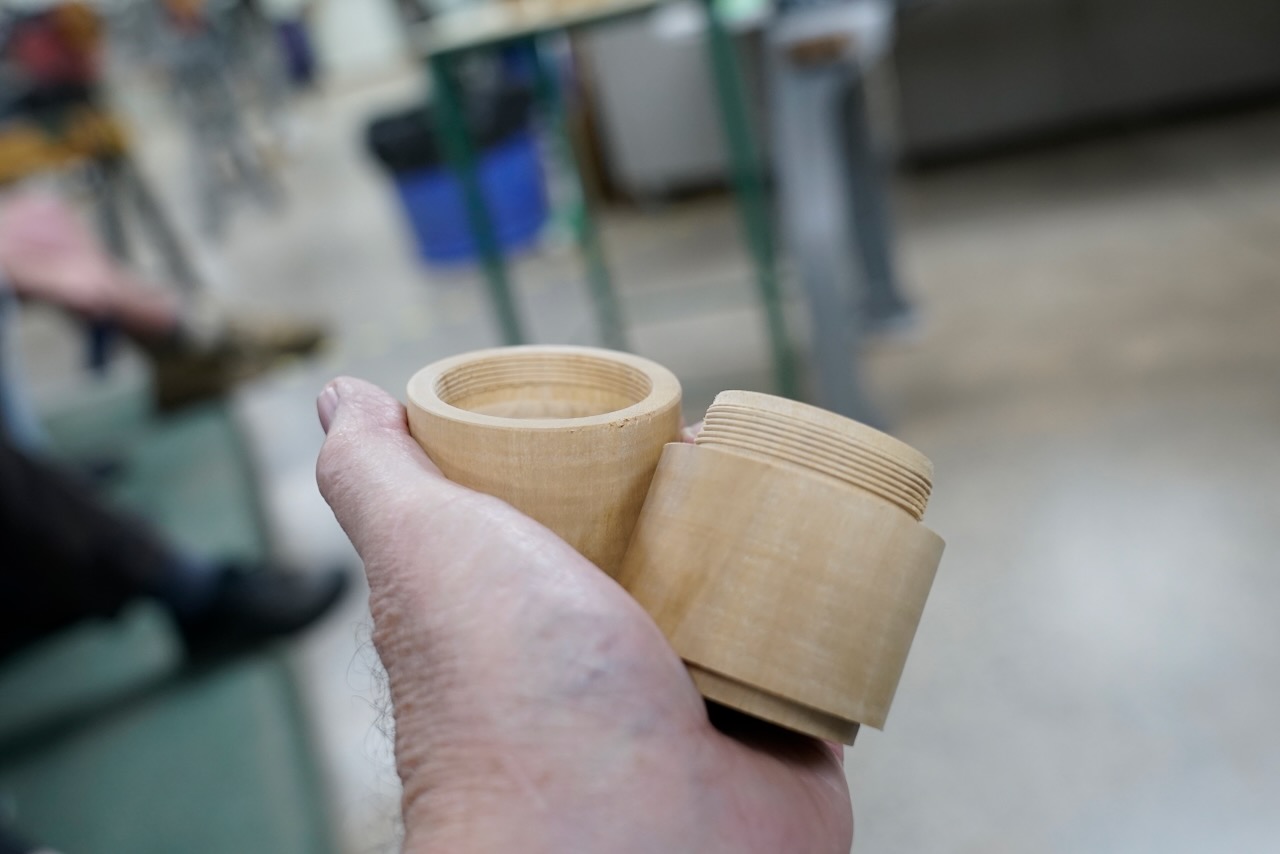
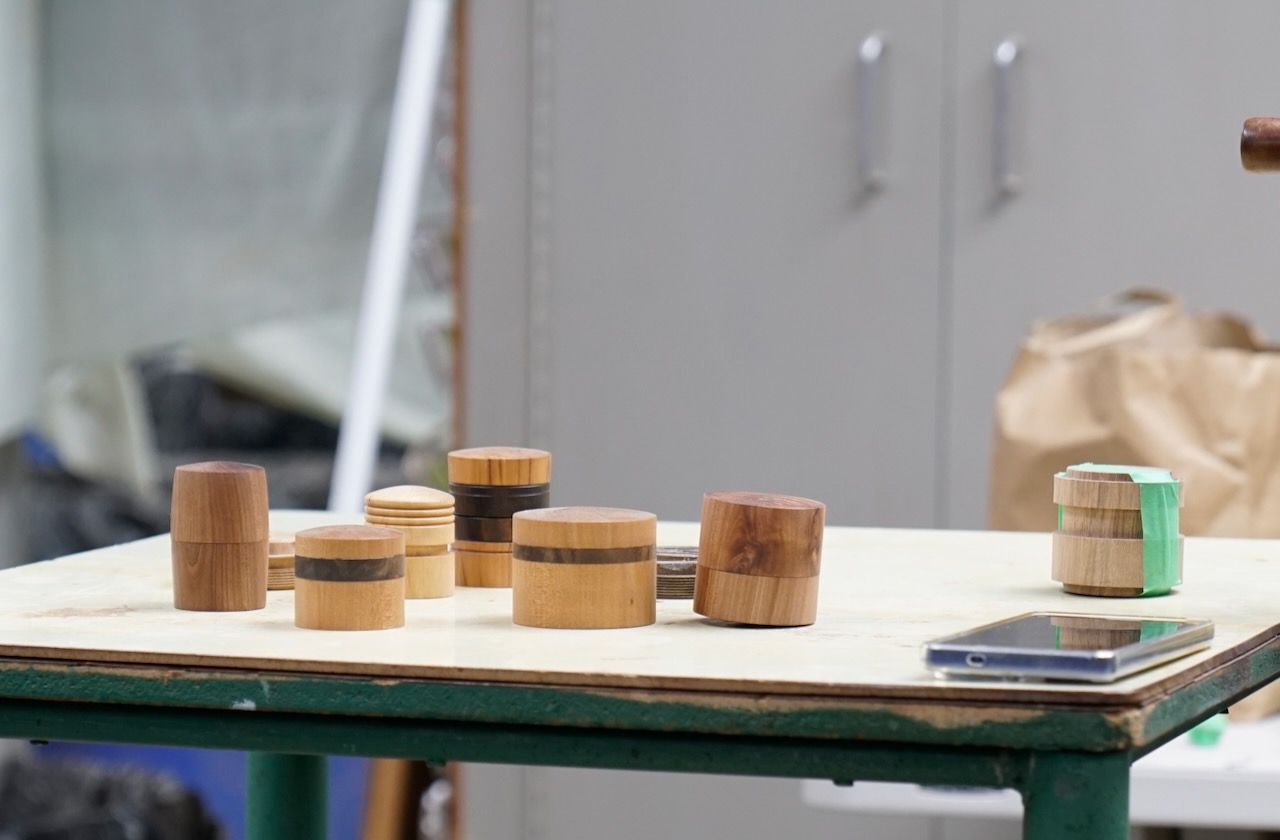
The 24th June 2020 Bruce Wood gave a great Demonstration of an Offset Box. Bruce followed the project sheet in our website of a project Guilio Marcolongo is well known for. So in this report I will not reinvent the wheel by giving you the box instructions, but leave a link to the website project instructions. https://sawg.org.nz/sawg/wp-content/uploads/2020/03/Guilios-Burl-Top-Box.pdf
But in among the demo Bruce reminded us of lots of general woodturning things to help achieve a great look.
If you are using callipers for measuring wood; round off the ends of the metal pincers slightly so the tips don’t grab the wood.
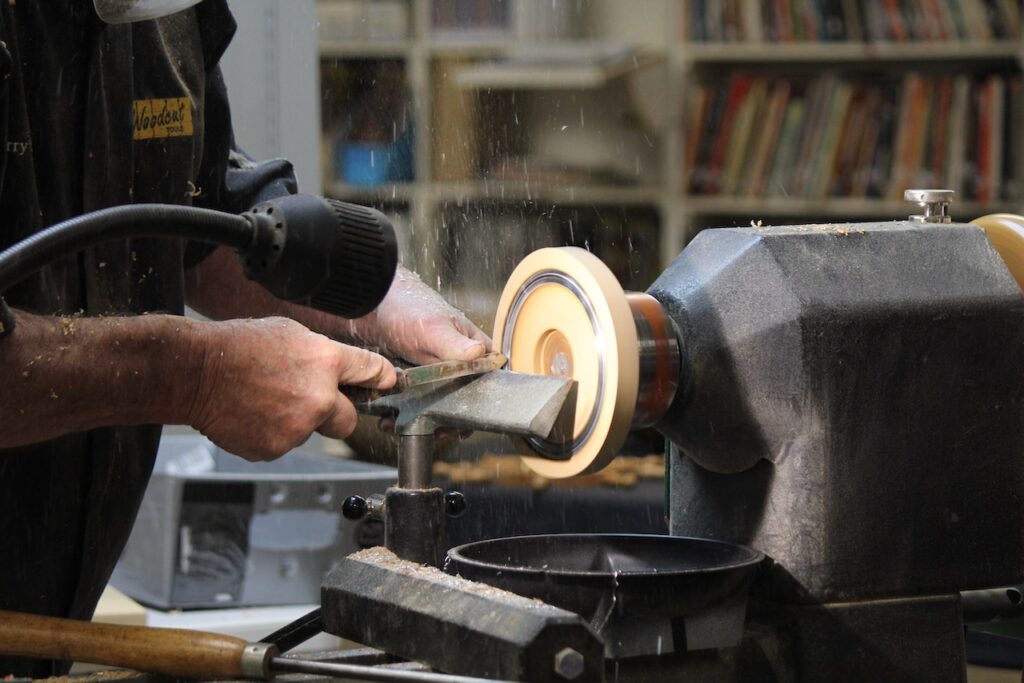
When using buffing wheels on your lathe it is easy for your turned object to fly out of your hands. So Bruce laid a folded towel over the lathe bed, so if the object flew it would not get dented on the lathe bed.
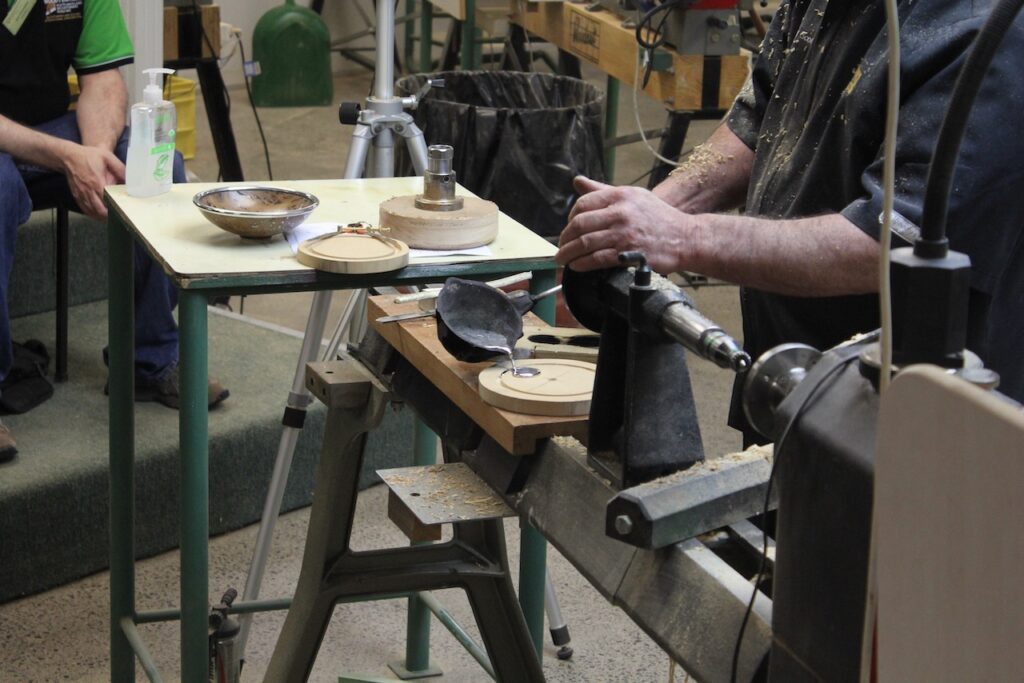
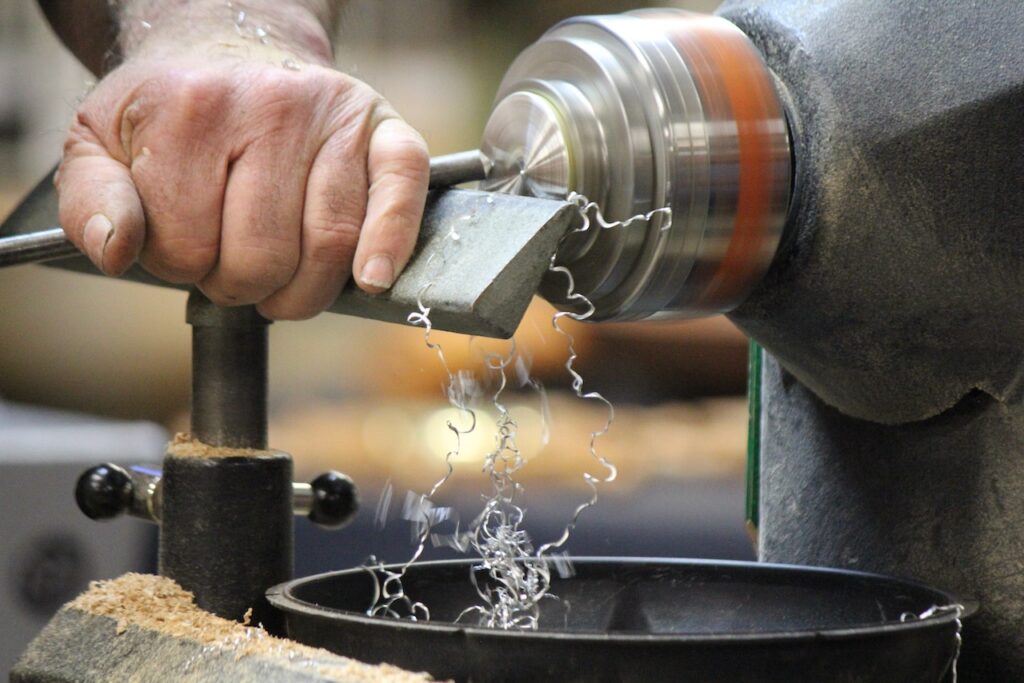
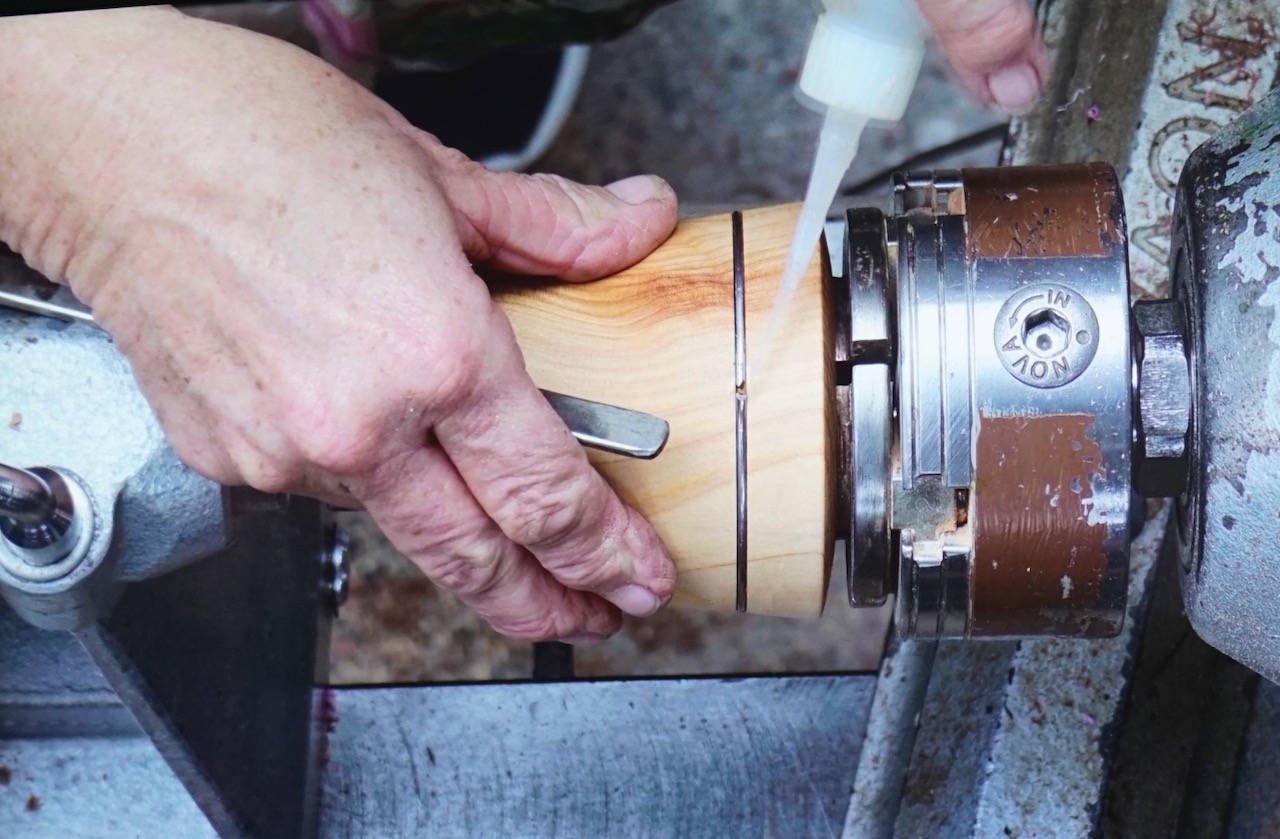
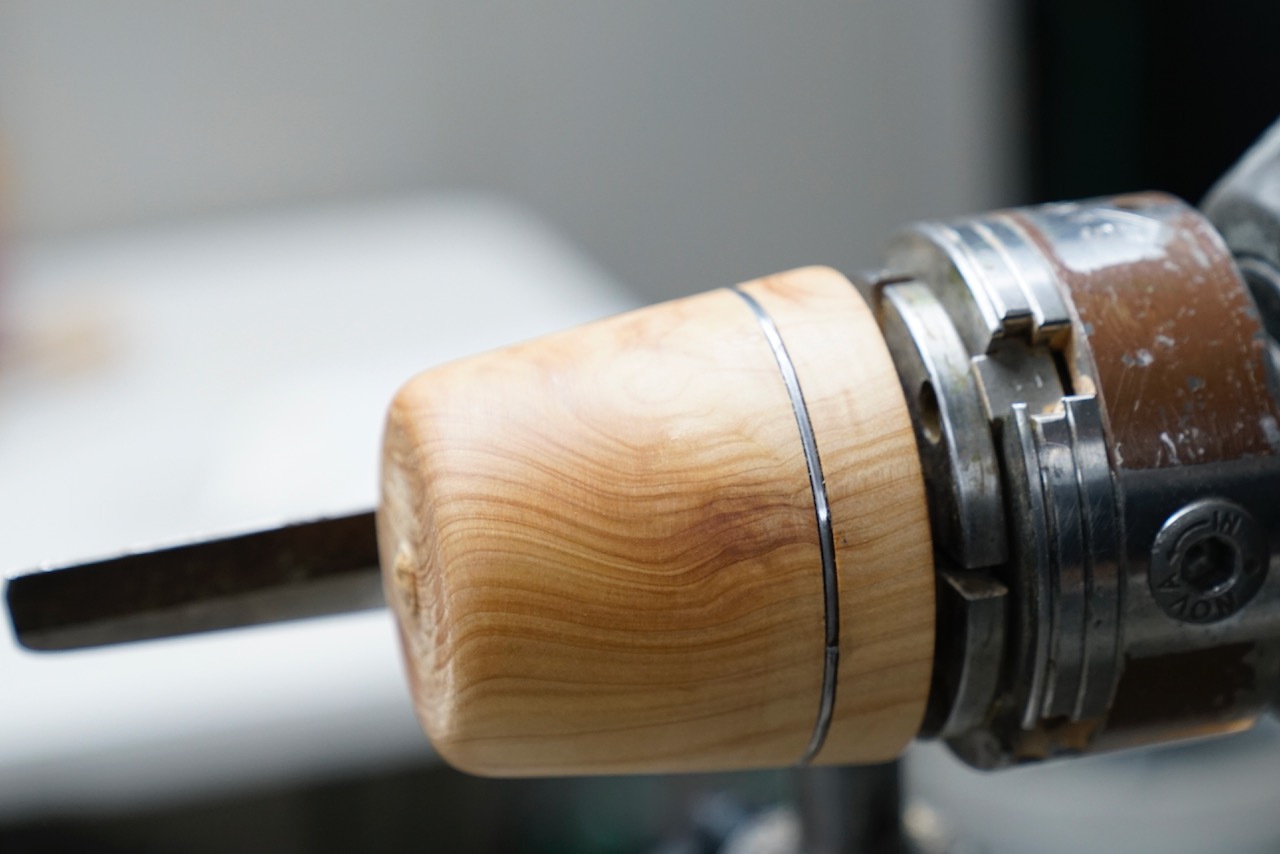
Terry had pre-poured the pewter into grooves in timber to make rods; easier to work with.
Pewter turns like butter but will scratch easily.
2nd hand pewter from op shops melted down can be ok, but old stuff will contain lead, whereas it is no longer added to new pewter.
Making the base- Use a forstner bit in plywood to make a round mold.
Pewter has a low melting point, a solder iron is no-good however.
Rim – groove with rebate; measure your outside perimeter on blank.
For molten pewter, jimmy a metal spoon onto a long stick, stir to remove slag. If left in will make the pewter brittle from air voids. It will stop skimming off slag when it’s ready.
Pour into base mold and rim, Keep continuous even pouring till it crests.
Running it under cold water will weaken it so allow it to cool naturally.
When melting do not let it boil. It will burn the timber and will react with resin in the wood when poured directly into your bowl. Sparks and flames ensue.
Diluted pewter containing lead will also make flames.
To release from mold, sometimes sawing of the wood will be needed.
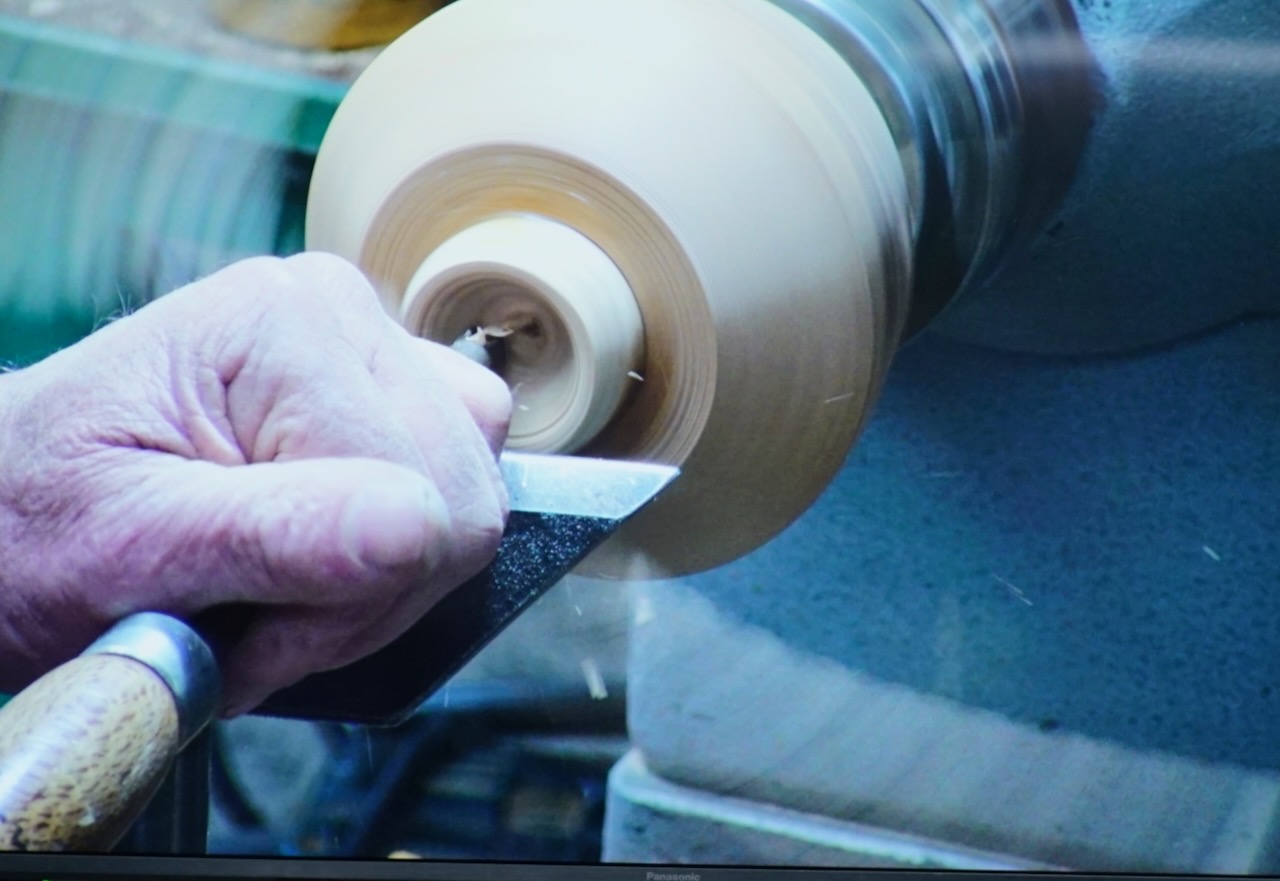
Terry demonstrates turning a bowl, cutting spigot (54mm), proceeds to make the mess he promised not to (10/10).
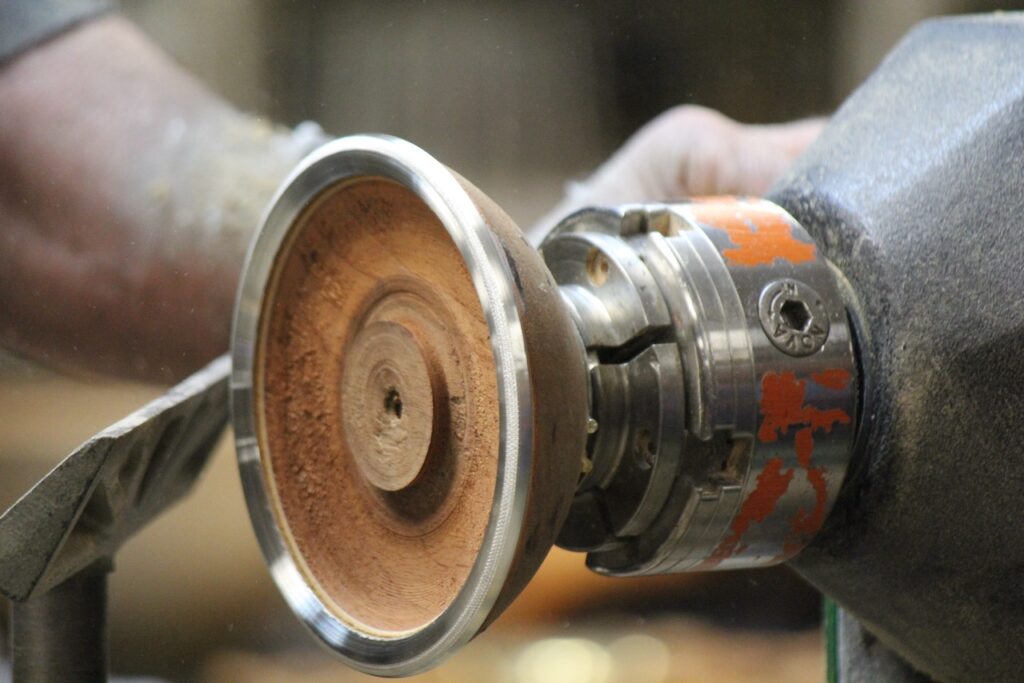
For base, cut rebate for pewter to key onto, 3mm, not too deep so you don’t lose the bottom from the inside.
Remove from chuck.
‘New turners can’t imagine a concave curve’, isn’t that always the way.
Plywood backer behind the pewter base disc in the chuck.
Levels pewter, knocks over his shavings bowl.
Cut corresponding rebate in pewter.
Turning the tenon, flat or slightly concave is ok.
Turning the rim, add spigot. Chattering that can be heard is the pewter moving in the mold, can use superglue to hold it.
Check rebate depth is the same on both sides.
Back to bowl. To avoid going back-and-forth buy a second lathe (but only from Terry of course).
Match rim to bowl with calipers.
To glue use 24hr araldite , quicker setting (5 min) is ok to get turning sooner but not as strong.
Use tape on the chuck to avoid gluing the jaws shut (Terry has extras of course).
Turn away wood on top to reveal Pewter rim, round and tidy.
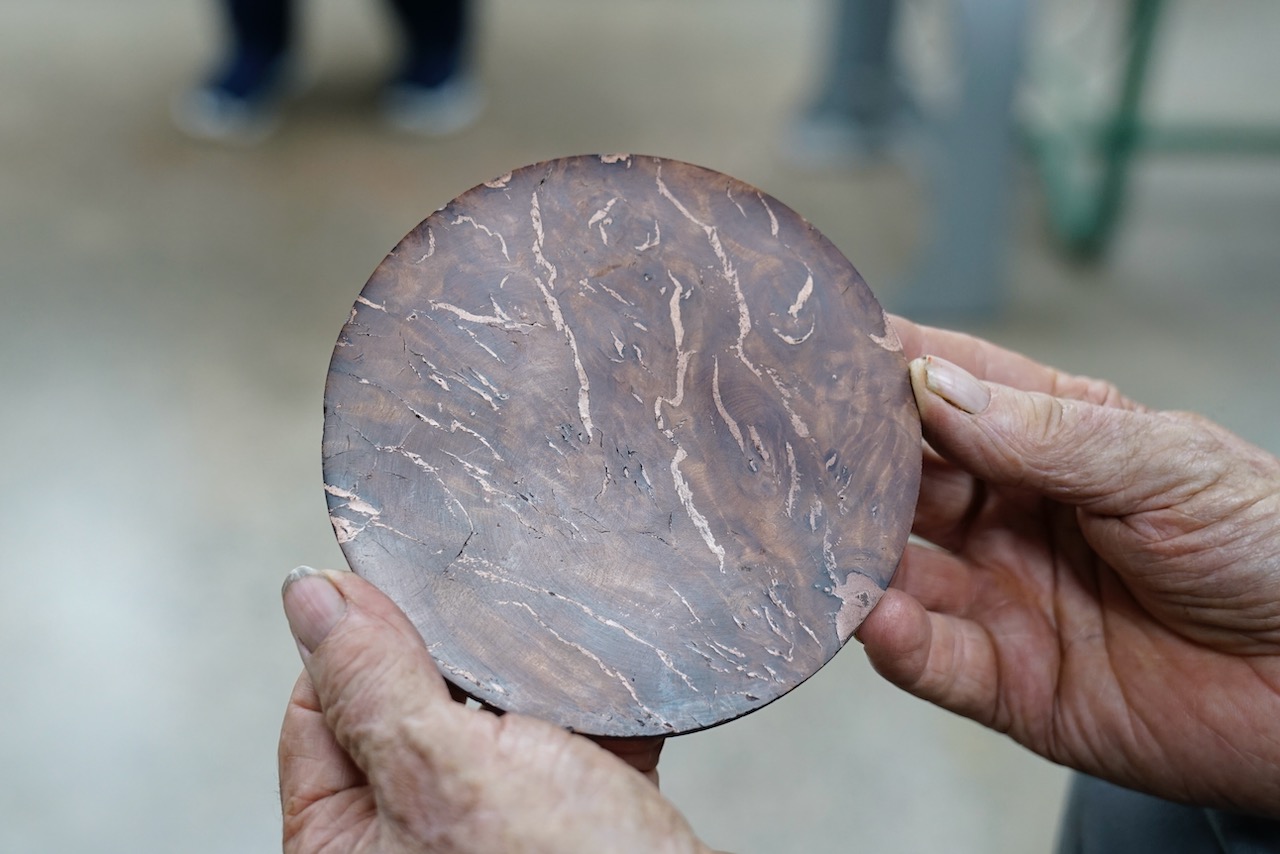
Pewter embellishes nicely, a leather punch will work and can accent with Indian ink in the grooves.
Terry uses a texturing tool.
For sanding, 400 through to 2000.
Don’t use Danish oil- black comes off pewter into the wood.
Turning inside of bowl, finish rim first because the heat from the glue can move it.
Sand inside w/ 240 grit, through to 400.
Use jam chuck to reverse bowl, Terry uses next bowl to hold it however, turn RPM down.
Cleaning the base pewter, pronounce concave of the base to remove weight.
Tidy and sanding exterior of the bowl.
Warned to use mask with mahogany as the dust is sharp and dangerous to inhale.
The base foot pewter can scratch easy but won’t need polishing like silver.
Club Meeting Demo : 3rd June 2020 Report by Graeme Mackay
An excellent demonstration highlighting the need to work through process and sticking to measurements, measuring again and checking that measurement. Dick Veitch followed the Project Sheet for this small functional item, with several components.
As usual Dick came up with some simple solutions, some quick marking answers and developed a fun project. A good chance for new turners to think through process, work out the operation off the plan and apply the required actions. A good example was the use of the Bryden centre finding tool.
The side title to this project could actually be the drilling project and/or Jacobs chuck use. The Turner is required to use the Vernier callipers and check the diameter of the Forstner and/or Brad point drill bits. This included the simple straightforward sharpening of the Forstner cutting blade. The age-old question of checking out your tools before use was quite apparent. It may be a 16 mm Forstner bit, however, when check the diameter was 15.85 mm. A small discrepancy that could totally fail up the pop-up movement.
Dick demonstrated that keeping to the sequence was key to this little project. Possibly one should say sequence and correct depth. Marking the depth on the drill bits was a good value-added action. Simple, straightforward and easy to do with a bit of tape. There was a timely reminder that dual speed is important. Check the charts. Ensure that the shavings are coming off an even basis. The correct speed means cutting rather than skidding.
Although a functional item, once the components were completed, there was plenty of design space for getting the best looking form. Choosing the appropriate type of wood will help get clean fine-grained services that allow the pop-up mechanism to work.
A good learning project. The project sheet is on the SAWG site and is easy to follow. Further, provides a good plan reading and/or process organisation exercise.
Tom showed us various boxes that he had made over the years of many sizes. Including a spinning top box which was an ancient game originating in the Middle East
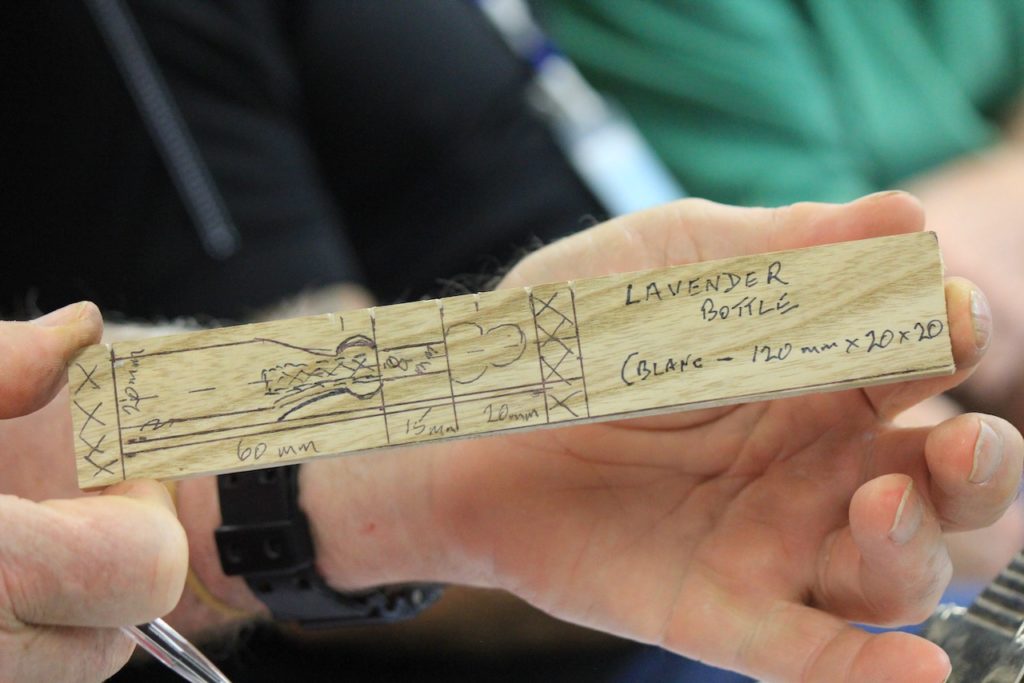
The blank used for the Lavender Bottle was 20mm X 20mm and 120mm long was placed between centres. Tom used a “story stick” with the dimensions of each element of the bottle. From the Headstock end. 60 mm for the bottle 15mm for the 8mm spigot plug and 20 mm for the knob.
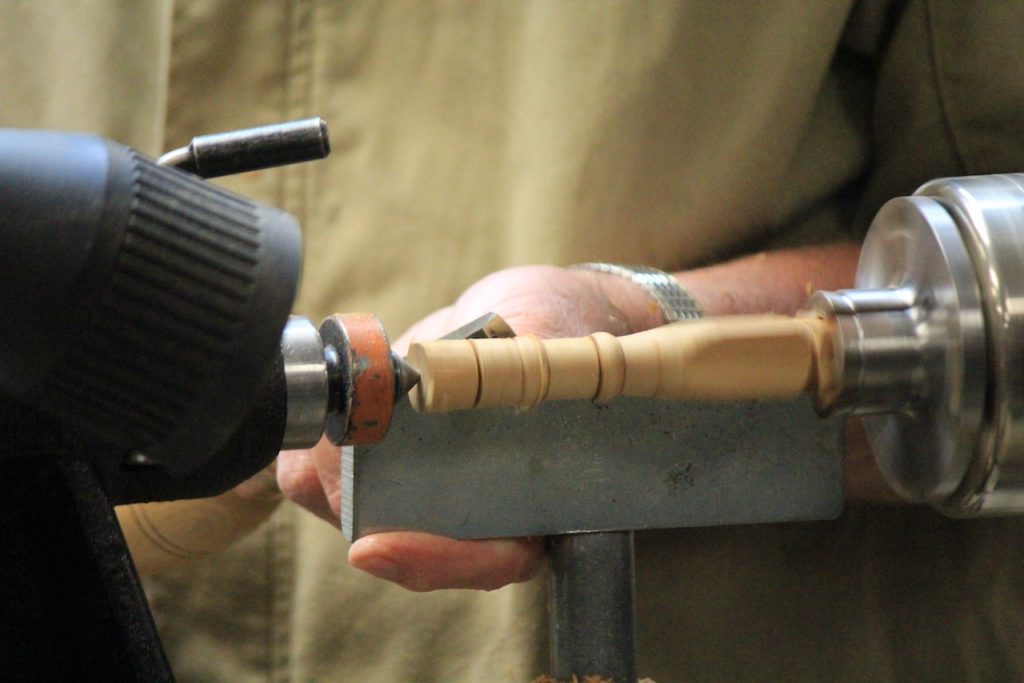
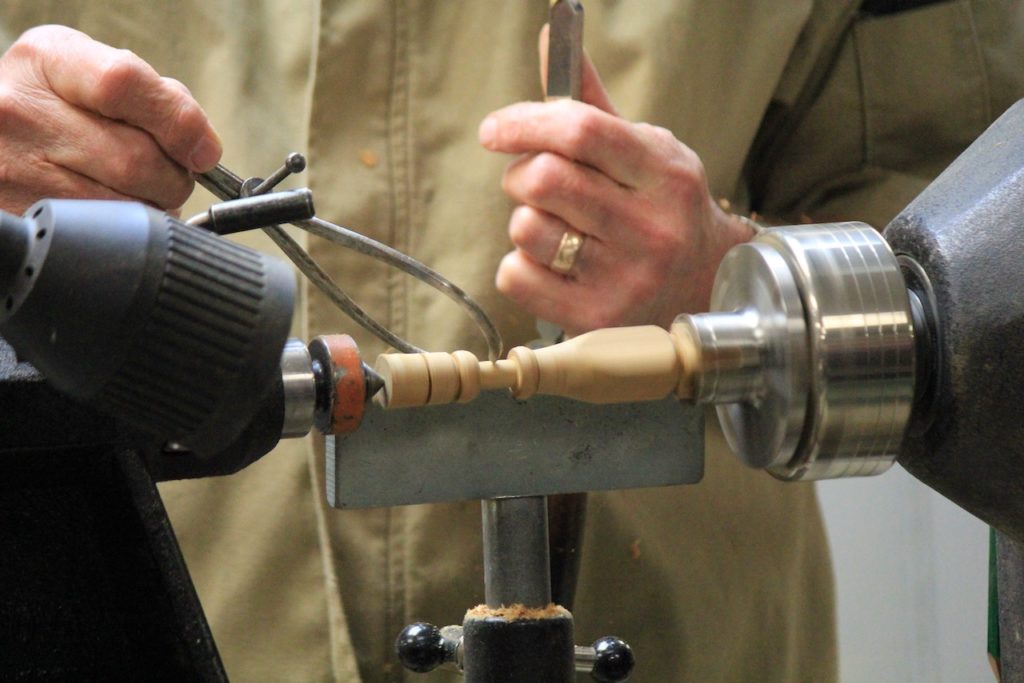
Leaving the bulk of the base square he shaped the foot and the neck of the bottle with a bulb at the top. The next 15cms were parted down to 8mm using parting tool and calipers. The lid was then shaped as per the photograph with a spindle gouge reducing the waste at the top for later removal.
At this stage the bottle should be sanded and finished.
Hold the base in in a small set of jaws and centre using the steb centre. A 2 mm parting tool is now used to cut off the spigot. With an 8mm bit drill to a depth of about 25mm and fit the lid spigot into this hole . Tom used a round file and sandpaper to achieve a snug fit. It was noted that the spigot may be shaped more narrow where it meets the hole to assist fit. The lid can now be removed from the waste and final sanding and finishing done at this point. The spigot is sanded if necessary to ease the fit.
The base is now parted off and sanded on a sanding mandrel in a Jacobs chuck on the lathe or a belt sander. Finish with oil wax or lacquer as preferred.
When ready to sell or gift pour no more than 2-3 drops of oil in the hole. This will permeate through the wood to perfume handbags, drawer or car, etc. Too much lavender oil can be overpowering.
Club Meeting: 11th March 2020 Report by: Bob Yandell
The “House Full” sign was up and Terry was at his best – humour, skill and knowledge for all present. The start was, as only Terry, the entrepreneur and entertainer could, an opportunity following the Covid-19 outbreak and subsequent shortage of toilet paper. We woodturners could meet the shortfall by providing toilet paper by supplying the leaf from Salanum maurtianum plant, better known as Woolly Nightshade or Tobacco plant which Terry observed was growing in plentiful numbers either by itself or in combination with our turnings and a few chemicals mixed together, compressed then peeled like a veneer and rolled. If you weren’t there you missed the business opportunity of 2020.
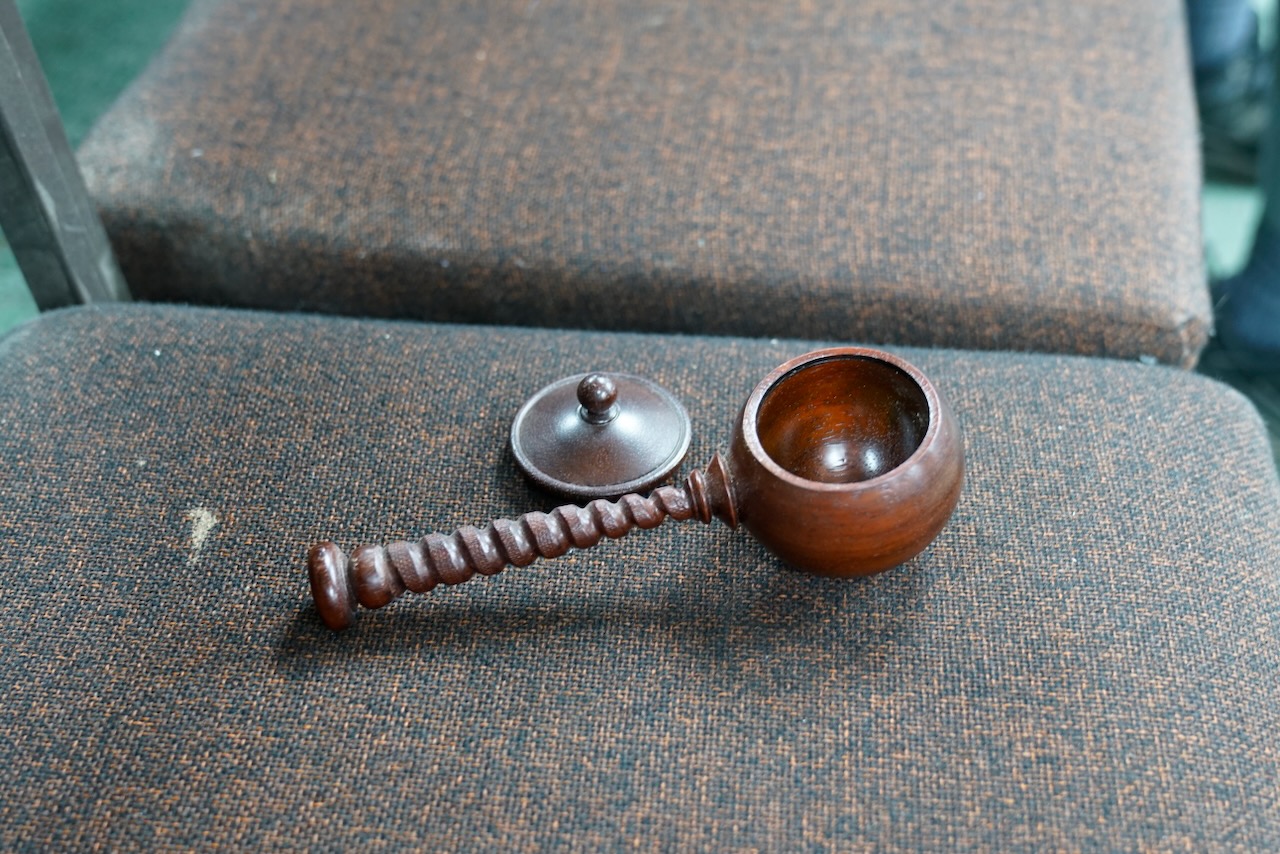
The actual demonstration began with Terry showing examples of spoons and his development of the concept into the lidded box. Spoons for a salt pig through spoons with long handles. (Refer Club projects sheets – Spoons for the basic concept).
Terry started with a block of Kauri 60x60x180mm. Hard woods are best used when making spoons. The block was mounted between centres and turned round. The final diameter was 53mm based on the internal dimensions of the sphere cutter being used and a 48mm spigot was put on each end. The lid section was parted off at 64mm. The box/spoon section was that left. At this point Terry informed that the length of the spoon was dictated by the swing over the lathe and a maximum length for the lathe was 400mm to which the allowance for the lid and spigots “X”mm is to be added.
The Spoon/Box portion was mounted in the 50mm chuck; end cleaned up and a line defining the centre of the sphere clearly drawn, approximately 28mm in from the end, and a fainter line defining the sphere diameter marked. This latter line is where the handle starts and a cut on the lathe head side of the line, with the parting tool indicates the beginning of the handle profile and diameter. The distance between the line defining the centre of the sphere and the external diameter is divided into 4 equal parts(3 lines either side of the main line) because a sphere is formed from 4 flats( starting with the centre line being the beginning of the curve and end furthest from centre being the end of the curve and the beginning of the next and repeating until curve complete).
The sphere profile is refined gently using a pipe tool with the lathe running. This is a piece of tube with a handle fitted in one end that allows approximately half the diameter to extent, like a chisel tip, and is sharpened on the belt sander. The “roundness” is checked using bottle caps and until no gaps between wood and cap. Sand and finish.
Complete the handle profile and part off. Texture, captive ring, may be pyrography – sand and finish.
The next stages require a jamb chuck and ideally a second chuck for the yet to be made lid.
Making the box requires a jamb chuck mounted in 50mm chuck. The sphere plus handle needs to fit snuggly so handle is flush with face of the jamb chuck. Determine diameter with callipers or Vernier and mark face of jamb chuck and turn out always checking fit. It must be snug and firm. Cut a slot to accommodate handle. Terry used an Arbortec. Drill a hole from the side of the jamb chuck into the bottom to assist removal. Position the sphere in the jamb chuck to optimise the strength of the grain and visual appearance. Hot melt glue can be used to ensure no movement of the sphere. Mark the centre so a drill can be used to define the depth of the cavity of the box. The depth is the diameter id the sphere less wall thickness.
Cut the opening for the lid and hollow it and cut the rim to accept the top part. Finish all these surfaces. Terry used a cup tool and emphasised the need to rub the bevel. He also used a scrapper in a circular motion, like the hand on a clock to maintain the inside of the sphere.
Next stage was the lid using the piece set aside at the beginning. The face is cleaned up and the internal hollowed so that the curve is a continuation of the internal curve of the box. There is sufficient wood so Terry was able to develop the external profile so it matched/complimented the box. This is where a second chuck is of value as you can produce the lid and then fit it to the box to finish the top albeit a finial, knob or handle. Complete the handle profile and part off. Texture, captive ring, may be pyrography – sand and finish.
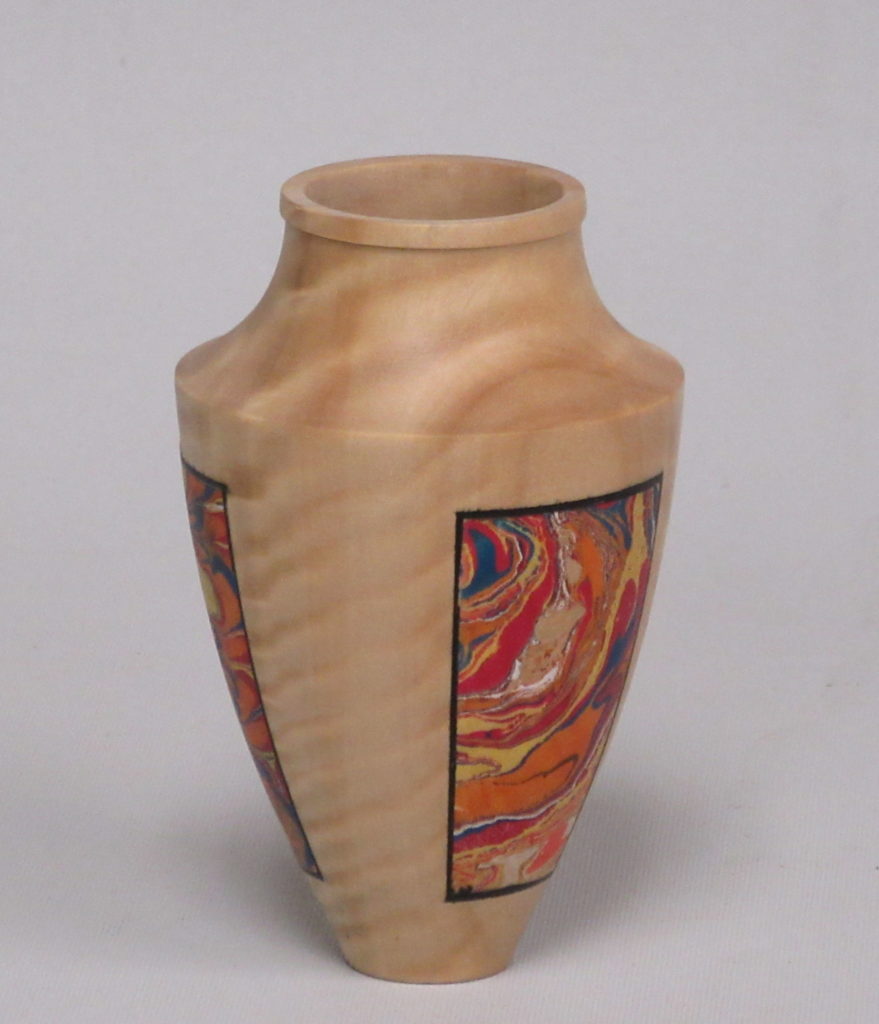
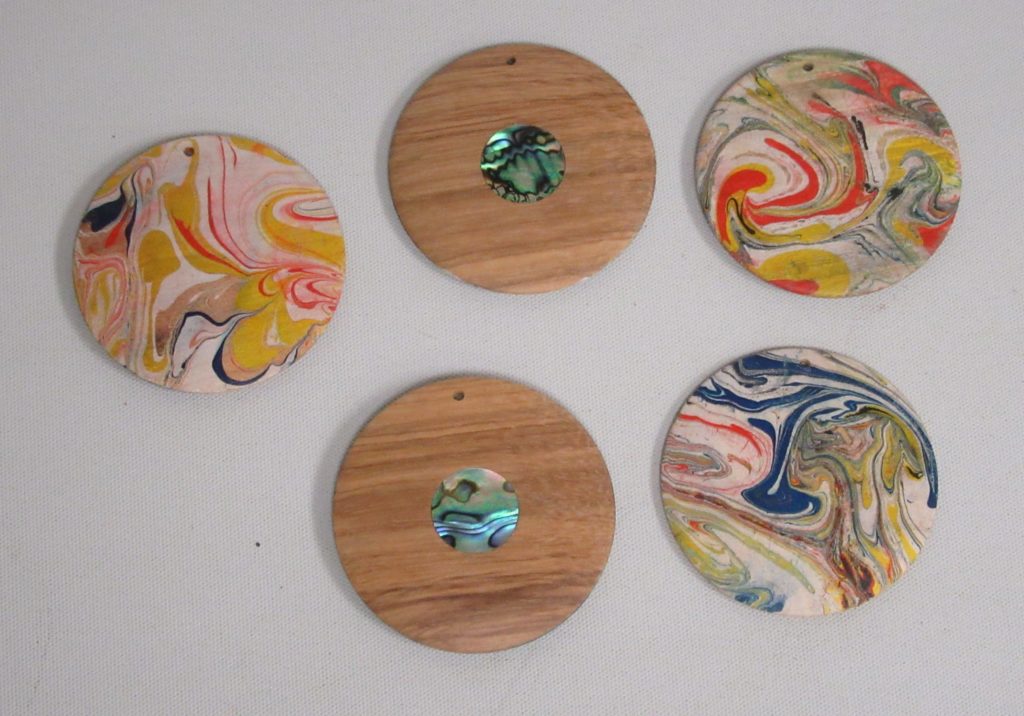
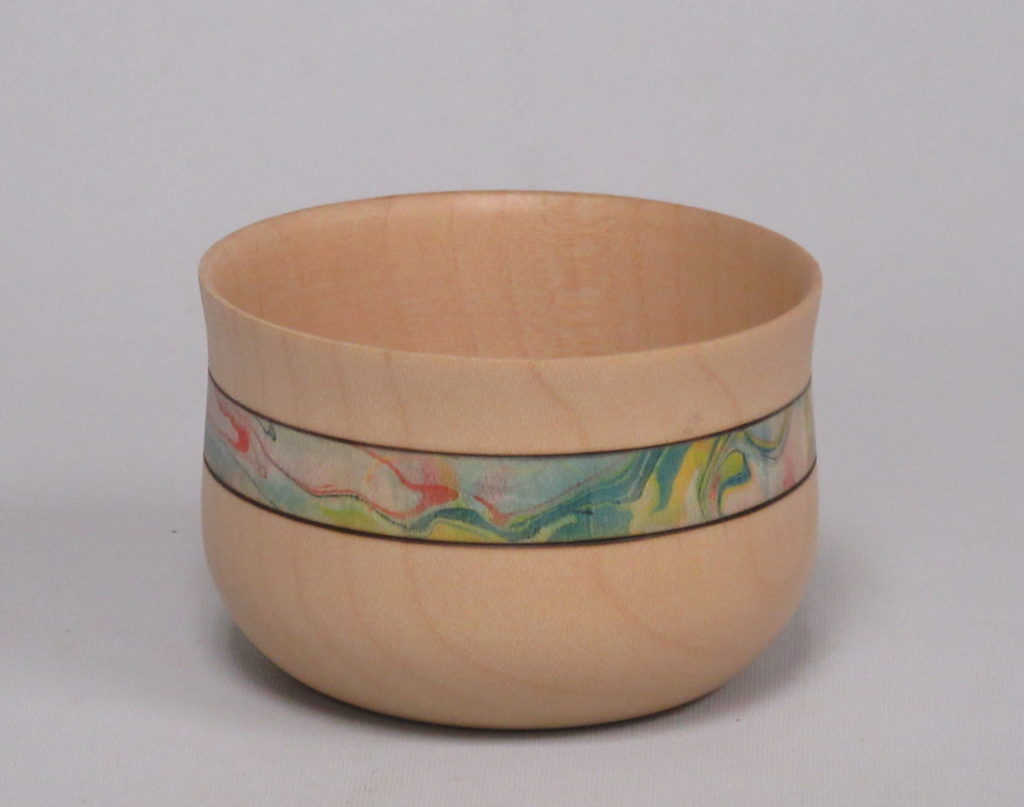
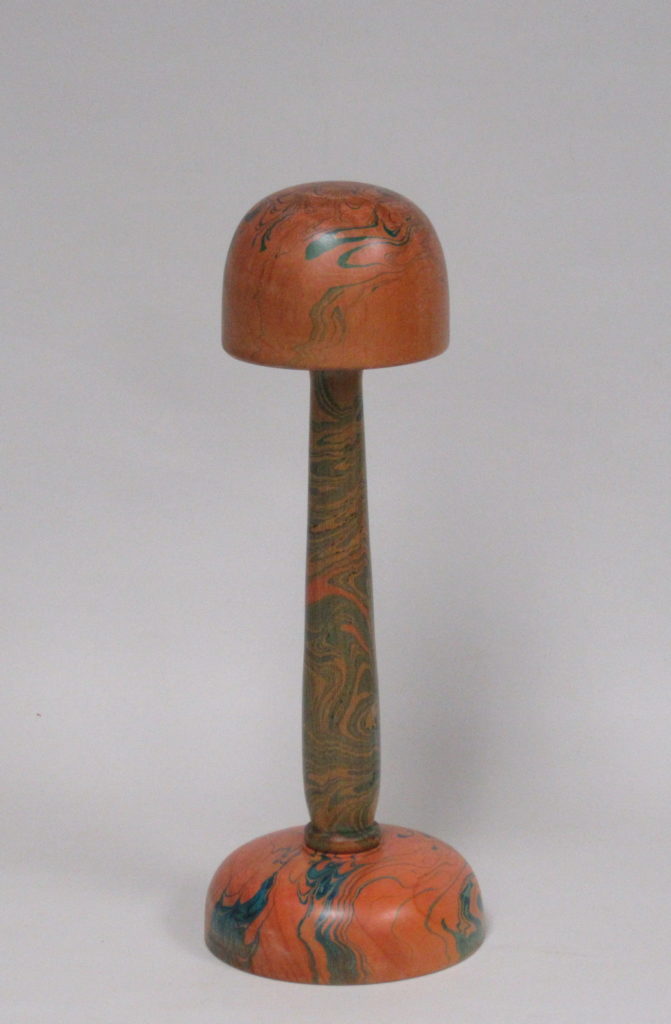
Despite marbling being a craft practised since the 12th century we still don’t have a precise recipe on how to do it. It has, however, been part of the NAW National Certificate in Woodturning since its inception. In the training books we find a recipe that works – but, it seems, not well enough for many to use marbling as a frequent enhancement of their woodturning.
When Walter Wager, from near Tallahassee, offered us a marbling demo I was a bit ho-hum. He included a copy of his marbling report to the American Woodturner journal. Nice pictures, nice work, and yet another recipe requiring the mixing of spoonsful of this with quarts of that to make up gallons – probably US gallons. There also was a statement about “pure” this and using distilled water. A little web search established that I could buy distilled water in the supermarket and I could order in pure methylcellulose and pure alum.
That suggestion of not using our chemical-laden town water and not using wallpaper paste (methylcellulose with unknown additives) made great sense. Please do visit us, Walter.
To prepare for his visit I worked my way through many recipes to make up an alum solution and the methylcellulose size needed to float the acrylic paint needed to create the marbled effects. Now, bear in mind that there are marbling kits available in some New Zealand stores and online – they all work, but most are designed for one-person use. We were going to have ten, or more, people wanting to put marbling on their choice of wood. The National Certificate in Woodturning also needs to cater for more than the single user. So, getting information on the important ingredients is necessary.
The important wood preparation is firstly to choose a dense white wood, turn it, sand it, and apply alum to the wood – just keep the items small please? That meant that most arrived with eggs, egg cups, a wig stand foot and little bowls but, as always, one had to arrive with an item that challenged our biggest dipping dish!
Any acrylic art paint is supposed to work – true, most do – but, as a rule, the cheaper the paint the coarser the granules within the paint.
Next challenge is to get a nice pattern of paint floating on the surface of the methylcellulose size mixture. Amongst the crowd at Walter’s hands-on afternoon we had some fairly basic acrylics, tubes of quality colours and some of the Golden High Flow Acrylic mentioned above. Most of those had to be thinned with water (or, later, more paint added) so that the paint would float on the surface of the size. Some spread more readily than others. Some colours of the same brand spread well when used alone but then either would not spread when placed over other colours or would spread madly and push everything aside.
Our choice now is Golden High Flow Acrylic. Ok, appears to not be cheap but only a few drops are needed for each marbling action. This paint has a fine and consistent texture and is available in more than 50 colours.
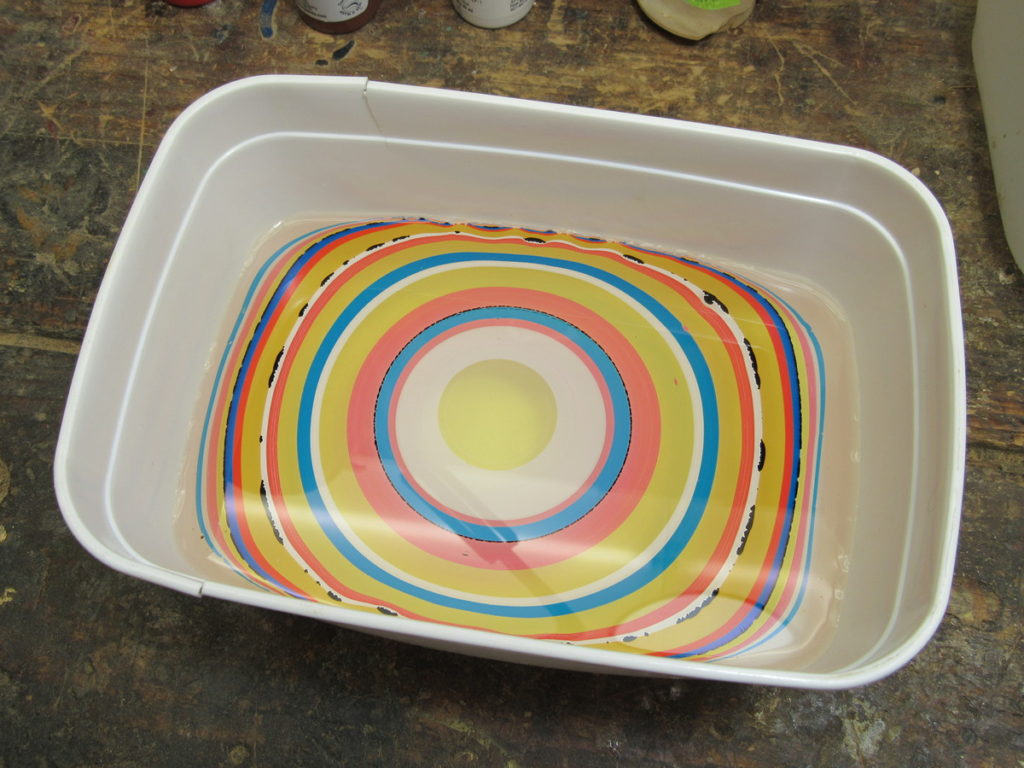
Obviously, putting drops of colour sequentially at the centre of a bowl results in rings of colour. You can have these rings of colour on your wood or take a comb and stir it a little. Then dip the wood in. Rinse it off and let it dry. When thoroughly dry put a finish over it.
Club Meeting: 4th March 2020 Report by: Cathy Langley
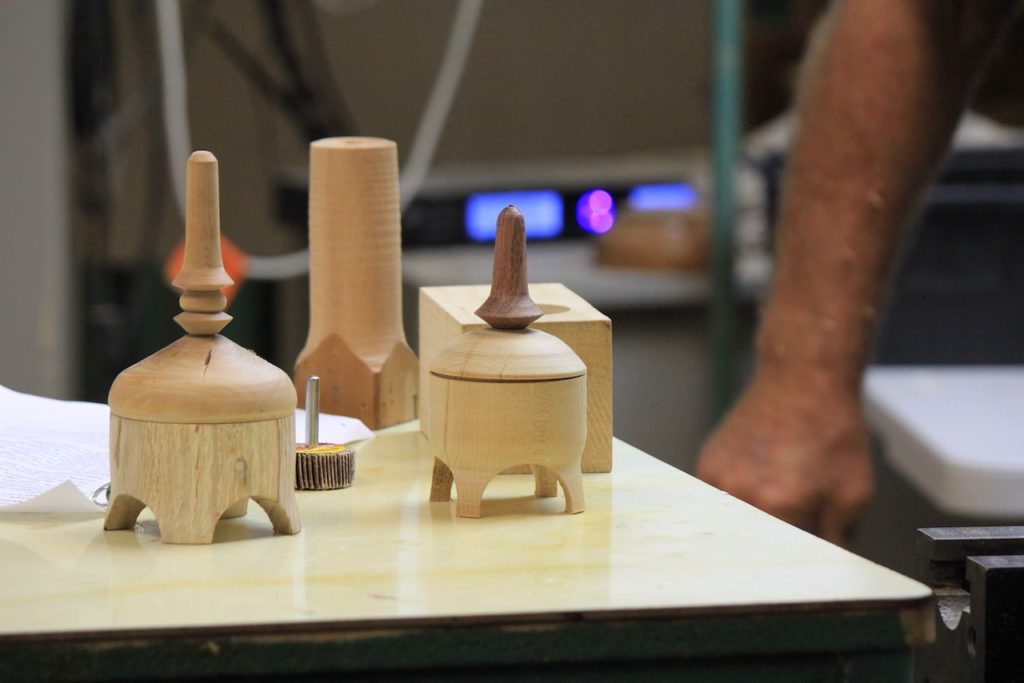
Garry Jones’ version of this term’s “lidded box” theme was a small jewellery box for storing women’s rings (both under and above the lid) with four feet and a finial providing elegance. Garry had brought a number of finished examples illustrating a range of possible designs.
He started with a block of timber 70 x 70 x 150 cm, emphasising that the blank needs to be exactly rectangular so that the feet are equally spaced. On each side of the blank, he had drawn a line 40 cm from one end for the lid, and had marked the centre point of the longer end on each of the four sides. At these points, he had drilled a 40mm hole into each side, meeting in the centre and creating what would eventually become the space between the four feet.
Using a steb centre in the chuck, he created a spigot on each end, remounted the blank with the holes at the headstock end. He marked a line just beyond the holes on the side toward the lid section, to indicate where the bowl shaping would begin. He then turned the lid section to a cylinder and shaped the bowl and feet, with a narrower diameter where the line had been drawn earlier to indicate the base of the bowl.
The next step was to part off the lid section and hollow out the interior of the box. Garry used a Rolly Munro mini-hollower to leave a raised “finger” in the base of the bowl to hold the rings. Garry then faced off and designed the rim of the bowl as for any other lidded box. He left the sanding and finishing to our imaginations (except to suggest that the edges of the holes be smoothed with a flapper wheel in a drill) and parted off the blank, separating it from the spigot at a point that cut into the bottom edge of the pre-drilled holes to separate the four feet.
The next-to-last step was to mount the lid section in the chuck, face it off, and hollow it. (Garry suggested that a dimple could be left in the inside of the lid with texturing applied around it, as he had done in several of the examples of finished ring boxes that were passed around.) He presented the base of the box to the mounted lid several times to ensure a good (and fairly loose) fit, and then completed the outside of the lid, leaving a spigot at the headstock end which could either be turned as the handle for lifting the lid, or as a 10mm (or just under) dowel over which a finial could be glued into place.
The final step is optional. Several of Garry’s examples had a finial on the box 50-80 mm long with an approximately 25mm base, narrowing to 12-15mm at the top, to hold additional rings. If you decide to do this, mount a 40 x 100 mm blank of similar or contrasting wood, drill a hole 10mm in diameter and about 10 mm deep, bring up a live centre in the tailstock, and shape he finial. Finish and part it off, and glue it over the dowel at the top of the lid.
Dick’s pencil boxes demonstration: This exercise was taken from an AAW project that was based on Beth Ireland’s boxes. The process is that the box making system ends up with a pencil looking like a pencil case. Dick started the demo with a history of lead pencils i.e. those with graphite in them in. Then a discourse about the colours that pencils came in.
The base: A cylinder, about 200 mm long is made with two jam chucks it is cleaned and then a parting is taken around 60 mm from one end.
A Dick V tip: When parting off a piece, remember to keep the gap and do not let the tool jam.
The next process is started with hollowing by way of Forstner bit or bits if you are precise. A piece of measured tape on Forstner bit provides a depth check. The second Forstner bit opens the hole further. The second part of the hole is continued with an extension on the Jacobs chuck.
Another Dick B tip: keep to speed down when using Forstner bit and check the actual width of the piece.
The lip at the top of the long section allows for fitting the pencil top onto the box base. Remember, the lip on the box head is made to fit the base lip. Similarly, a hole check on box top depth is required. Measure and make the lip fit in a close manner and this is done while leaving the box top in the chuck.
The pencil faces: Dick brought out his cleverly fashioned jig. A boxlike structure that is attached to the frame of the lathe. After some adjustment, fiddling, shifting around, the Router was used to clean off the six faces of the pencil. Some measuring and judging is required. The box is relatively simple and is technically only a guide for the router. It is simply one of the ways in producing the six sides of the pencil – all hopefully matched even and appropriate looking.
Back to the top i.e. the sharp end that that has imitation graphite in it. The lip is mark with Vernier callipers and cut down with a standard skew. It is hoped that you have remembered to leave sufficient thickness to accommodate the flat faces and that they join into a new top.
The finishing touch: The bead lines highlight the end of the pencil in the piece that holds your eraser. Texturing highlights these beads provides a differentiation to the pencil part and hopefully shows up in its glory, with some clean edges. This part of the process is achieved by putting the top of the box/pencil case onto a cylinder mandrel. Holding the box top on with the stem centres will assist safety and avoid any mishaps.
Colouring helps highlight faces, eraser frame and eraser itself. The sharp end of the pen is highlighted by colour or even just a dark felt -tip.
This is a standard box process with some interesting features. The avoiding confusion is easy, just go onto the site, and follow the box making plan.
Tip
The best tip once you enter this process is
measure, measure again, and check that measurement.
Club Meeting: 4 November 2026 Report by: Eoin Jury
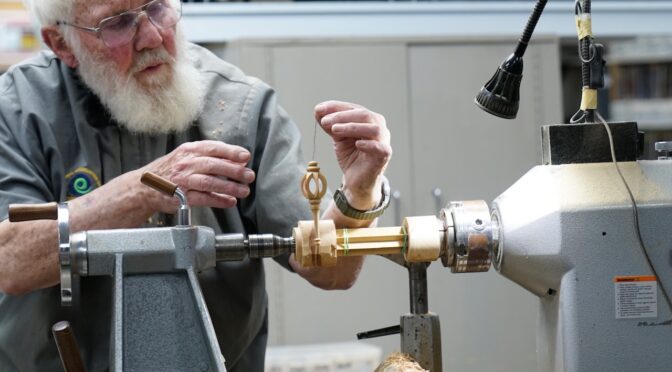
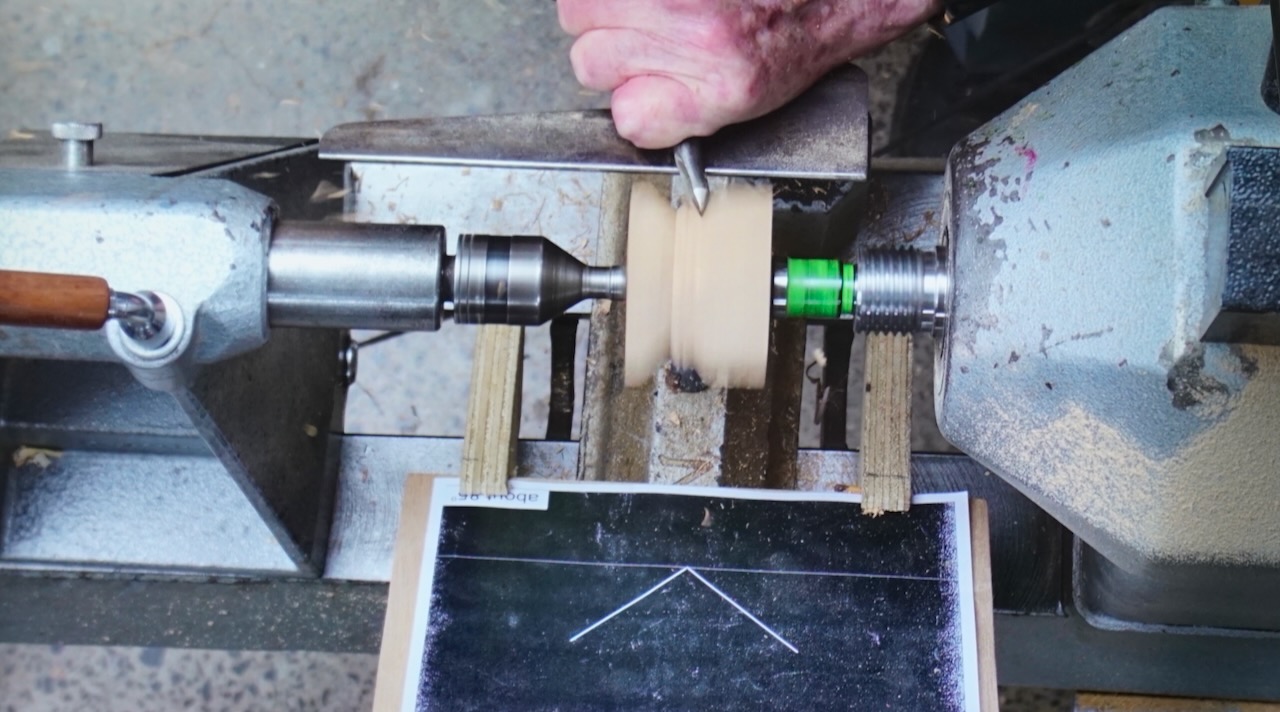
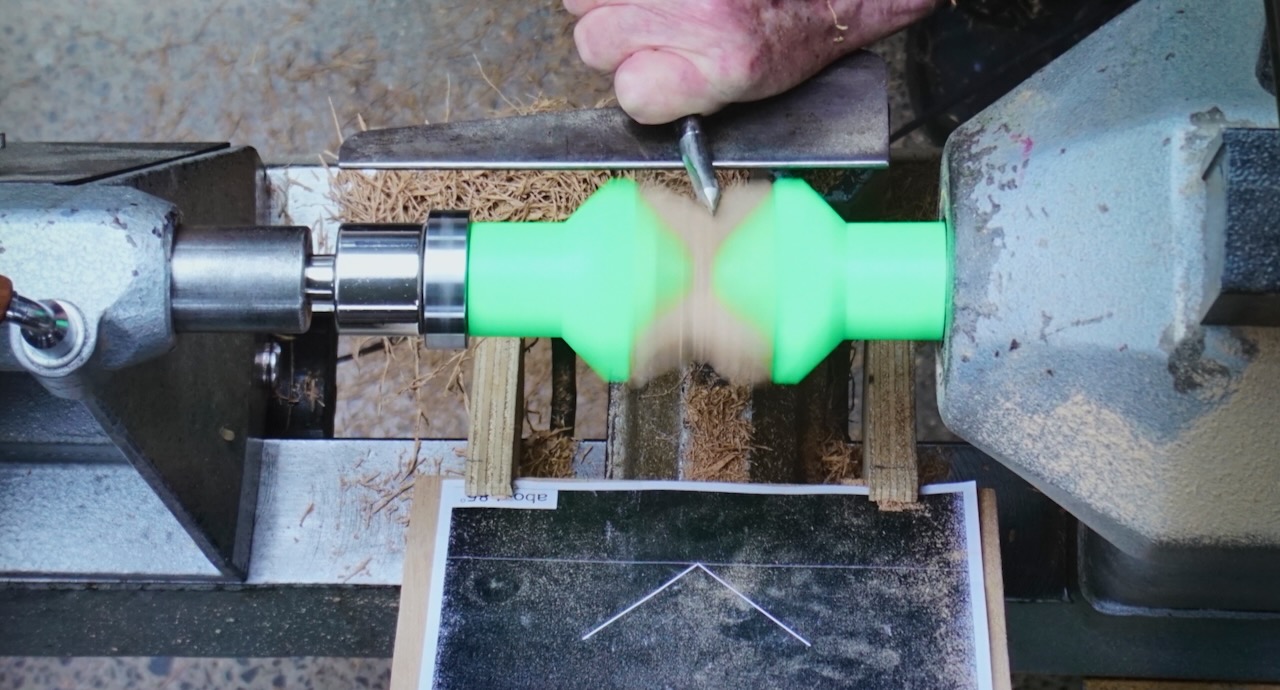
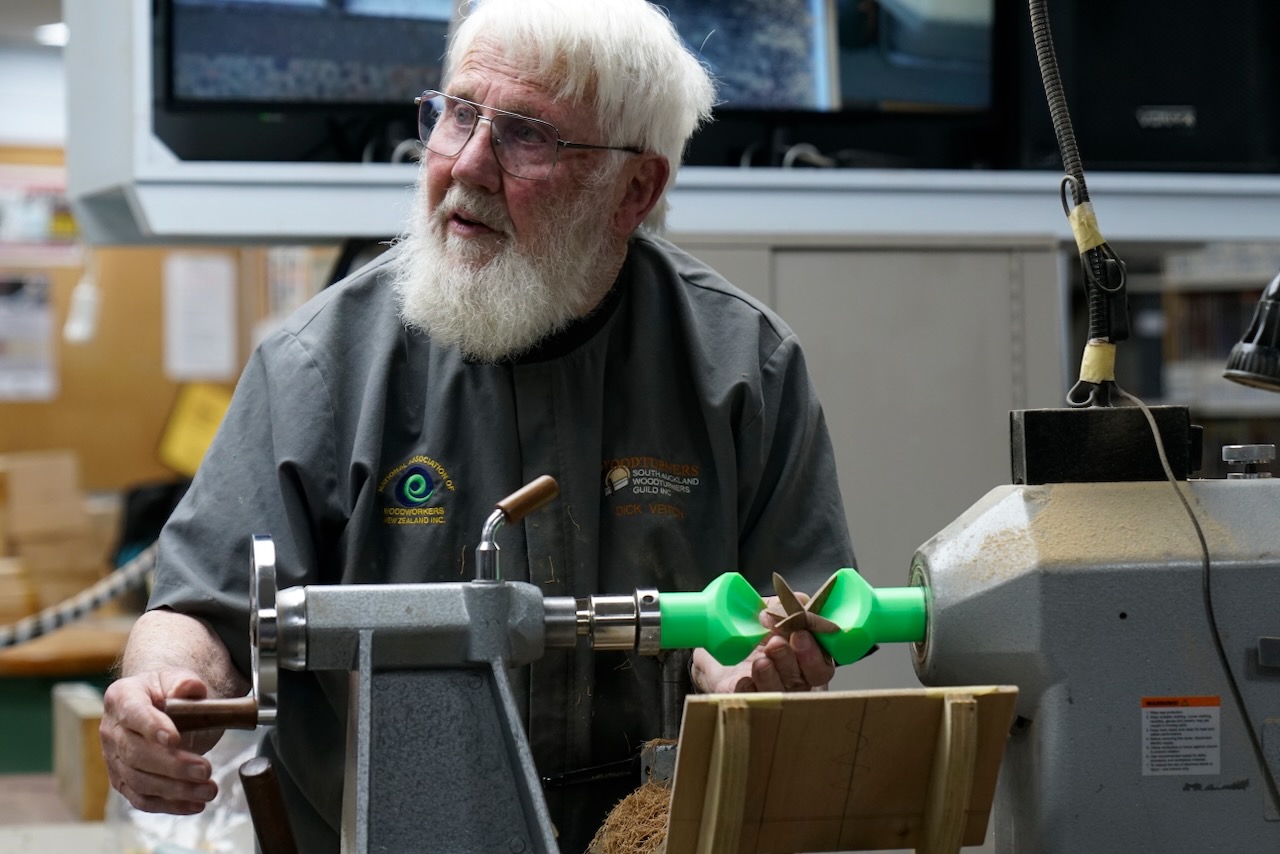
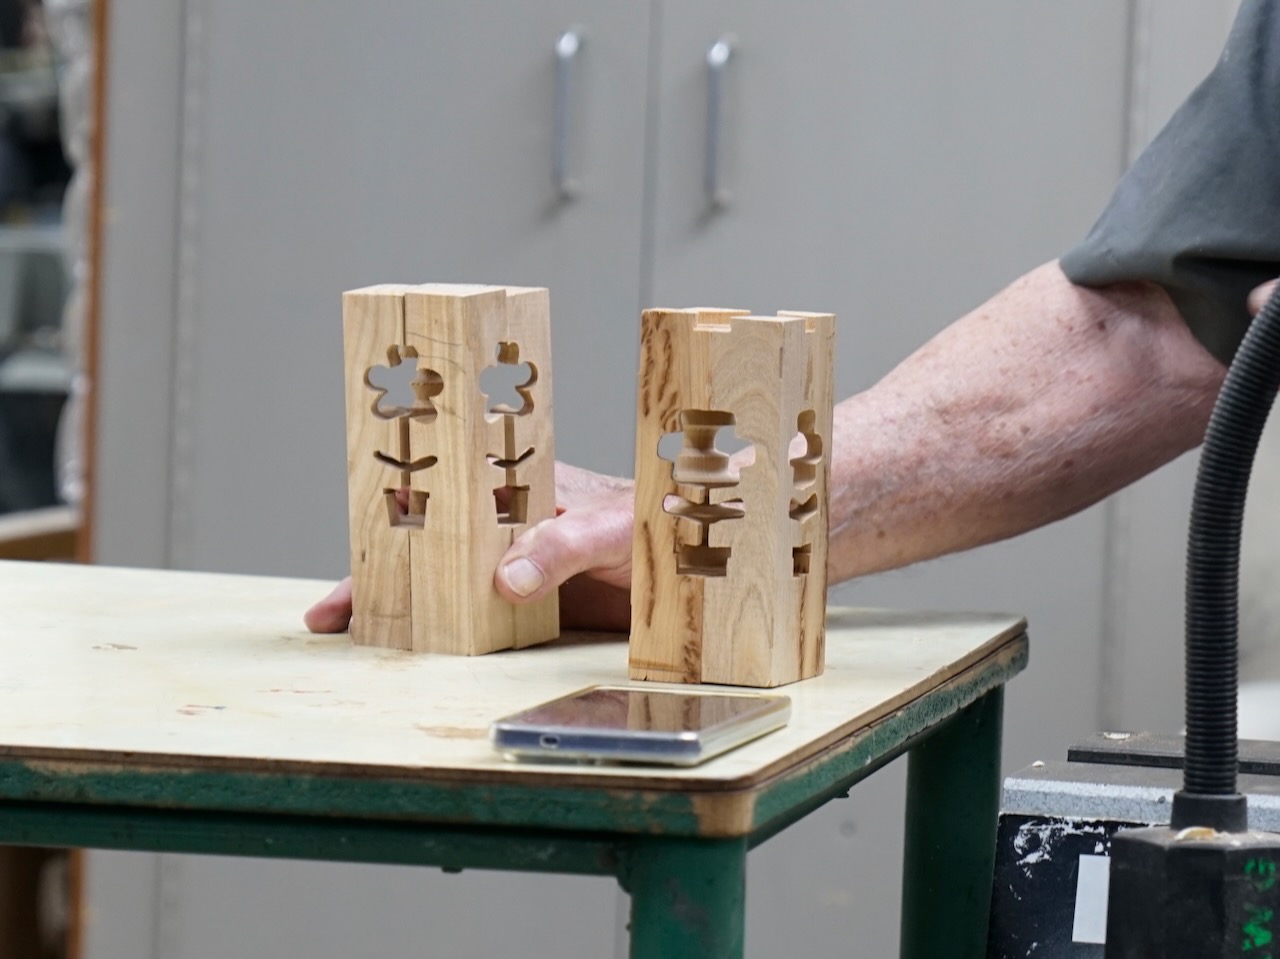
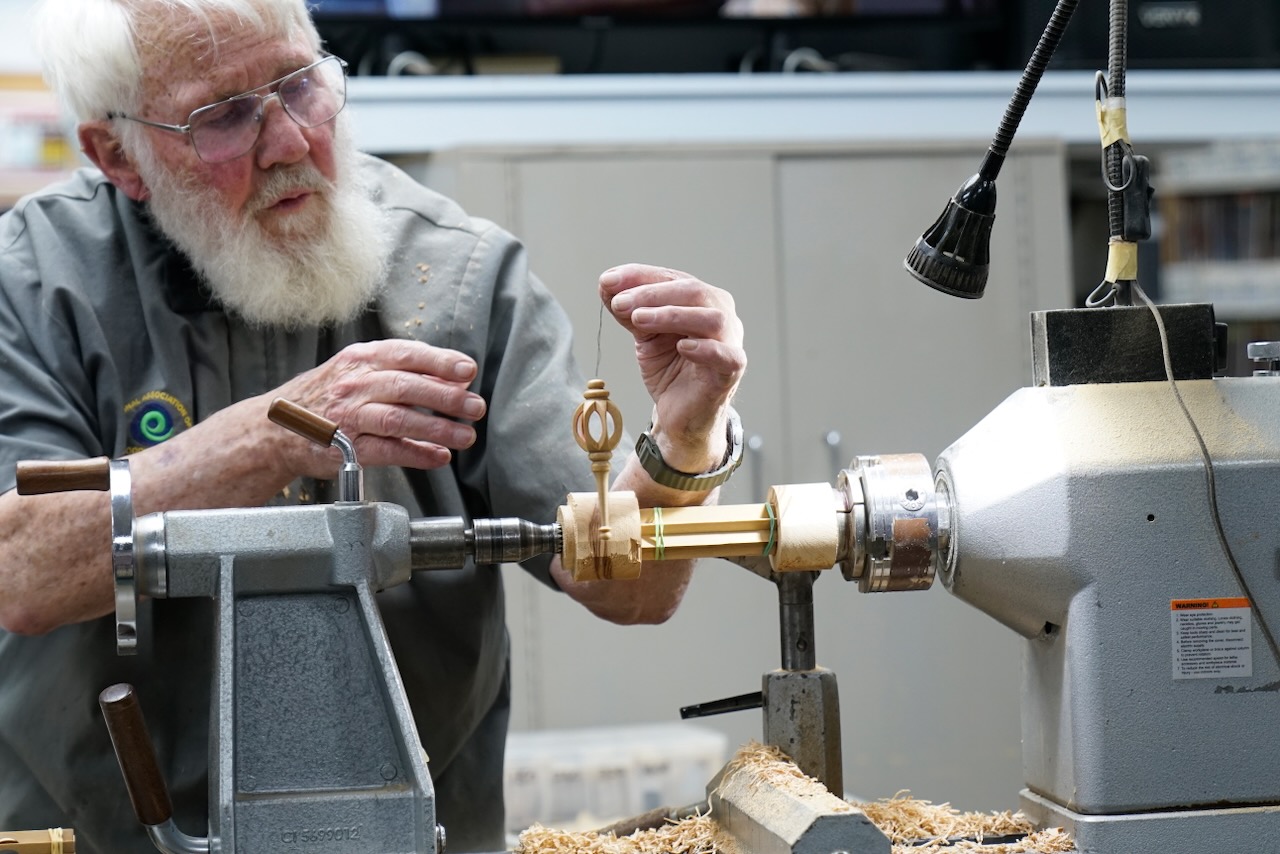
Dick began his demonstration this week with an updated technique to make 8 pointed stars. In the earlier demonstration the stars were quite fragile and the wooden box jigs made to hold them in the lathe did not offer enough support to reliably turn them out. Ian helped out by having holders with headstock threads 3D printed in green plastic for tonight’s demonstration.
Choosing the grain direction for the first cut is important to ensure the most strength is available for the last cut, but in the 50mm cube the grain was variable. The centres were marked with a spike as accuracy is paramount (Dick described it as the most accurate turning he has attempted), the cube was mounted on the lathe and a vee cut using a sighting card mounted on the lathe bed behind the work to get the angle right. With the vee cut, the piece can be mounted in the plastic jigs and the next vee cut using the bright green spinning jigs as a guide. The piece is rotated in the jig to cut the final vee. The star being cut chipped a point, so the next thing to work on is wood choice!
For inside out turning Dick began with four 25mm square pieces of wood about 150mm long, clamping them together at one end with a jubilee clip. The other end is put directly into a four jaw chuck so the four pieces of wood are secured together at both ends. It is not pushed all the way into the chuck, a wide step centre is used at the tailstock to help avold the four pieces breaking apart, and that end centred before tightening the chuck all the way up. The end of the jubilee clip is taped down so that it can’t catch on anything.
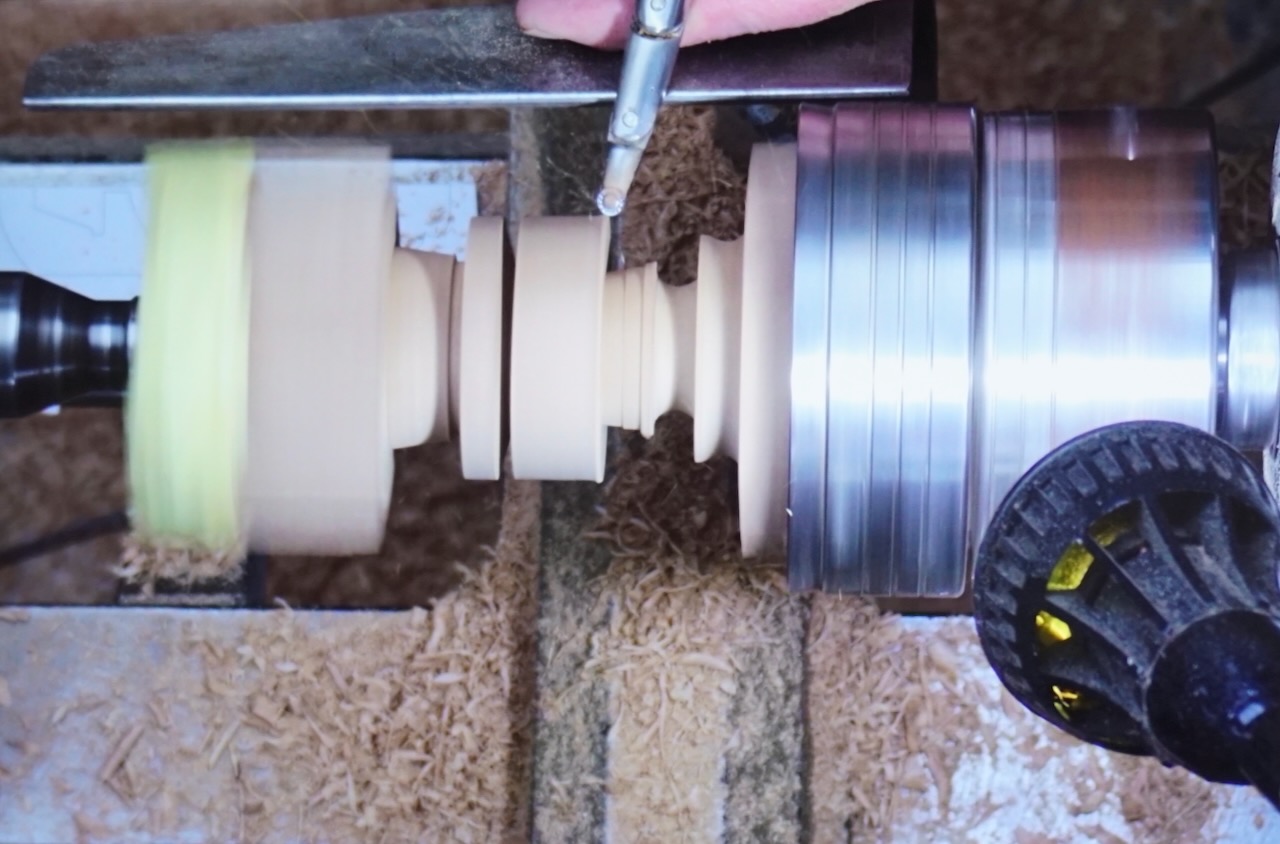
The design being executed is a flower pot (Designs can be found at: https://sawg.org.nz/sawg/wp-content/uploads/2020/11/Inside-Out-Turning-2.pdf). The first step is to mark out the design on the wood in pencil and round out the area that the design will cover with a spindle gouge – no wait … a skew chisel (to keep Strett happy!). The ends of the design are marked with a chisel cut, and the piece rounded between. Once round, the design parts can be penciled onto the piece and then cut with a parting tool starting with the top and bottom of the pot, sloping the cut deeper towards the top of the pot which will appear wider in the final work. A finer parting tool cuts the pot’s wider rim, and then the leaf which is cut on an angle behind the surface which can’t be seen and so has to be fashioned by feel. Back to the skew chisel, the round between the top of the pot and bottom of the flower is reduced in diameter to reflect the plant stem in the final piece.
The flower is the next element, and the parting tool is used to define roughly the form, and then refined with a spindle gouge, again worked into hollow area by feel.
Now the parts can be removed from clamp and chuck then reversed to make the final design.
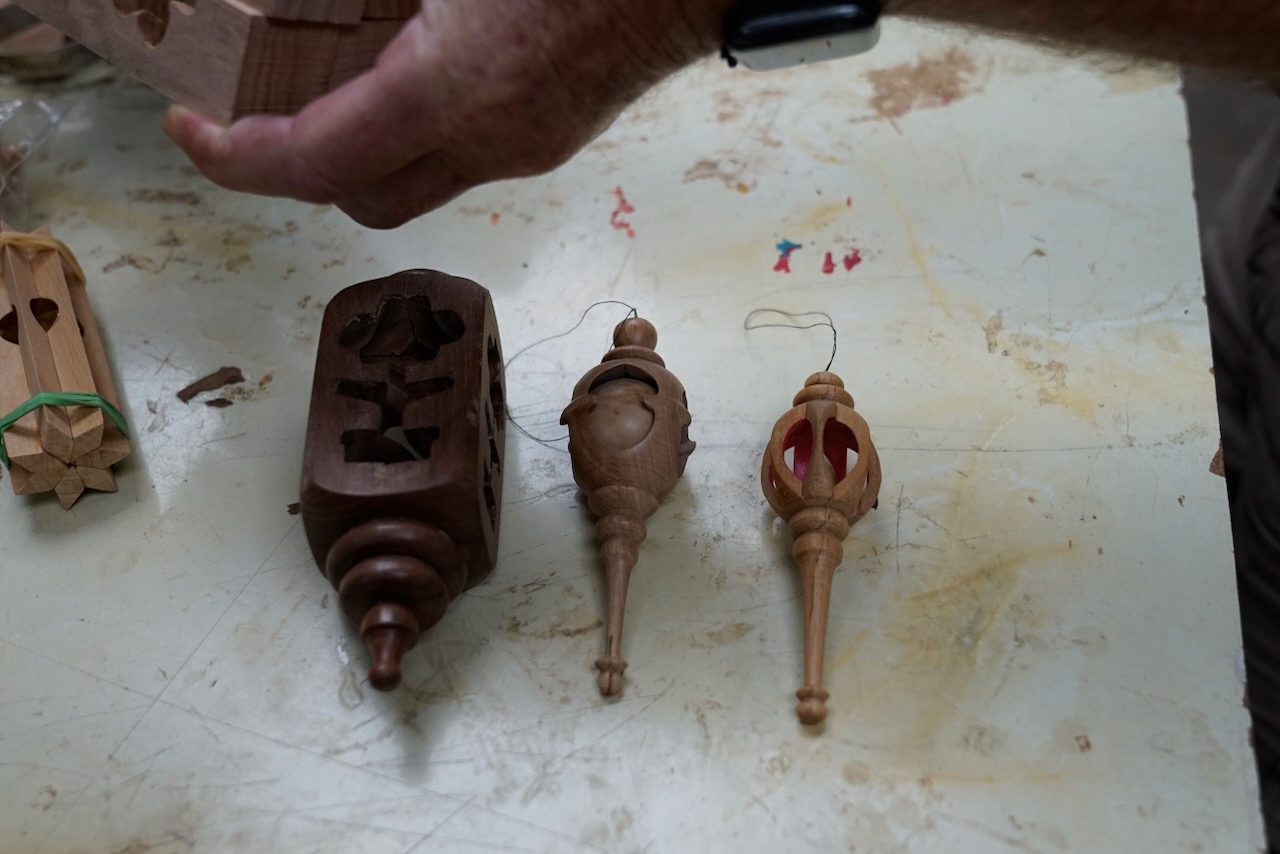
Another variation is an inside out Santa, his front and back silhouette fashioned separately, each on four squares, then reversed and assembled in fours with fronts and backs as appropriate.
The last sample was made with seven pieces of wood, cut at 51.4˚ on.a bench saw and held in a bunch together with rubber bands. A jig consisting of two rounds with hole in the end of each the right size to secure the bunch, one in the head stock and one at the tail stock end. A notch can be cut to form a hollow in the finished piece.
With not enough time left to make any more, Dick showed us some samples of pieces made with the same technique including a finial with a small ball inside.
Club Meeting: 28th October 2026 Report by: Jacqui Oxenbridge
Demonstration used a macrocarpa blank, approximately 230mm long – but the length of the handle you want determines the length of the blank.
Must be large enough to round down to 51mm at the bowl end.
Examples provided included a variety of wood, including ebony, but the comment was made that black maire was not recommended as your first attempt as difficult to hollow out the bowl.
A tenon was made in the handle end and the blank placed in a chuck with the tailstock up for support.
Using a roughing gouge sharpened with a straight up the wings so it could be used like a skew, with the gouge held angled to the side, thumb on top of the tool and travelling over the work slowly so it cuts the entire surface Terry rounded approximately 60mm along the blank at one end down to 51mm diameter. When roughing down work from the centre out as if come in from the end it can splinter and end up in the palm of your hand.
If making a lot of spoons would get them all to this stage to avoid taking the piece in and out of the chuck.
Making the sphere.
Part in at the tailstock end to allow room for shaping the sphere. The parting tool was used again at 50mm towards the headstock (same distance as the diameter of the sphere when turned) cutting down to the same depth. Using a spindle gouge the handle end was rounded down to the level the blank was parted to providing more working space for shaping the sphere.
The 50mm section was then marked with a pencil at halfway and then a further 4, equally spaced lines, were marked either side of the centre mark.
A sphere is a series of flats so using a spindle gouge Terry shaped between the lines – moving from right of the centre to left of the centre – to shape the sphere cutting between the marked lines – start with the tip high, lift the handle to cut, roll the tool and lift at the end.
Once close to a spherical shape a “tool” was used. This tool was a piece of 50mm ID aluminium exhaust pipe from Mr Muffler attached to the end of a 50mm(ish) diameter dowel. A burr was raised on the end of the aluminium with a belt sander and this was moved around the wooden sphere with the lathe running.
Next Terry added a bead at the headstock end and commenced with the roughing gouge and skew to cut the handle down to 12mm diameter.
With the skew he was only using about 3mm of the heel of the tool, slow travel speed to avoid cutting a spiral which leads to chatter and noted that it is important not to push hard on the tool.
At the headstock end of the blank he used the toe of the skew to make a V cut and then used a spindle gouge to shape the end.
Making the spiral on the handle.
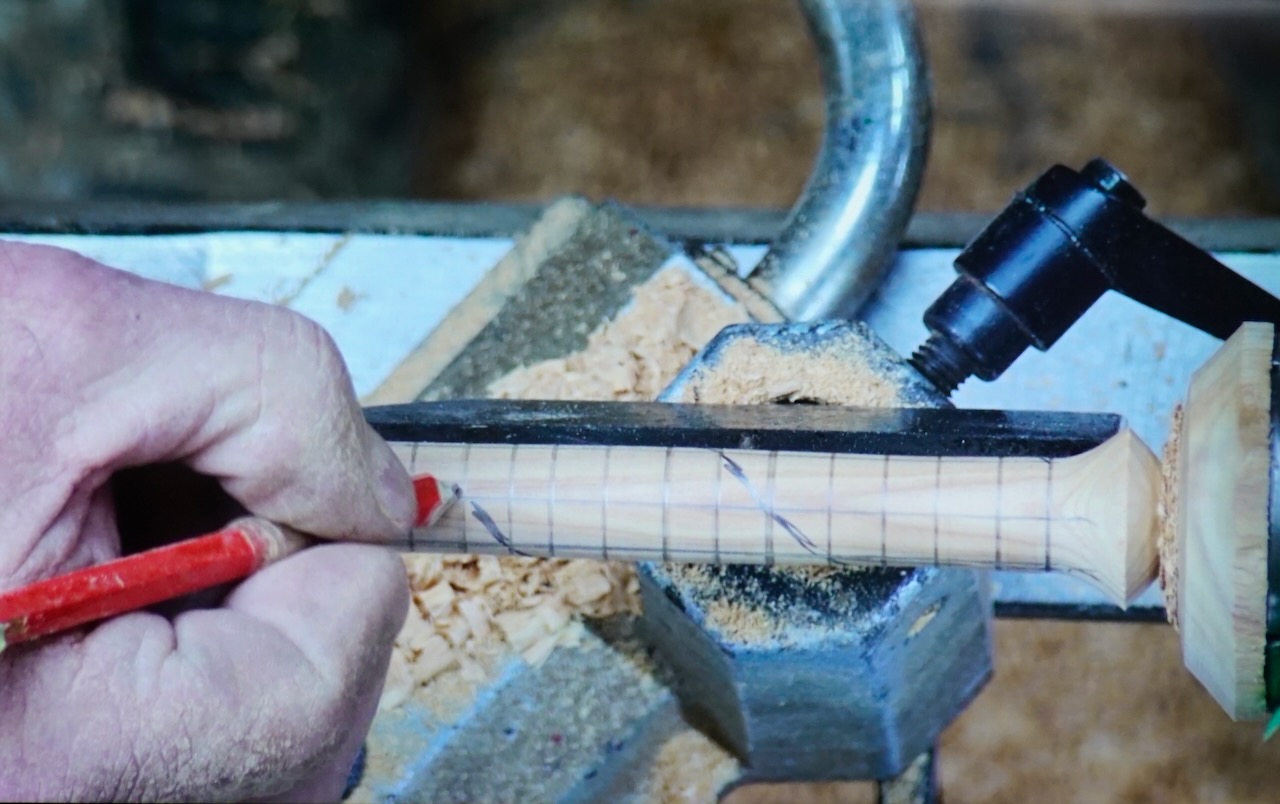
Using the indexing on the lathe (and a jig if you have one or the tool rest set to the centre of the handle) mark a series of evenly spaced lines along the length of the handle. Terry used every second click. Used a soft lead pencil to draw the line and suggested that should aim to keep the lines tidy.
The tighter you get the lines, the closer you get the spiral.
Next add vertical lines, same spacing, evenly along the length of the handle so have a series of squares.
Now, joining corner to corner on adjacent squares draw a spiral line – turn the piece in the lathe – should look like a barber shop post.
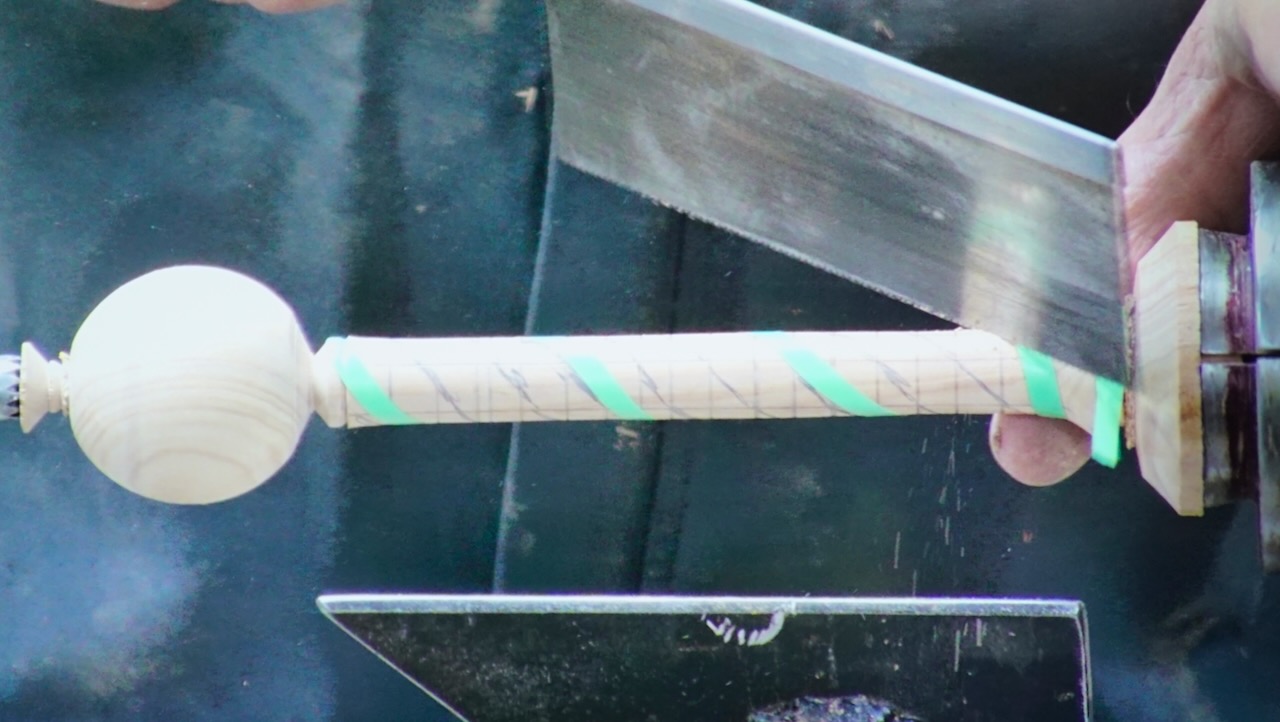
Now can begin to make the spiral. A tip – using thin masking tape mark out the first spiral that you are going to cut to avoid crossing by accident to another spiral.
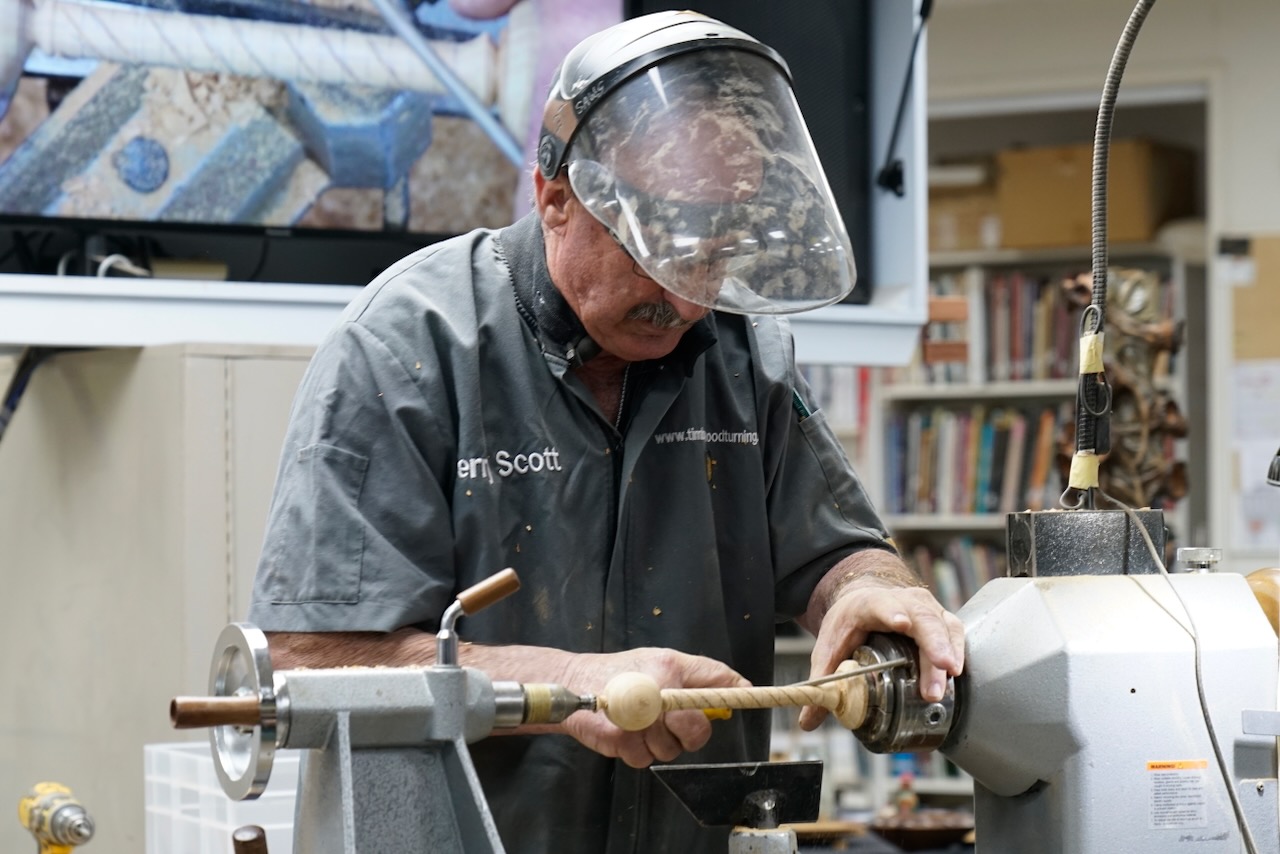
Add some tape on your Japanese saw to the depth you want to cut and begin cutting along the line you have highlighted with the tape.
Once one spiral is complete move on to the next spiral line until all are cut.
Next use a round diamond file (Terry used a 5mm diameter file) to make an indentation along the cut line. Again, turn the piece as you file.
Tip – to avoid mixing the spirals can colour them eg black, blue, red etc.
Once filed to your satisfaction to tidy the spirals can wrap sandpaper around the file. Also round off the tops of the spirals.
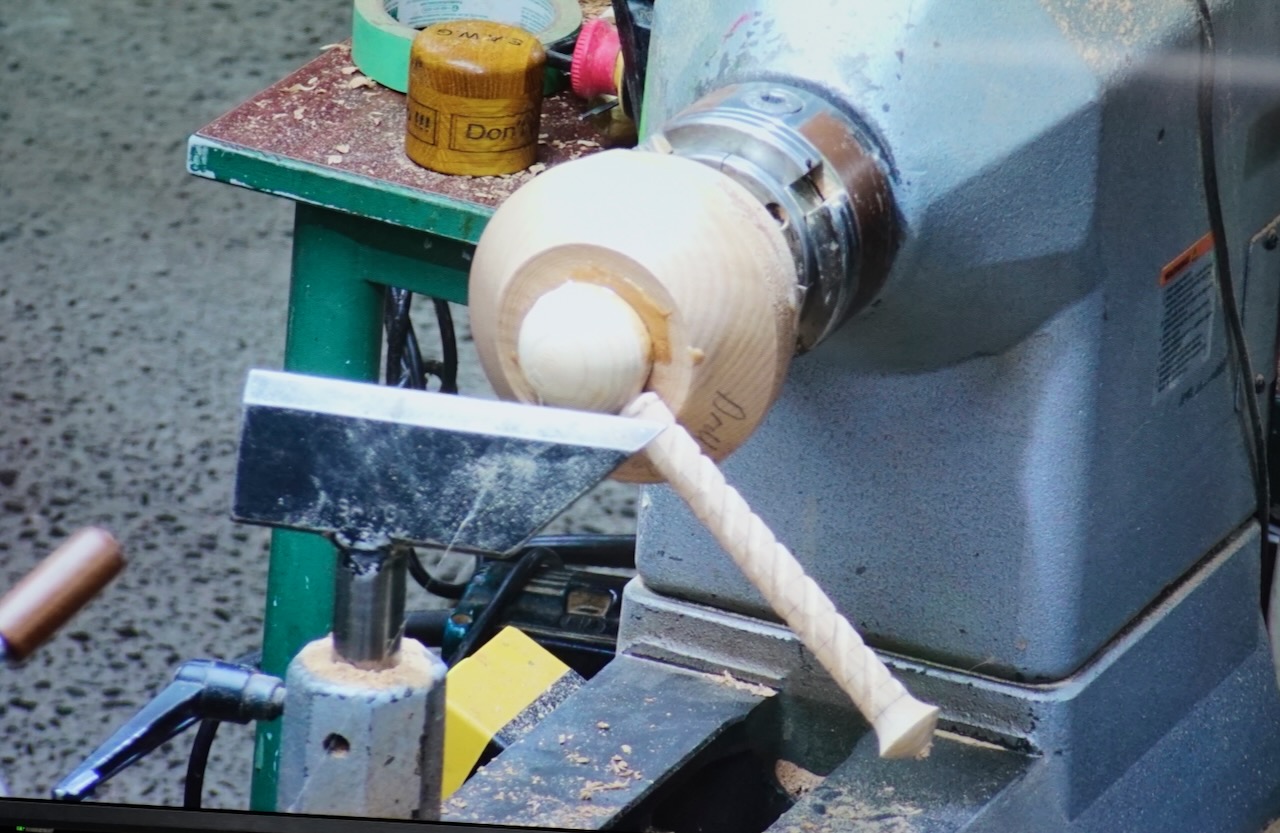
The spoon was now parted from the blank. – Using a spindle gouge, handle down, slice down and remove the bulk at the headstock end leaving a small diameter joining to the waste wood. Repeat at the tailstock.
Hollowing the spoon.
Make a jam chuck. The opening needs to tightly fit the 50mm sphere. The inside of the recess of the jam chuck was undercut to allow the sphere to seat well. Make sure the jam chuck is hollowed sufficiently that there is a void below the sphere when in position. Terry also recommended drilling a hole through the base of the jam chuck so that if the spoon got stuck then can use an air compressor through the headstock to assist removal.
Positioning the sphere needs a little thought – as we do not want to be cutting into end grain it should be lined up so cutting into side grain. For the demo the handle was positioned vertically. It can be placed at an angle and that adjusts the shape of the connection between the handle and the bowl – but does mean you have the handle spinning around further out and so that needs to be taken into consideration with placement of the tool rest and your hands.
The jam chuck can have a recess for the handle and then you can get it more or less level but a 10-degree rake is good. To be extra safe can also hot glue the spoon into the jam chuck.
With a spindle gouge, bevel always rubbing and pushing the bowl in to the jam chuck, hollow the bowl (outside to inside). Remember to always rub the bevel. Treat the end of the sphere like the edge of a thin bowl, drop the handle right down and slice in with the bevel rubbing rather than going straight in. The tool can then enter end rain without a dig-in.
If going to add a lid – put a straight rebate in at the edge of the bowl. This can also help when you are hollowing it if you have a dig in the bevel will come against the rebate and chuck the tool clear.
The sphere is 50mm in diameter. To make a spoon bowl shape it is necessary to true up the face and remove the top 10 – 15mm so now have a remaining depth of 35-40mm. Drill in to the required depth for hollowing – but if you go through it is an olive spoon!
If the handle of the spoon is at more of an angle, then it is possible to cut into the handle and get a nice bit of definition.
Keep your hand behind the tool rest, hand and wrist well anchored to ensure you do not get hit by the handle.
Finish the bowl with a negative rake scraper (sharpen bottom bevel last to raise a burr). Follow the radius of the bowl – do not pull the scraper straight out of the bowl.
If you get a different noise – stop and look – the spoon might have moved in the jam chuck, or you are not rubbing the bevel or there could be a crack.
Kava Bowl
The spoon can be made to use with a Kava Bowl. Terry had an example of a decorated bowl and briefly showed the stages to make one.
Shape the outside of the bowl leaving a very large spigot from which a ring can be made. The feet will be cut out of the ring. Use a parting tool inside the ring and cut a 90mm spigot. The wood between the outside of the spigot and the outside of the ring for the feet should be shaped so that it flows from the outside of the bowl.
Measure with a vernier the depth either side of the ring that the feet are going to be made from as want the bowl to flow through the feet. The depth on the outside should be about 4mm more than the inside. To test if have removed enough wood inside the “feet ring” can use a carver to remove a small portion of the ring to see if the two sides line up.
Mark out where the feet will be placed – 4 in this case but can be up to 10 or 12 feet. Note – the feet on a kava bowl tend to be round, not splayed.
Put a chuck on the spigot, using the faceplate with screw and an adapter in the tailstock, ensure that the bowl is trued up. Remove the faceplate, remove the sharp edge of the bowl.
True up the outside rim. Using indexing mark out 24 sections on the rim. Remove from the lathe.
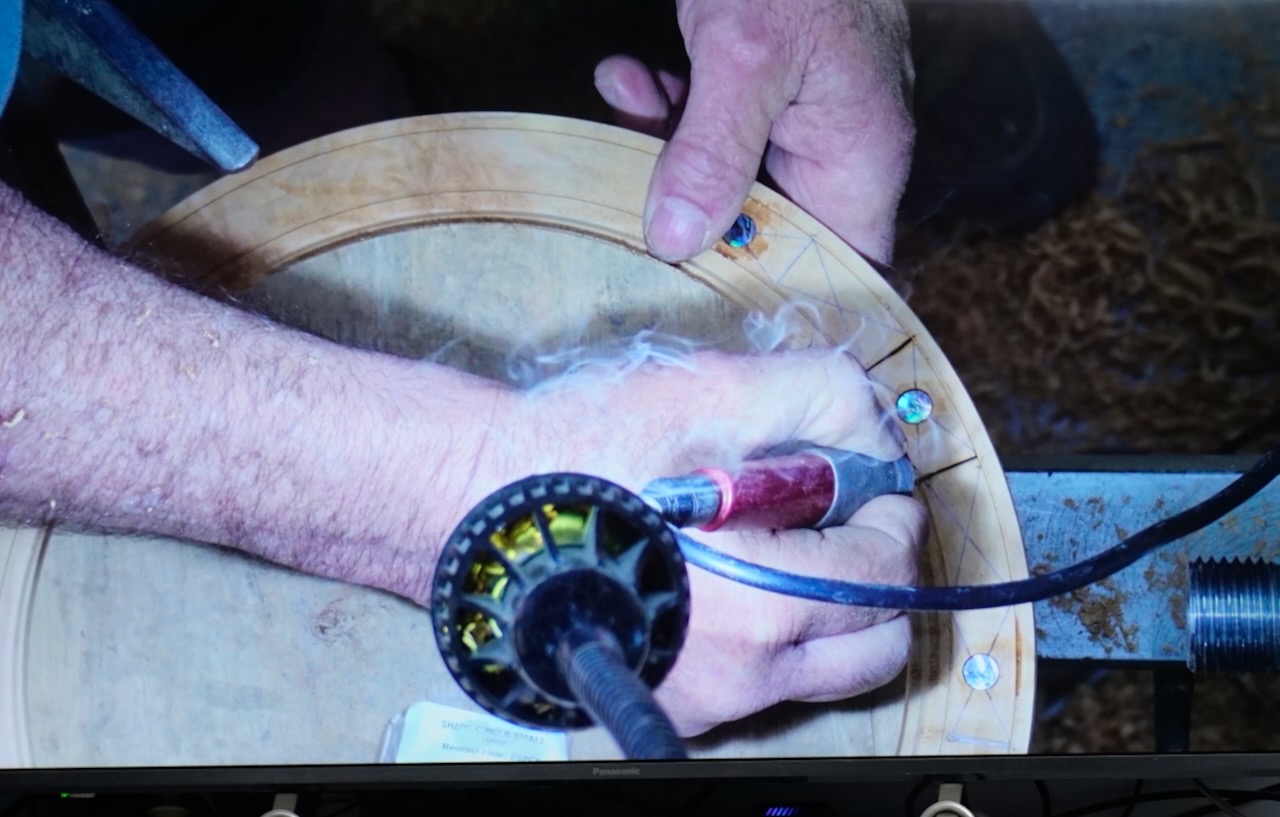
Add a decorative pattern – Terry placed crosses between the indexed lines then he drilled out every 2nd centre of the cross and added a paua dot. In the islands they tend to use Mother of Pearl for decoration or possibly tapa cloth.
Terry then burnt in lines in each of the four triangle sections of the 24 marked rectangular sections. The lines can have cultural significance or make a pattern up. It is like a canvas to tell a story.
Club Meeting: 24 August 2026 Report by: Thinus Oberholzer
Our demonstrator for the evening was Tom Logan from Franklin, who opened with the comment that he felt a bit like “an Eskimo showing people how to build an igloo.” It was a fitting introduction from someone who has spent a lifetime learning, creating, and solving problems across a remarkable range of trades and professions.
Before retiring in 2019, Tom worked for 22 years as a telecommunications technician and also spent time in timber and hardware sales, canvas and vinyl manufacturing, signwriting supplies, engraving equipment, electrical wholesaling, rest home maintenance, and farm gate manufacturing. Describing himself as a “Jack of all trades”, Tom’s wide-ranging skills were evident throughout the evening’s demonstration.
A Late Start to Woodturning
Tom’s woodturning journey began only seven years ago after visiting the Franklin Woodturners Club display at the Waiuku Steel & Wheels event. Encouraged by Gavin French and other club members, he turned his first project, a small end-grain lidded box. Interestingly, he still has that first piece today and encouraged newer turners to keep some of their early work as a reminder of how much their skills improve over time.
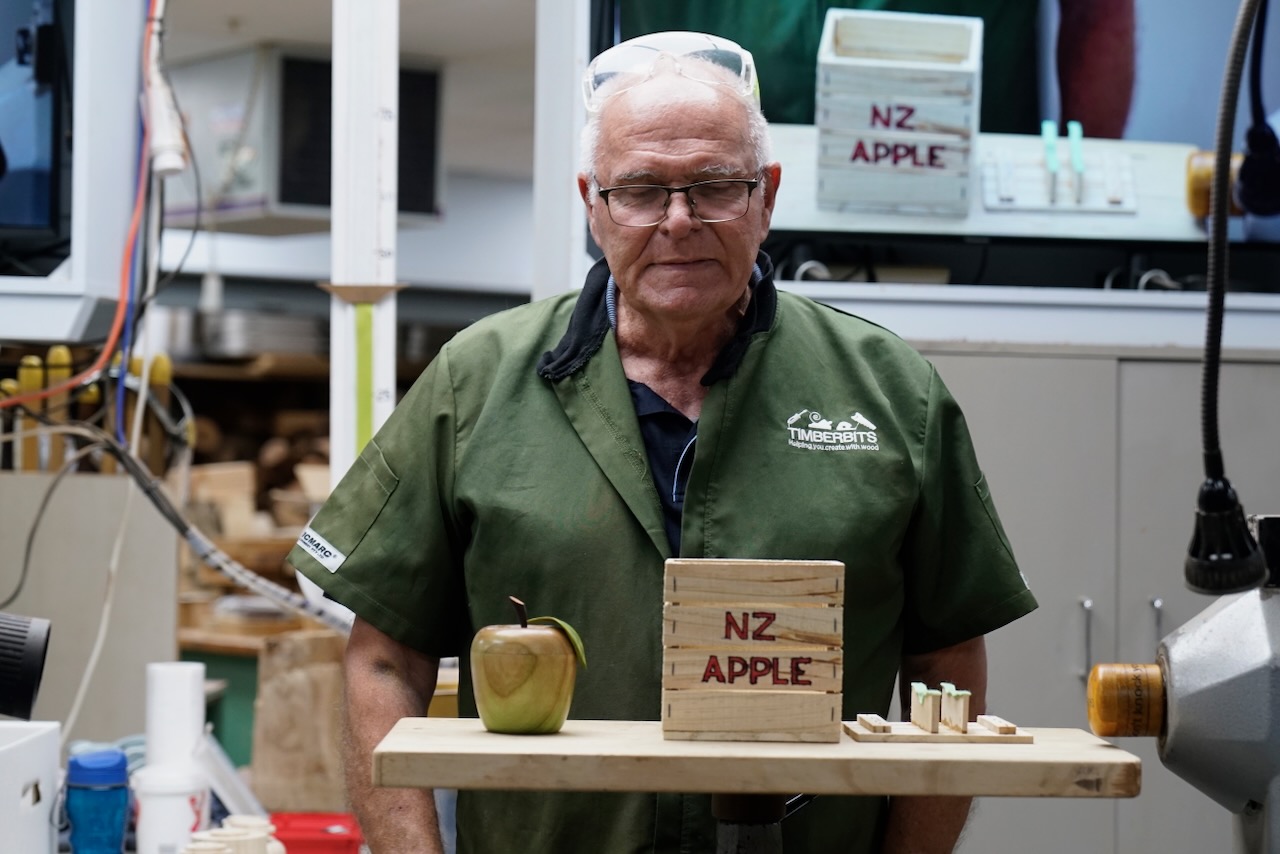
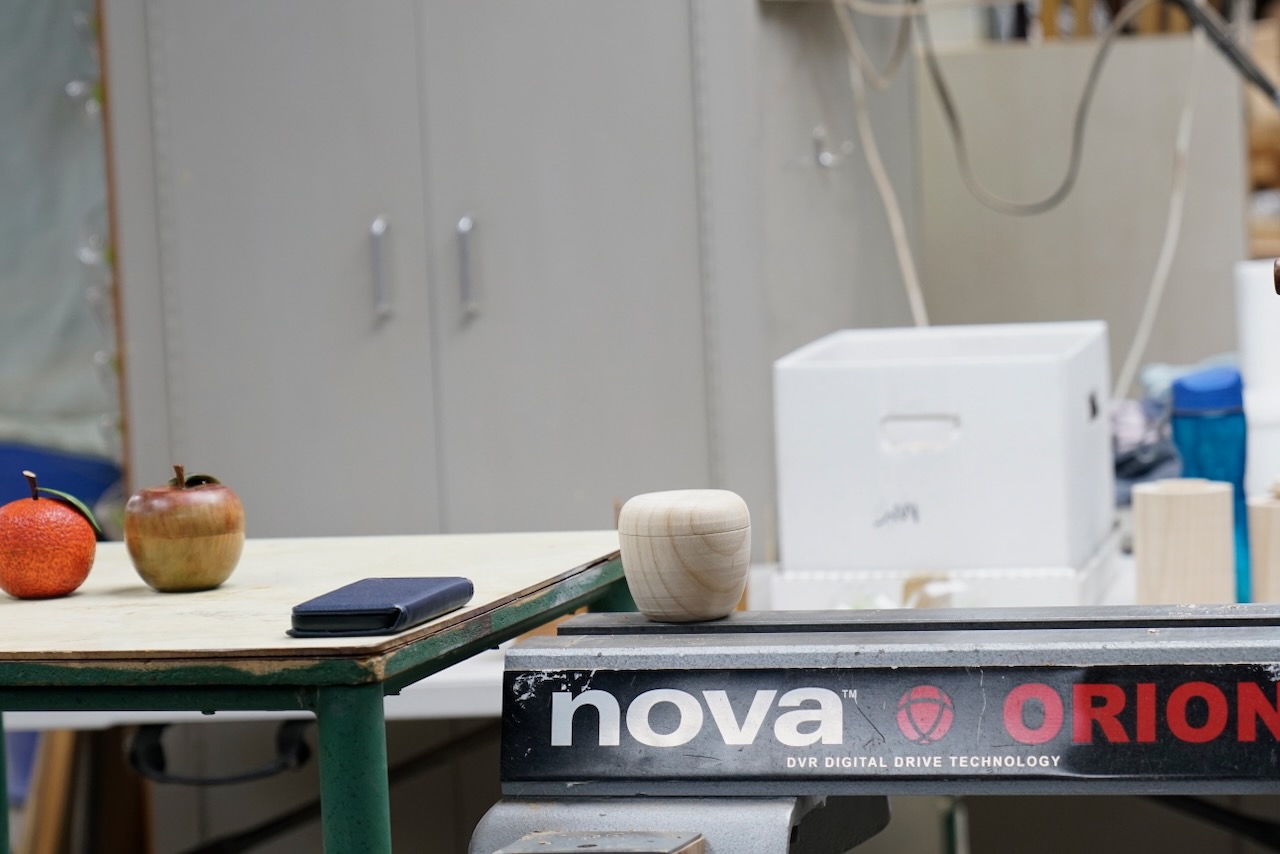
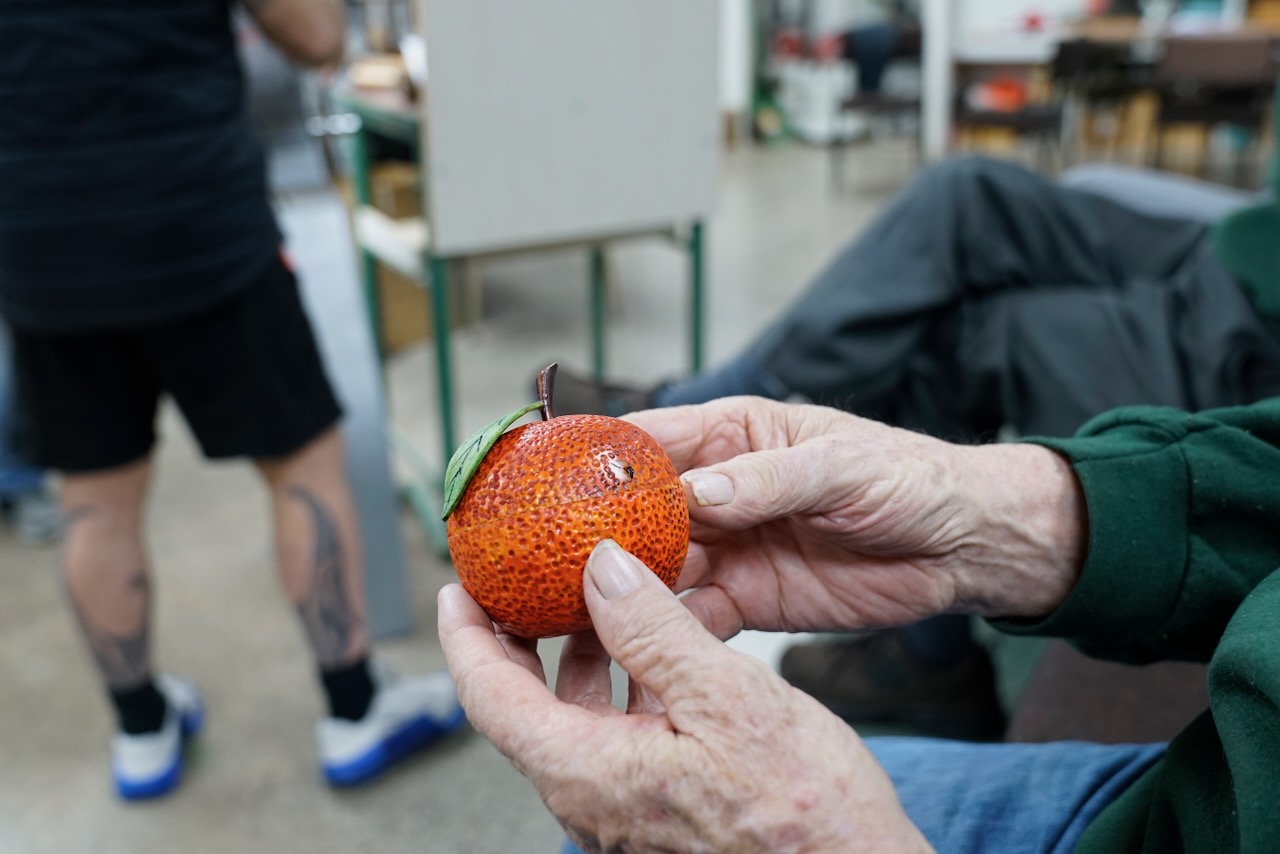
Like many turners, Tom initially learned by reproducing ideas he admired before gradually developing his own style. Drawing inspiration from woodturning, pottery, decorative arts, and online sources such as Pinterest, he has developed a distinctive range of fruit-inspired boxes, with apples and pears becoming a particular speciality.
The Apple Box Demonstration
The evening focused on one of Tom’s popular Apple Lidded Boxes, a project that combines spindle turning, hollowing, decorative carving, colouring, and clever design details.
Starting with a square block mounted between centres, Tom turned the blank round and formed chucking tenons at each end before shaping the overall apple profile. Careful consideration was given to grain orientation to achieve the best visual effect in the finished piece.
The lid was then parted off at the widest point of the apple to preserve the grain match and simplify the final shaping process. Both the lid and base were hollowed, maintaining an even wall thickness while leaving sufficient material for the decorative fittings that would be added later.
Once hollowing was complete, the lid and base were reassembled and carefully aligned to ensure the grain flowed seamlessly across the join. The exterior was then refined before drilling holes for the stalk and calyx. The remaining tenons were removed using jam chucks, followed by the final sanding and finishing of the box.
The Details Make the Difference
What elevates Tom’s apple boxes from a simple lidded container to an attractive display piece are the additional decorative elements.
The calyx is turned separately from a darker timber and textured with pyrography to give it a natural appearance before being fitted into the base of the apple.
The peduncle, or stalk, is also turned separately. After turning, additional shaping and carving create the gentle curve found in a real apple stalk, adding an extra level of realism.
A decorative leaf is then cut, shaped, textured, and attached to the stalk area. Combined with the carefully shaped stalk and calyx, the leaf completes the illusion of a freshly picked piece of fruit.
Tom also discussed the use of dyes and colouring techniques to enhance the apple, stalk, and leaf. While the boxes look excellent in natural timber, subtle colour can further accentuate the fruit-like appearance and help draw the eye to the finished piece.
An Inspiring Evening
Tom’s demonstration showed how a relatively straightforward lidded box can be transformed into something unique through imagination, careful planning, and attention to detail. His practical approach, combined with his willingness to experiment and adapt ideas from many different sources, provided plenty of inspiration for members.
The finished apple boxes were greatly admired, and members departed with several new ideas for adding character and creativity to their own turning projects.
Club Meeting: 21 October 2026 Report: AI, edited by Jacqui Oxenbridge
Overview
Strett demonstrated how he turns a Pinard stethoscope or horn, the traditional wooden foetal stethoscope used by midwives to listen to an unborn baby’s heartbeat. Originally invented by Pinard (a French doctor) around 1860 it continues to be used today by midwives looking for a more natural stethoscope device.
Strett has made around 250 of them over the past few years, most for one regular customer who purchases 50 at a time. Strett has refined the process into a repeatable batch routine (usually about ten at a time) which reduces the time taken when drilling and shaping by avoiding the need to keep changing tools.
The demonstration also covered skew chisel practice, drilling a through-hole from both ends, shaping the bell and hearing end, and a bonus variation: a wooden amplifier for a mobile phone.
Tools & Materials
Item
Details
Timber
Spindle blanks approximately 180mm long, 65mm square. This demo used a piece of kauri gifted by Colin Mitchell. Strett uses NZ native timbers and individually decorates each Pinard so when the batch is delivered, no two are the same.
Lathe & chuck
Between centres to start, then a chuck gripping the spigot.
Roughing tools
Skew chisel (used here for roughing and for cutting spigots); roughing gouge is the usual alternative. Parting tool is the normal way to cut spigots, but a skew can also be used.
Measuring
Vernier calipers were used to measure the spigot and the diameter of the bell end. (Note: metal calipers should be used as a plastic pair was once melted by the heat of a spinning blank).
Drilling
10 mm drill in a Jacobs chuck, with a little wax melted onto the end as lubricant. Forstner bit is a possible alternative.
Shaping
30-degree spindle gouge; a hollowing tool for tidying the bottom of the bell.
Finishing
Sandpaper, an 8 mm dowel with sandpaper for the hole, sanding sealer, then spray lacquer.
Other
Tailstock with live centre, wax for lubrication of the drill, compressed air or a small air pump for clearing dust.
Key Settings & Measurements
Item
Value
Reason
Turning speed
About 2000 RPM
Roughing and shaping
Drilling speed
About 750 RPM
Slower speed for the long 10 mm hole.
Hearing-end spigot
46 mm diameter
Fits the 50 mm chuck jaws.
Bell-end spigot
55 mm diameter (55.5 mm achieved)
Same size every time, so one jam chuck fits every Pinard.
Through-hole
10 mm, drilled from both ends
Must meet in the middle and go fully through.
Hearing end thickness
About 1 mm heavier than looks neatest
Stops the earpiece breaking if dropped.
Step-by-Step Process
Mount and round the blank. Mount a spindle blank between centres, find the centre and make a mark for the drive centre. Check the blank spins freely and everything is clear. Wear a face shield and start at about 2000 RPM once it is firm and tight.
Take off the corners. Strett used a skew chisel rather than a roughing gouge. Rub the bevel and work from the heel into the cut; if the bevel is rubbing, a catch is unlikely. He also demonstrated cutting backwards with the skew, using the bevel to support the fibres. Set the tool rest at the right height first.
Cut both spigots. Cut a 46 mm spigot at the hearing end and a 55 mm spigot at the bell end, using the skew or a parting tool. Check with vernier calipers.
Mount in the chuck. Grip the bell-end spigot in the chuck. Check the blank runs true, tighten, and take a little material off the hearing end, but leave enough of the face to work from when the piece is turned around.
Drill the first hole. With the lathe at about 750 RPM, drill the 10 mm hole from the hearing end. Wax the drill end to reduce heat and squeaking. Retract the drill often to clear shavings and do not extend the quill too far, or the drill can pop out.
Shape the hearing end. Use the 30-degree spindle gouge to shape the earpiece. Start with the tailstock up, use two or three push cuts, then switch to a draw (pull) cut where the grain would otherwise be cut uphill. Sand lightly and apply sanding sealer.
Reverse and drill from the other end. Turn the piece around, centre it again with live centre, tighten, and then drill the hole from the other side at 750 RPM so the two holes meet. Do not assume it has gone through: check it. A puff of air that blows sawdust out the other end confirms it.
Shape the bell. Back at 2000 RPM, shape the outside of the bell first, then hollow the cone with the 30-degree spindle gouge, working a section at a time and keeping timber at the centre for support. Do not go so deep that it rattles. A hollowing tool tidies the bottom more easily than the gouge. Go only as deep as a finger can still reach to sand it. Shape the outside of the bell end and move towards the earpiece.
Finish the outside shaping of the earpiece. Remove from the chuck and turn around. Support the piece with the live centre (in the earpiece, tailstock end) and a jam chuck (in the bell at the headstock). By making the diameter of the horn the same each time the jam chuck can be reused. An alternative would be a small 10 mm dowel that fits the drill hole, so the Pinard does not wobble while shaping the outside. Complete the outside shaping, including any beading, burnt cuts etc. Leave the neck of the earpiece slightly thicker for strength, then sand the outside.
Finish. Spray with lacquer which can be wiped with water or disinfectant.
Tips & Safety Notes
Making about ten at a time avoids constantly swapping drill bits and live centres.
Check that both the tailstock and the chuck are tightened.
Demonstration reminder: Strett pointed out that going into end grain with a roughing gouge, or putting a finger inside a spinning piece, are things beginners are taught not to do. Demonstrators should model good habits, particularly with new turners present.
Air for clearing dust is better than blowing by mouth.
Discussion & Questions
Strett was asked about drilling just one deep hole with a long drill or using a Forstner bit to remove more wood from the bell end. He had not considered a single long drill and had only recently used a Forstner bit for the first time.
Reading a vernier: look for the one line on the lower scale that lines up exactly with a line on the main scale; that gives the decimal part of the reading.
Bonus: Phone Amplifier
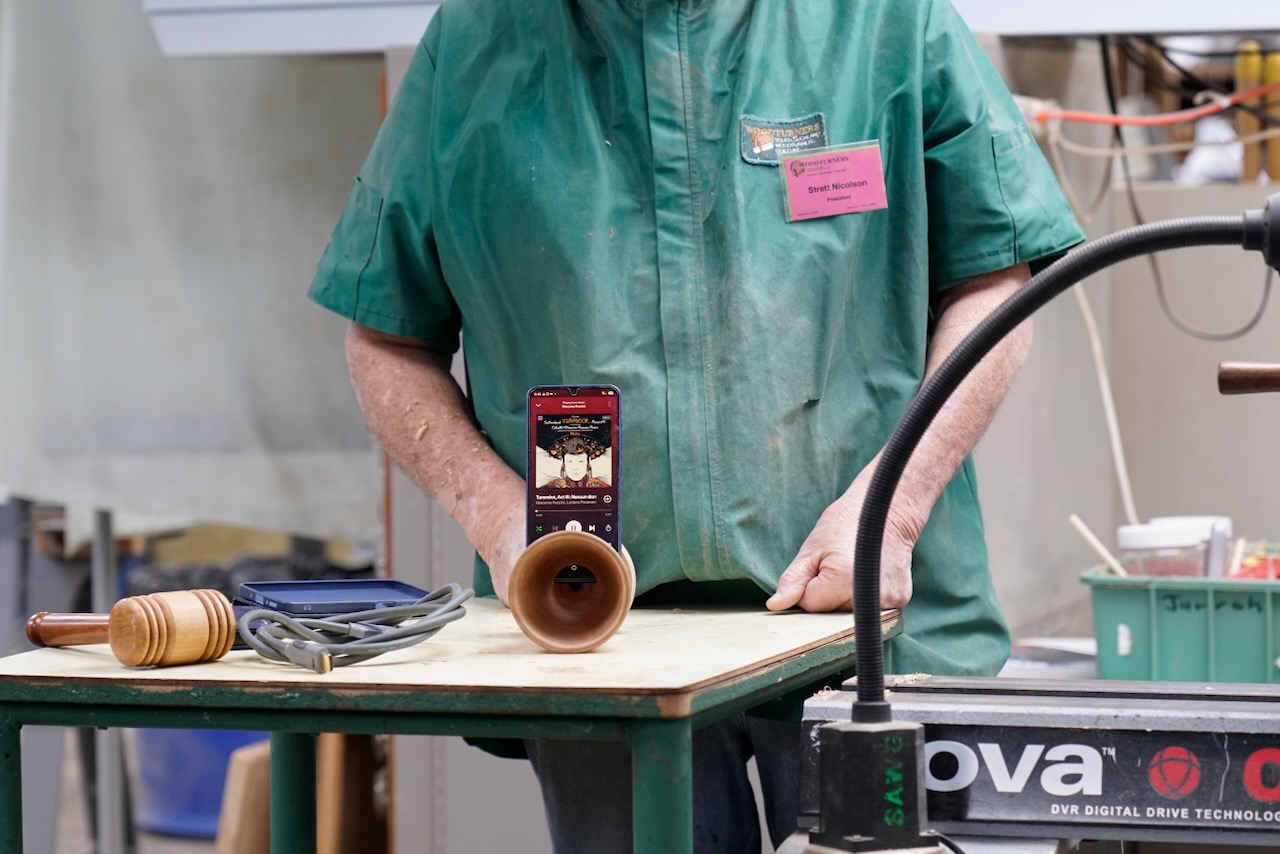
With a few minutes left, Strett showed a phone amplifier made by the same process, inspired by Rob’s earlier cell phone speaker. A Forstner bit was used for the larger cavity. He initially drilled the hole all the way through, then realised the sound should not escape out the back, so he added a small closing piece. A phone was placed in it for a quick sound test, with music played, and Dick felt it made a difference to the sound.
Club Meeting: 23 September 2026 Report by: Kevin and his AI Helper
Overview
Kevin’s first demo for the club covered turning a two-piece, lidded box in a teardrop (or “onion”) profile, turned long-grain from a single blank and split apart partway through so the grain continues to match across the lid and base once reassembled. He brought along several earlier practice pieces — including one in Rimu and one in an unknown wood — to show the shape at different stages and discuss what had gone wrong along the way, before demonstrating the process live on a fresh blank. Time ran short, as is common for a first demo, so the piece shown was left partly refined rather than fully finished — the notes below combine Kevin’s own written process notes with what was covered live, including a couple of useful suggestions from the floor.
Materials & Tools
Item
Notes
Chucks
100mm and 75mm
Step centres (drive & live)
Used at both ends for initial mounting between centres — sized to suit the blank
Tailstock chuck mount
A second chuck mounted via a Morse taper adaptor in the tailstock, used to keep the lid and base aligned before fully separating them
Spindle roughing gouge
For initial rounding of the blank
Spindle gouge
For shaping the teardrop profile
Thin parting tool
Used for the critical cut separating lid from base — a thin kerf helps the grain line up better once rejoined
Flush-cut / pull saw
A Japanese-style saw with no set on the teeth (cuts only on the pull stroke), used to finish separating the two halves once the parting tool can’t safely go any deeper
Jacobs chuck + Forstner bits (35mm)
For boring out the centre of the lid before hollowing
Outside callipers
For matching diameters between lid and base
Masking tape
Used both as a marking guide on the tool rest, and to hold the lid and base together for final shaping and sanding
Sandpaper
Through to 320 grit
Design & Proportions
Timber is used long-grain, with end grain at the top and bottom of the finished piece. Before starting, size the blank so the finished piece will end up at roughly 130–150% of the blank’s diameter — for example, a piece meant to finish around 130mm at its widest point wants a blank close to 195mm long overall, plus about 20mm extra at each end to leave room for spigots.
“Measure twice, cut once, and panic quietly the whole time.”
The high point of the teardrop’s curve (the widest part) should sit at roughly one-third of the way along the finished length, not counting any separate foot.
Method
Mounting & Roughing
Mark the approximate centre at both ends and make a small indent with an awl to seat it between centres.
Mount between centres using a step drive centre at the headstock and a live step centre at the tailstock, sized to suit the blank. Make sure everything is firmly locked up.
Round the blank down to approximately the diameter wanted for the widest part of the finished box.
Turn a spigot at the tailstock end sized to suit the chuck that will hold the base. Reverse the piece — that end into the chuck, the other end supported on the live centre — and turn a matching spigot on that end too (this end can go in a smaller chuck, since it’s eventually turned down to a point).
Put masking tape on the tool rest and mark the top, bottom, and high-point positions on it as a cutting guide — marks made directly on the spinning wood tend to disappear too easily to rely on.
Shaping the Profile
“Turning a circle is easy. Turning a teardrop is just a circle with an identity crisis.”
Shape the base end first, including a fairly steep taper near the spigot down toward the foot’s finished diameter — a parting tool can establish this diameter early on.
Shape the upper part of the teardrop, checking the profile from above regularly and using the tool rest marks as a length guide. Bring it to the rough final shape, but stop short of a fine point — enough thickness needs to remain here to keep the piece securely held in the chuck while the inside of the lid is later hollowed.
Sand the outside smooth through to 320 grit before separating the two halves.
Separating Lid from Base
Mark the separation point and begin parting through with a thin parting tool — a thin kerf helps the grain match up better once the two halves are rejoined later. Part in only as far as is safe (the tool gets hot, especially fine ones), then stop the lathe and lock the chuck.
Finish the cut with a flush-cut/pull saw, rotating the piece by hand and sawing in from different points around the circumference until the two halves are nearly separated.
Before fully parting through, mount a second chuck in the tailstock (via a Morse taper adaptor), bring it up to the piece, and tighten it onto the still-attached section. This keeps the lid and base captured on their own chucks and correctly aligned relative to each other, rather than risking them coming apart out of true.
Cut through the remaining connected wood, then remove the lid (still on its chuck) from the tailstock, followed by the base and chuck from the headstock — swap the lid onto the headstock in its place, keeping each half mounted on its own chuck throughout.
Hollowing the Lid
Using a Jacobs chuck and an appropriately sized Forstner bit in the tailstock, bore out the centre of the lid. Measure the target depth from the outside first, and make sure the bit’s diameter stays well within the piece at that depth given the final outside shape.
Turn a small registration recess just inside the outer edge of the lid — about 1–2mm in and roughly 1mm deep. This recess is used later as a fit-testing template when turning the matching recess into the base.
Turn out the rest of the lid’s interior to the desired wall thickness, rounding over the flat left by the Forstner bit to follow the intended inside profile.
Hollowing the Base to Fit
Mount the base and hollow the interior with a parting tool, working from the centre outward in small cuts, leaving the outer 4–5mm untouched initially.
As you approach the edge, cut a matching recess to the same depth as the one turned in the lid, stopping the lathe frequently to test the fit of the lid directly against the base.
“The hardest part of a box is making a lid that fits. The second hardest part is pretending it fits on the first try.”
Once satisfied with the fit, sand the inside to 320 grit, taking care not to round over or damage the rim.
Rejoining & Finishing
Refit the live steb centre in the tailstock, bring the lid and base together, and tighten gently. Do a final light sanding pass around the join, since a small amount of material is inevitably lost during parting and rejoining.
Wrap masking tape around the joint to hold the two halves together securely for the final shaping — position it so it won’t lift or catch while spinning.
Turn the final point at the top down as far as practical, then remove the tailstock. Drill a small hole in the remaining waste wood at the tip and use it as a jam-chuck point to support the piece while finishing the very top and completing all outside sanding and your chosen finish.
Remove the tailstock and lid, then part off the base from its chuck to complete the piece.
Tips From the Floor
For a more consistent curve, a shop-made template of the lower “sphere” portion of the teardrop can be held against the piece as a guide while turning — useful since eyeballing a smooth, continuous curve (rather than one with a flat spot partway through) is genuinely difficult freehand. The same template idea, used as a thickness gauge, can also help keep the wall an even thickness on the inside.
To make grain matching between lid and base easier without losing extra material at the join: rather than cutting the lid down further to form its recess, part the initial separating cut a little deeper (10–15mm), then glue a separate internal ring into the lid at that point to form the fitting recess instead. This avoids sacrificing another 3–4mm of matched grain purely to create the lip — worth trying on a future piece.
Wood Selection Notes
Long, thin sections near the top of the teardrop are easy to turn too thin without noticing — one earlier pōhutukawa attempt ended up too fragile at the top as a result.
Macrocarpa gave repeated trouble in practice pieces — prone to splitting, and small surface knots often hid larger, more disruptive knots just beneath the surface once turned into.
Rimu performed well and was used for both a practice piece and material discussed on the night.
A certain amount of loss to splits, knots, or mistakes is normal and expected — as Kevin put it, that’s simply where firewood comes from.
Notes
As a first demo, this one was always going to be ambitious to finish in the time available, and it was left partly refined rather than fully complete on the night — entirely normal, and well received by the room. A good candidate for a short follow-up demo once the internal-ring and template ideas above have had a chance to be tried out.
Notes compiled from the presenter’s own prep notes and a recording of the demonstration.
Club Meeting: 16 September 2026 Report by: Eoin Jury
Nicole’s mystery project begins with two blocks of wood, one about 40mm thick and the other 50mm thick, both turned down to about 160mm diameter with a spigot added to each. Put each piece in your chuck and flatten the face. They are then glued together with the spigots facing out. The wood type is optional, but in this case includes expensive wood purchased from Rosenfeld Kidson purloined from mum’s collection!
The shorter end is secured in the chuck, and lines marking 75 and 80mm diameter are made on the face, and then the face is rounded off from the join in the pieces through to just outside the 80mm line. The tailstock is disengaged so the spigot can be removed and a hole put in the centre with a 26mm Forstner bit, around 20mm deep.
Nicole then cut a groove with the parting tool around 5mm deep between the 75 and 80mm lines and rounded off the centre to the groove. The piece is removed from the chuck and the chuck replaced with one that can grip the piece by the 26mm hole just created. Now the bottom can be rounded off and spigot removed. With the bottom rounded and sanded, a light pencil line is made to mark 50mm from centre. This circle is divided with six equal sections and every second marked for drilling holes.
Now a 20mm square piece of wood about 80mm long is put into the chuck and rounded off. The dowel is marked at 10mm, 40mm and 55mm from end.
The end is rounded off from the 10mm mark to end. Between the 40mm mark to the 55mm mark, the piece is machined down to 8mm, then the portion in the middle is shaped down in a curve leaving a slight ridge at 40mm, then parted off at 55mm. Two more pieces the same are made.
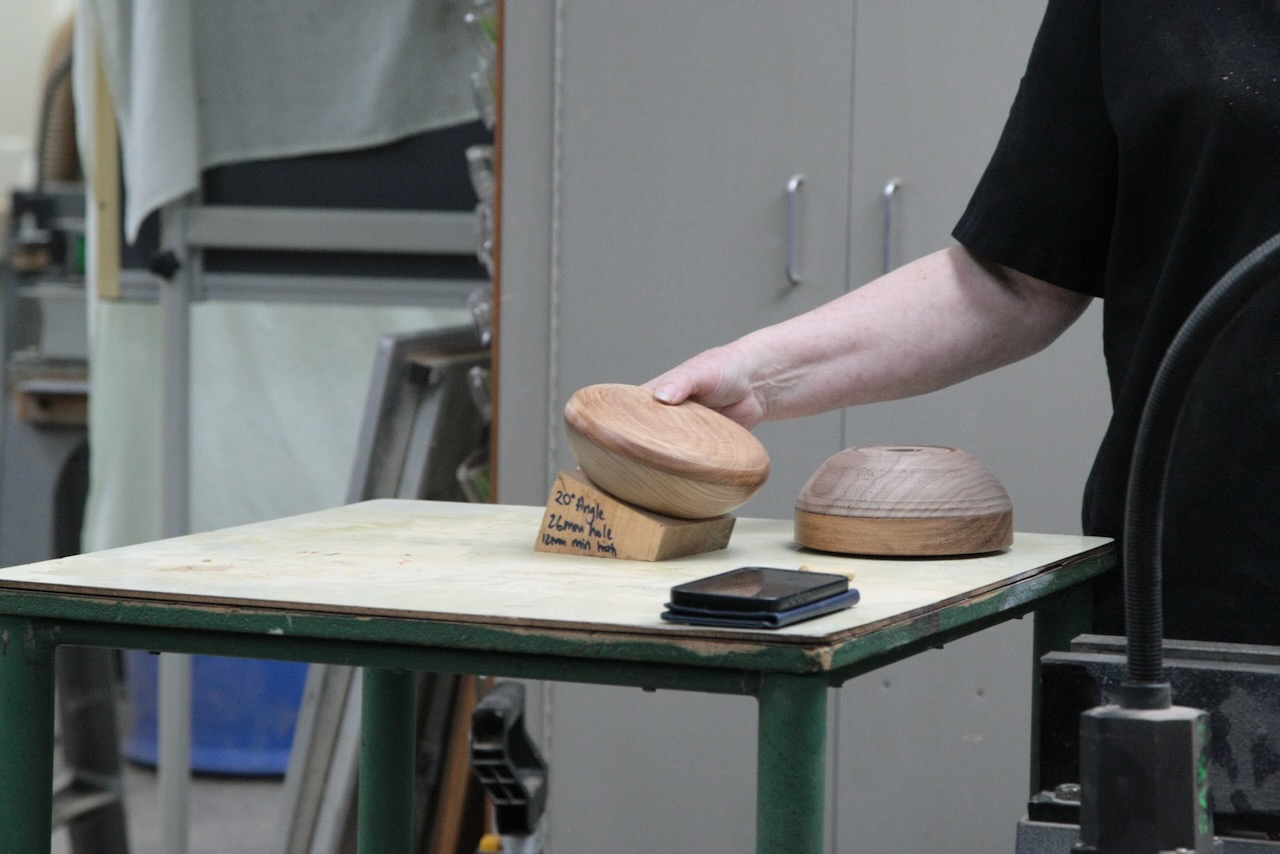
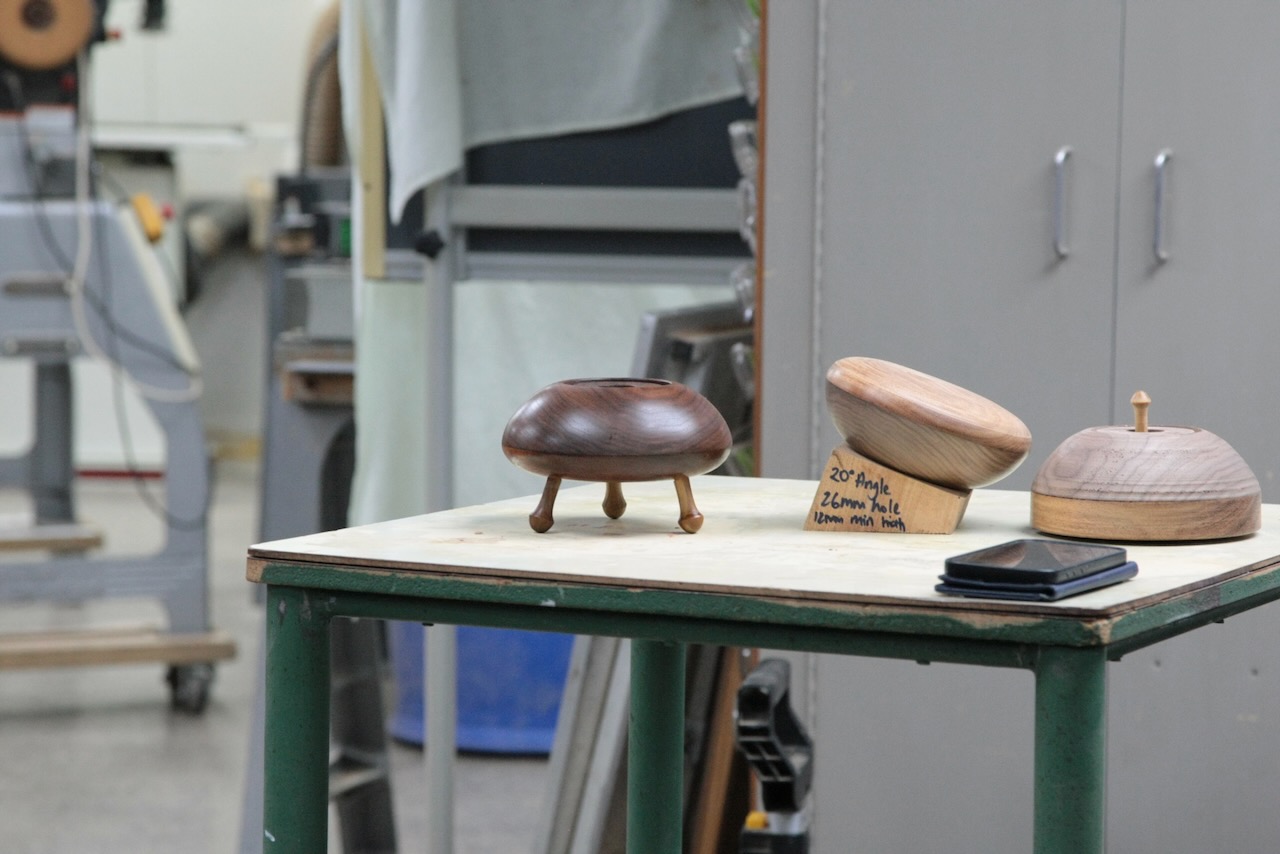
Nicole made a jig out of a block of wood with a 20˚ tilt on the top face and a 24mm dowel in the middle. The piece is put on the jig, base side up and a 10mm wide hole using a w-point wood bit is drilled in the drill press at every second mark to make 3 holes. (Depth of 20mm) The small dowels made in the previous step are inserted and it has legs!
A piece of pine approximately 120mm x 50mm is turned down to 40mm, then the portion from 60mm to 75mm is turned down to 24mm. Nicole rounded off the end and added some shaping to the middle part, sanded end and parted off at 75mm.
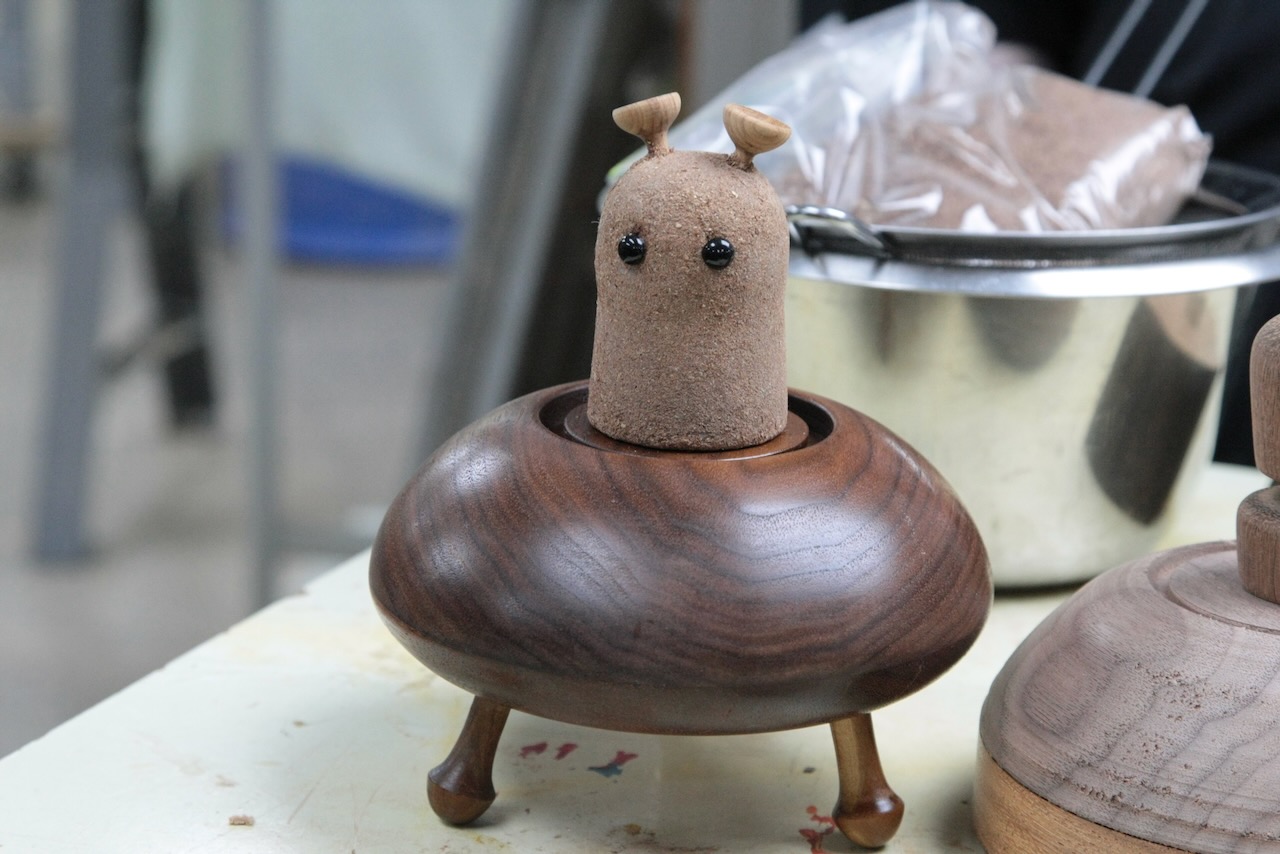
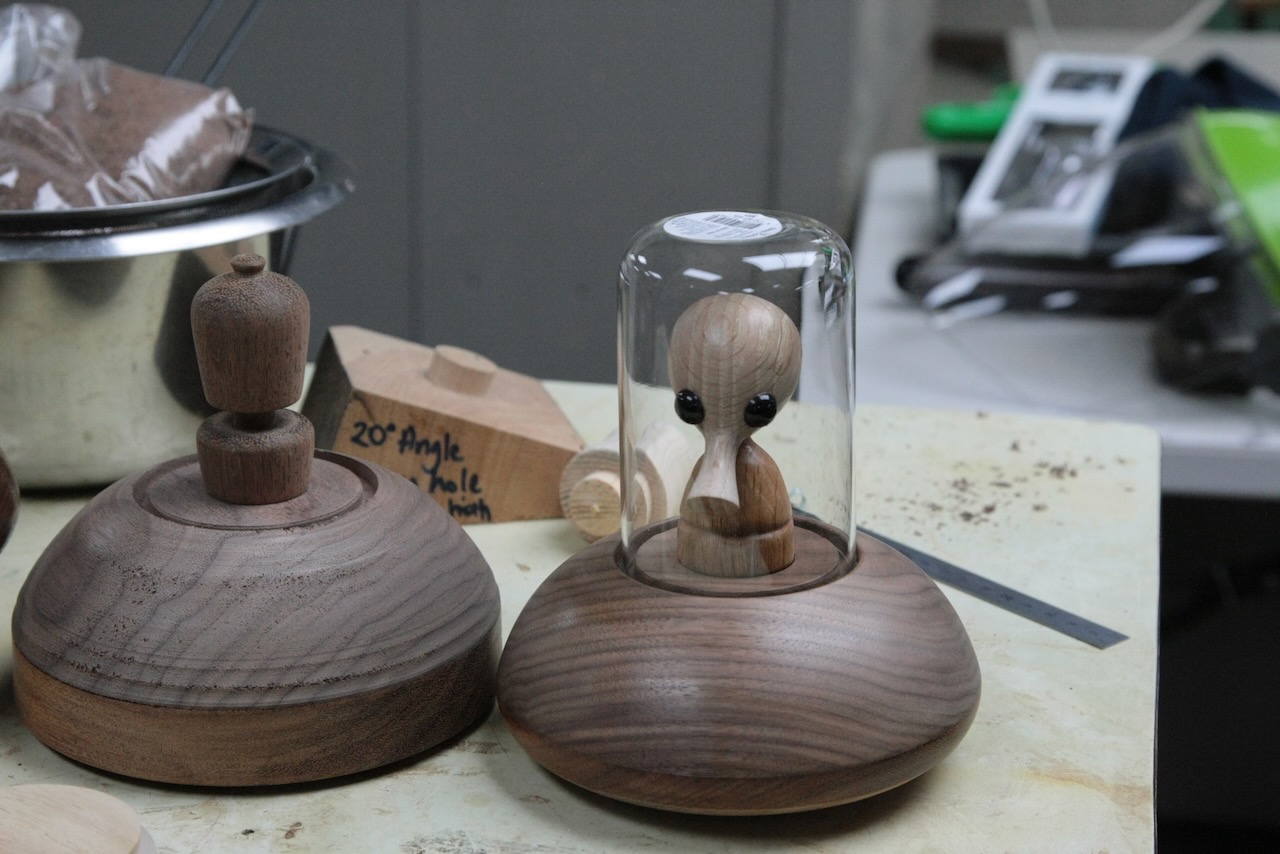
Nicole had some sawdust that she had sifted, by applying PVA to this piece, she could coat it with sawdust, and draw some eyes. This piece goes into the top hole of the main part (with legs), a small glass jar (purchased from Kmart) is inserted into the top groove and voila, we see a flying saucer!
Nicole also had some variations of the alien she had made earlier.
Club Meeting: 9 September 2026 Report by: Kevin the ai guy
Overview
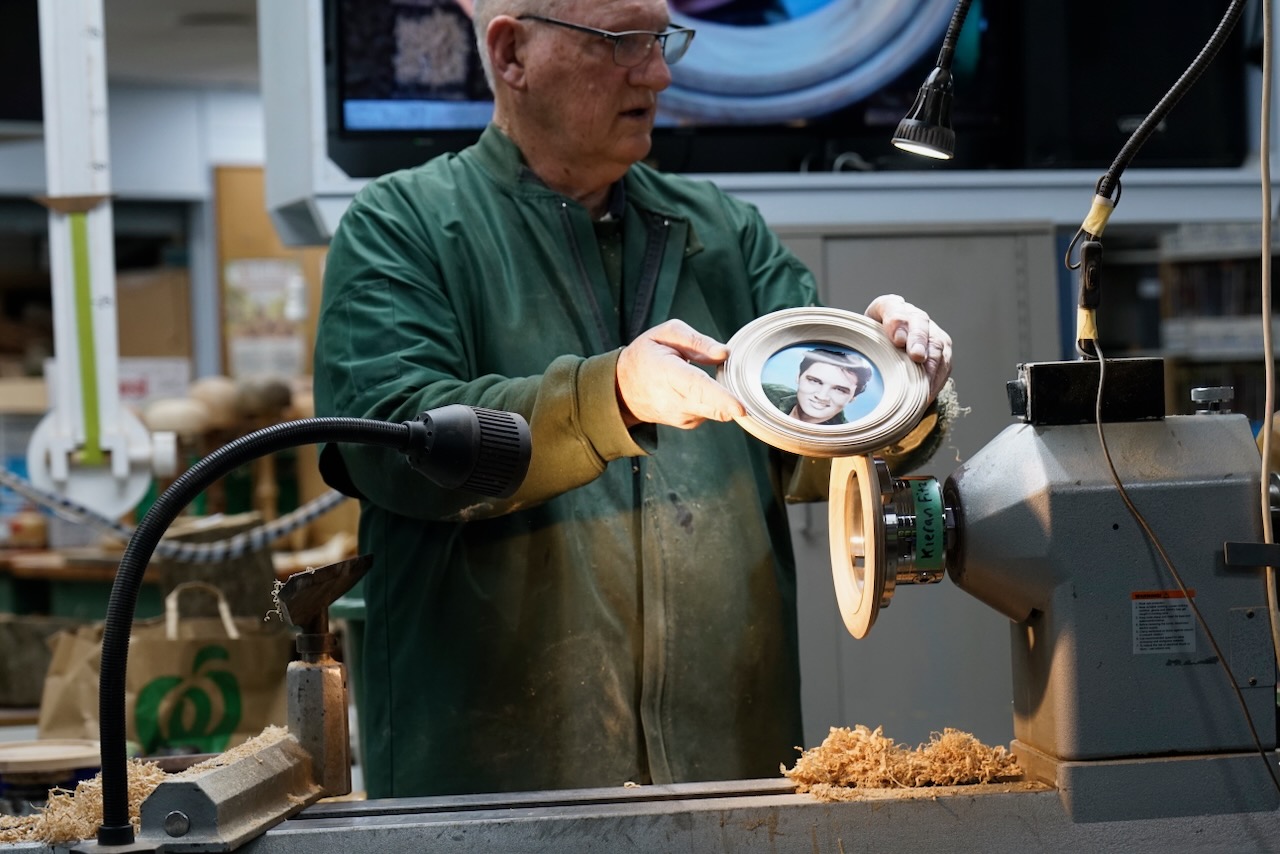
Kieran split this demo in two. The first half was an honest, in-progress look at hand thread chasing — a notoriously difficult technique he’d been practising for weeks without fully mastering, shared candidly warts-and-all rather than as a polished method. The second half was a quick, satisfying photo frame project, adapted from an earlier decorative “picture frame” plate design, included specifically so the demo finished with something complete.
Part 1 — Thread Chasing (Experimental)
Hand thread chasing cuts a screw thread directly with a handheld chasing tool rather than a jig. Kieran was upfront that after weeks of practice, results were still inconsistent — useful context for anyone tempted to try it expecting quick success.
Tools & Materials
Item
Notes
Chasing tools (male & female)
Carbatec sells sets in 10, 16 and 20 TPI (threads per inch). 10 TPI is very coarse/aggressive and generally too large for a small box; 20 TPI is very fine; around 16 TPI was suggested as the best all-round choice for box-sized work.
Recess tool
Cuts a clearance recess at the back of the piece so the chasing tool can be withdrawn before hitting the headstock end — without it, continuing to cut simply tears out the finished threads.
Hook tool / arm rest (optional)
Hooks over the main toolrest to give extra leverage pulling the tool into the cut. Kieran doesn’t own one and manages without, but noted it as a legitimate aid.
Diamond file
Used to sharpen the chasing tool — hone only the top face.
Wax / Ondina oil
Applied to the thread to help the tool slide rather than grab. CA glue is sometimes suggested to stabilise chippy grain, though Kieran hasn’t found it especially effective.
Timber
Needs to be hard and very straight, tight-grained. Trialled on the night/at home: swamp rātā, pōhutukawa, olive, titoki, camellia and black maire, all with mixed or partial success. Boxwood is considered the gold standard overseas but isn’t readily available in NZ. No NZ native timber has been reliably, repeatedly thread-chased by club members to date — puriri is considered the most promising candidate but still hasn’t been cracked.
Technique
Cut a slight chamfer on the leading edge of the piece first — this helps the chasing tool engage cleanly when starting the first thread.
Enter the cut at roughly 45 degrees and begin the first thread, then gradually rotate your hand/the tool handle around as you cut subsequent threads, until the tool is running parallel to the lathe bed once the full thread length is cut.
Cut a recess at the back of the threaded section before you get there, using a parting/recess tool — this gives the chasing tool somewhere to be withdrawn to once it reaches the end, avoiding tear-out.
Work at a low, consistent speed (around 280 RPM was used on the night) — speed affects how quickly the piece draws the tool in, and a comfortable, repeatable speed matters more than a specific number.
Listen as much as you watch — you cannot see thread breakout happening while the lathe is spinning, but a change in sound (a distinct “clunk”) is a reliable sign it’s occurred.
The female (internal) thread is harder to cut successfully than the male (external) thread.
To size a male thread to fit an existing female one: cut a test rebate at the front of the male piece until it just fits inside the female threads, then estimate and cut down to the matching depth, checking for a light “witness mark” appearing on the tenon as a sign you’re close to the correct depth.
Honest Assessment & Practical Notes
Kieran estimated it takes roughly 200 repetitions to build the muscle memory this technique relies on — it was described as requiring total concentration of sight, sound and touch simultaneously, more so than any other lathe operation he does.
Even with a well-suited timber, success is far from guaranteed on any given attempt — treat early results as practice, not a reliable process yet.
A 6mm-long thread section can mean roughly 20 turns to fully engage — too many for practical use.
Matching grain pattern between a threaded lid and its box is trial and error: screw the two pieces together fully, note how far the grain is out of alignment, remove that amount from one piece, and repeat until it lines up.
Part 2 — Photo Frame (Quick Finished Project)
Adapted from an earlier decorative “picture frame” style plate design, reworked into a functional photo frame. Made from a piece of recycled shelving timber on the night, though any suitable timber will do.
Roughing & First Mounting
Sand one face flat and mark the centre, then mount it against a glue block using a few dabs of hot melt glue — sufficient to hold it securely for light truing work.
Round the blank, working until the visible “shadow” cast by an out-of-round edge disappears, then continuing until any remaining flat spots are gone.
True up the face — it typically won’t be far out.
Mark and cut a dovetail-profile recess sized to fit your scroll chuck jaws, using a parting tool followed by a small skew to form the dovetail angle.
Cut a small cove or relief detail on the back edge— it makes the finished frame easier to pick up off a flat surface.
Second Mounting & Front Design
Remove from the glue block and remount by gripping the dovetail recess directly in expanding scroll chuck jaws (or press onto a shop-made jam chuck if you don’t have matching jaws) — either holds the piece securely and centred for front-face work.
Measure or eyeball from the back to locate where the chuck jaws finish, and scribe a circle marking the section that will later be removed to create the photo opening.
Divide the front face into two zones — an inner section and an outer border — to create a “picture frame” effect.
Turn the inner section as a shallow half-cove; treat the outer section more like a bowl’s rounded rim.
Leave a detail line between the two zones to visually separate them.
Check the remaining wall thickness in the recessed area with outside (figure-eight) callipers — around 3 mm looks good.
Creating the Photo Opening
Use a parting tool to remove the centre section. Reduce the lathe speed to around 500 RPM before breaking through. Work gently to avoid breakout on the back of the frame. Any breakout that may occur will not be visible anyway.
Finishing & Assembly
If the cutting technique is clean, very little sanding is needed at this stage — as little as two to three minutes in the demo.
Insert your photo from the back with a cardboard backing piece, then secure with small push pins (inexpensive T-pins from a craft/hardware store), pressed in by hand and lightly tapped home with a hammer.
For hanging: the simplest option is a small tack in the wall using the natural recess in the back of the frame. Or a standard D-ring picture hook can be fitted into the back instead.
Overall this is a genuinely quick project — roughly half an hour from a rough blank to a substantially finished frame, with only a couple of minutes’ sanding on top given clean tool work throughout.
Club Meeting: 2nd September 2026 Report by: Eion Jury
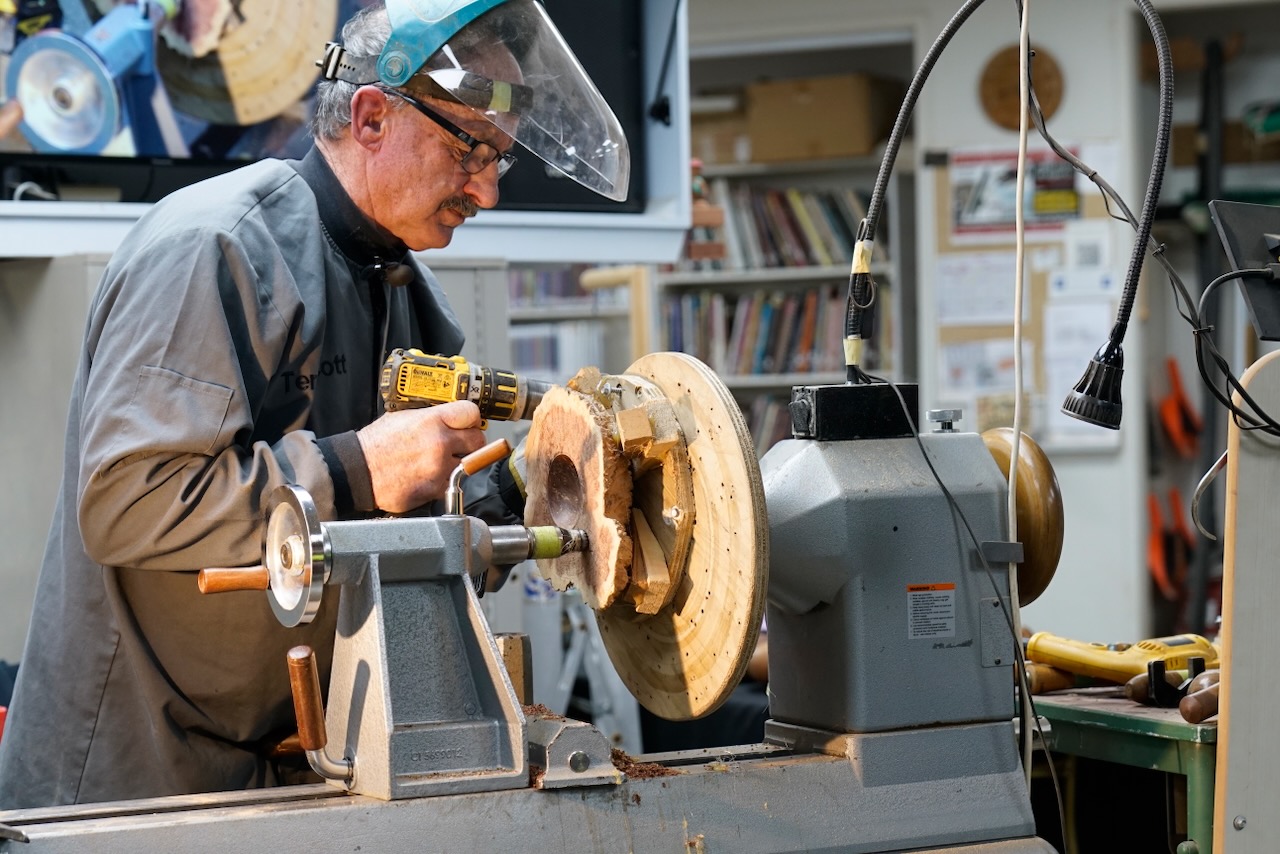
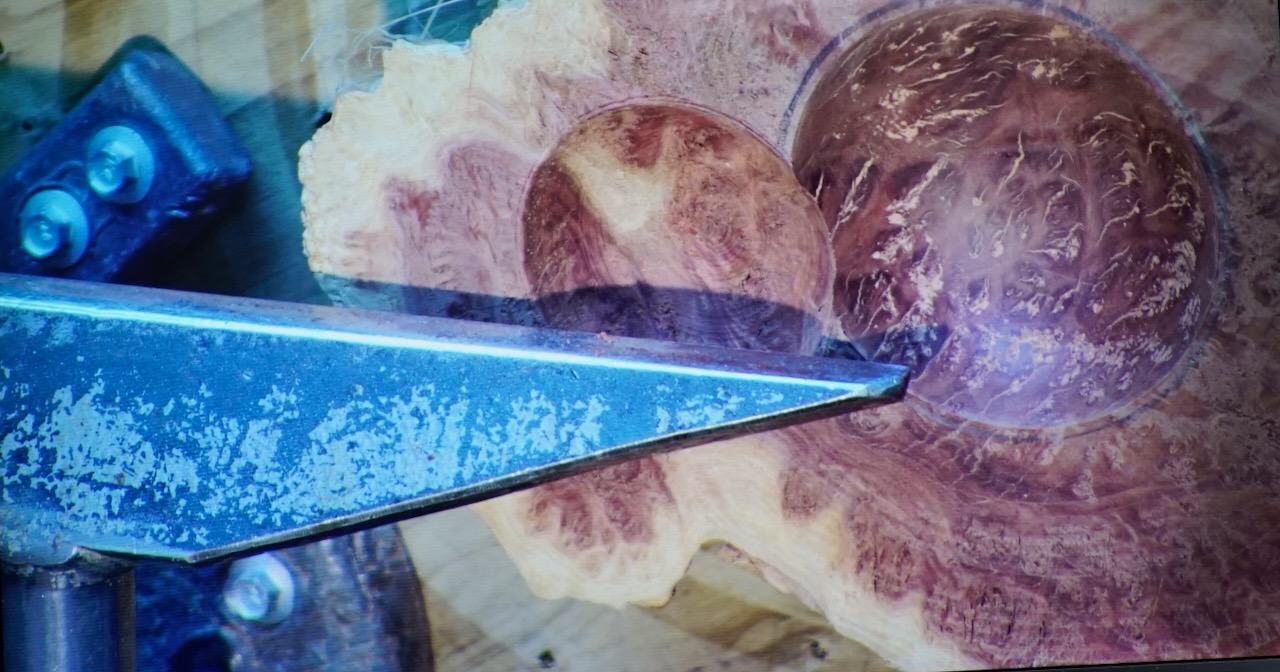
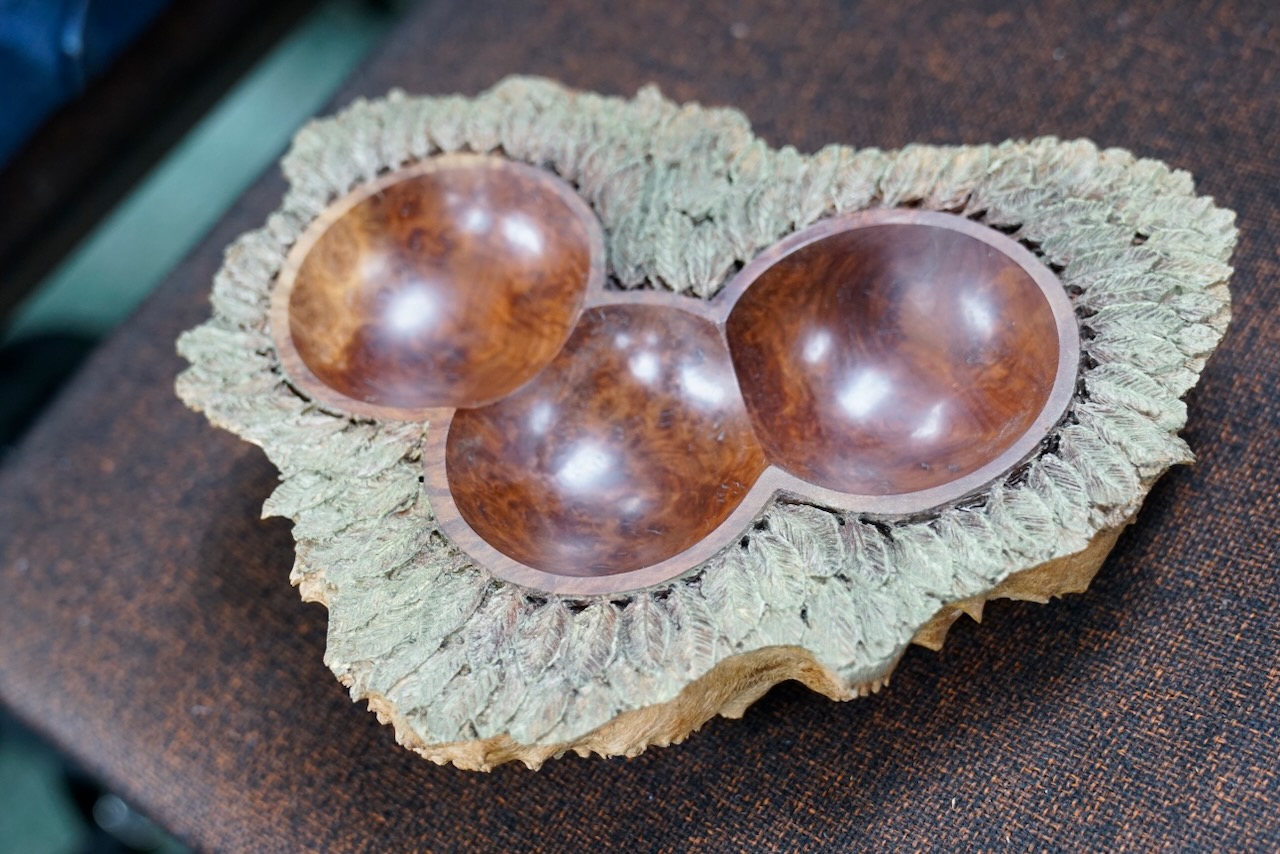
Terry Scott delivered a masterclass in creative burl turning, showcasing the signature technique he has refined over many years of woodturning— producing several overlapping, offset bowls from a single burl blank. The result is a sculptural, multilayered form that reveals both the raw exterior and the spectacular inner structure of Australian burl timber.
Understanding Burl Timber
Terry began with an explanation of what a burl (or burr) actually is: a tree’s response to stress or injury, where dormant buds erupt into chaotic, swirling grain. This can be triggered by insect damage, animals rubbing against the trunk, fire, or repeated pruning.
The burls used on the night were Red Mallee and coolabah, sourced from the Northern Territory — a region where land clearing for agriculture means burls are often removed as a byproduct. Red Mallee in particular is prized for its intense figuring and colour.
Importing these burls is not for the fainthearted: both Australian and New Zealand authorities require extensive paperwork, and once they arrive, they must be heat treated, leaving them hard as stone.
Why This Technique Exists
Terry shared the story that sparked the development of this method: a customer wanted a raw Red Mallee burl displayed with the natural edge facing upward. Terry realised he needed a way to turn only one side of the burl while preserving the untouched exterior — leading to his nowdistinctive approach of singlesided, overlapping bowl turning.
The result is a piece that allows viewers to enjoy both the rugged natural burl and a “lenslike” window into its inner beauty.
The burl wirebrushed clean to ensure good glue adhesion.
The plywood “slide” was attached to the disc using screws around the perimeter.
Wedges inserted to level the face, secured with industrial hotmelt glue (famously purchased at a SAWG silent auction!). Domestic glue guns work, but the mounting surface must be preheated with a heat gun.
Once the bowl positions were planned — typically offset by half the bowl diameter with around 10 mm overlap — the burl mount was pressed against a plywood faceplate (preferred over MDF because screw holes don’t raise fibres).
The tailstock was brought up, wedges adjusted, and the mount screwed firmly to the faceplate. Finally, lead counterweights were added until the assembly was balanced.
Cutting the Bowls
With the burl balanced and secure, Terry demonstrated the cutting sequence:
Flatten the face at low speed.
Use a skew chisel to mark the bowl’s perimeter — creating a crisp barrier.
Switch to the bowl gouge, beginning at the outer edge with the flute at 10 o’clock, rotating to 2 o’clock as the cut approaches centre.
Stay on the bevel at all times.
Coming off the bevel near the thin “wing” sections risks a catch and destroys the crisp intersection line.
4. Maintain a true spherical shape — mismatched curves cause wobbly intersection lines.
5. Finish with a shear/negative rake scraper, ground like a skew for a safer, cleaner cut.
6. Sand with the lathe stopped to preserve the crisp overlap lines.
Each bowl requires the mount to be unscrewed, repositioned, rebalanced, and cut again.
Finishing & Embellishment
Once all bowls are complete, wedges and glue can be removed with a heat gun — or left in place if further carving is planned. Terry discussed several finishing options:
Leave highly coloured or figured burls plain so the timber speaks for itself.
Add carved or pyrography scored borders to create a picture frame effect.
Use rotary carving bits for fine sculptural detail (accepting that burr bits are consumables).
Negative rake scrapers — originally adopted from Australian turners — excel in burl work and are now widely available.
Notes & Tips from Terry
The technique works on plain timber too — burl simply adds drama.
Shallow overlapping rings or craters can mimic the effect without full hollowing.
Practise cheaply on long straight stock (e.g., fence posts) using a scroll chuck with two jaws removed.
Advanced variation: a centre hollow form intersected by another bowl — still experimental.
These burls are remarkably stable and can even be blowtorched while wet without cracking.
To release the finished piece from the backing board:
Heat gun softens glue, or
Freeze the assembly — frozen hotmelt glue becomes brittle and pops off cleanly.
Terry’s Philosophy
Terry emphasised the importance of developing a personal signature rather than copying techniques directly. His decorations in combination with the turning style was something he hadn’t seen elsewhere when he began — and it has since inspired others.
Club Meeting: 19 August 2026 Report by: Jacqui Oxenbridge
The journey all started at Turnfest this year with Len Mengel’s demo showing alternatives to wobble chucks.
Other inspiration came from Eli Avisera with his turned wine bottle and balance glasses and Radek Teterycz’s extreme turning where most of his work is done on the lathe – worth a look on Facebook or Instagram.
Part one of the demo will be showing the use of Colin’s Vicmarc Eccentric Chuck with a 40mm cup chuck and ball. He also has a separate ball (gimbal) that can attach to a Faceplate.
To use the “eccentric chuck” we first need to shape a taper that will fit in the ball/gimbal but not bottom out in the chuck. The gimbal can be moved inside the cup chuck when the appropriate grub screws are loosened off. Note: the blank is held in only by friction.
The chuck is a little confusing with multiple grub screws requiring different Allen keys. Some are marked with a line – these have a pin on the end which can go through corresponding holes in the ball to hold it in position when it is square (straight). The other grub screws are flat and tighten the chuck to the outside of the gimbal at various positions when turning off centre.
Place the blank between centres – using a smaller drive centre with a Steb live centre so if have a catch the mini drive centre point does less damage to the blank.
Round off the blank sufficiently that a taper can be made. To help ensure the taper is going into the ball/gimbal square, and how far in the taper has gone, can draw lines on the blank.
Push the taper in to the chuck/gimbal. If too large, turn more off the taper. Use a mallet to seat the blank tightly.
Tighten up the grub screws on the chuck to secure the gimbal.
Put the chuck on the lathe – note that the chuck has a dedicated thread.
Bring up the tailstock, begin to shape the blank.
When the tailstock is removed to true up the end, and as you hollow the end grain with a spindle gouge to make the goblet REMEMBER to avoid aggressive cuts across the blank as it is relatively easy to pull the blank out of the chuck.
Once the goblet is hollowed, if desired, it is possible to use the tailstock in the hollow to stabilise the blank while cutting the outside shape of the goblet/stem/foot. Use a skew and spindle gouge to shape.
Ideally, you will know what shape you want to make before you start turning – it can be helpful to have a photo or drawing of your intended shape.
Once the goblet is complete, carefully sand and finish it as it is difficult to recentre the piece once you start off centre turning.
Now loosen off the screws on the chuck that are holding the gimbal in place so that the blank can be shifted. The movement is small and it is important to check that the base of the goblet is over the centre of the next section that will be turned. To check, move to where you think it should be, tighten 2 screws in the chuck to the gimbal and rotating the blank, draw a line to allow you to approximate where the centre will be. Once in the correct position tighten all the grub screws holding the gimbal in place.
Start to turn but before going too far, check the pencil mark again. There must be some of the pillar remaining to support the top cup. Adjust the position if required.
Working away from the goblet bring the next section into round. Use a spindle gouge and skew to remove surplus timber in the grooves. Once the desired shape is complete carefully sand this section only – do not attempt to sand the 1st goblet.
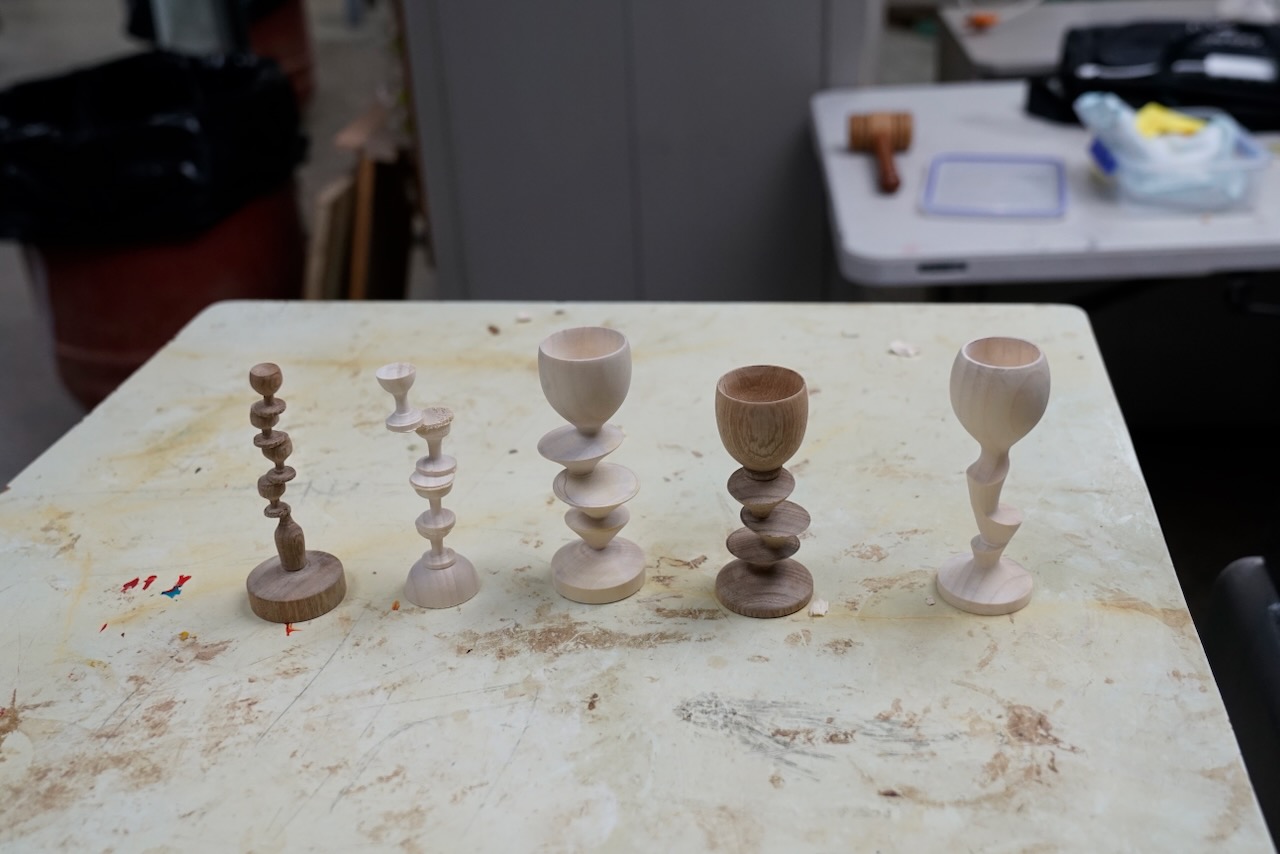
Repeat the process moving the blank, checking where centre is, turn the section – ideally keeping the diameter of each shape the same, sand.
Two things are important for success – your tools are very sharp and the timber has a straight grain and low tendency to split. Gingko was a good choice.
Sorby also have a Wobble Chuck which uses standard 50mm jaws. In this chuck the piece in the jaws rotates so changing the angle of the piece. The angle can be repeated so that less guesswork is required as to where to move the blank. This also has a worm screw to retain the work, or the screw can be removed and the faceplate attached to larger blanks.
Part two of the demo will be making stacked cups without a wobble chuck.
Mount the blank between centres, round off part of the blank. Turn a hemisphere (ball) on one end of the blank – this does not need to be super accurate but does have to have clearance so that it will fit into a set of jaws. For the demonstration used Nova 35mm spigot jaws with the serrated teeth for a powerful grip on the blank.
Put the turned ball into the spigot jaws. Can now adjust the position of the blank (ball and socket rotation).
The first time the blank is moved off centre it is possible to use the live centre in the tailstock to show where centre is to measure the offset. An alternative that could be use would be a laser pointer in the tailstock.
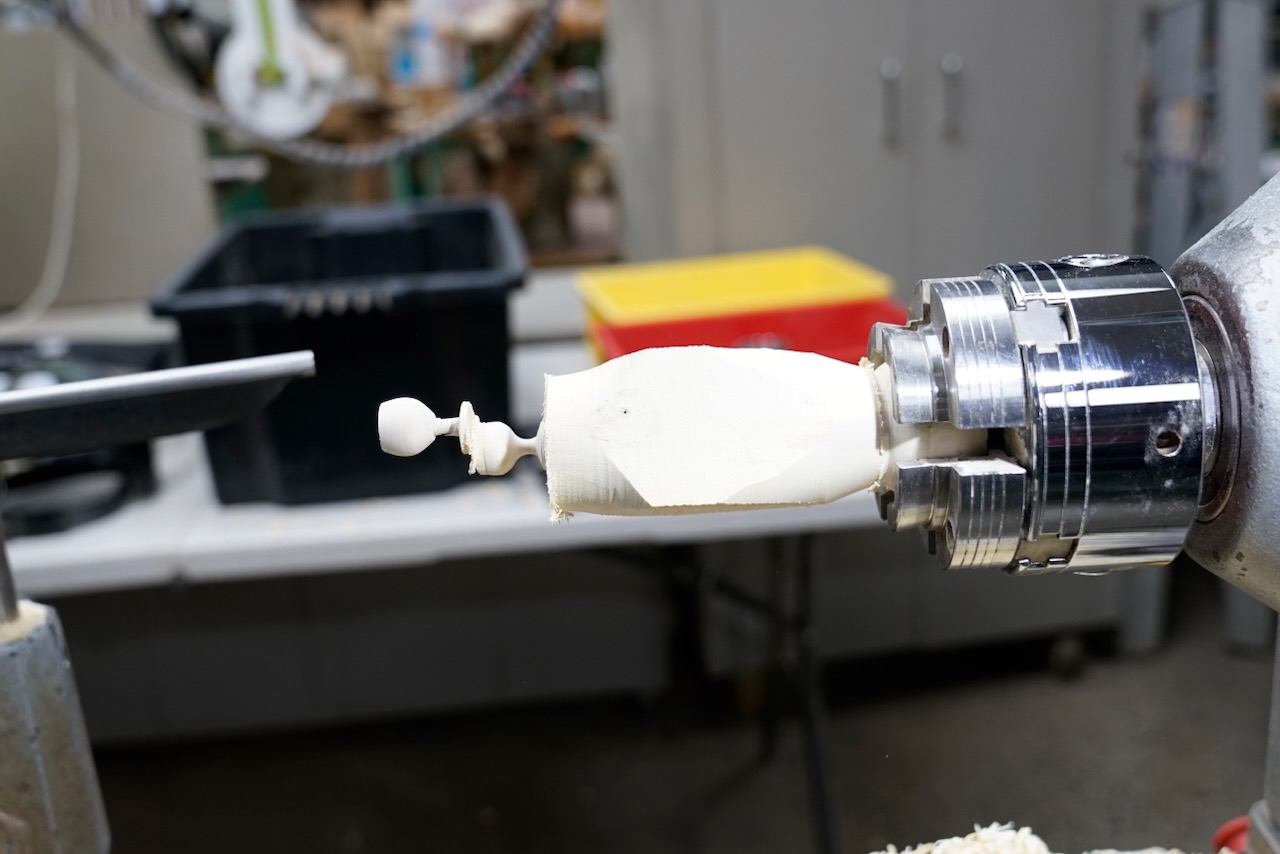
Start shaping the blank with a spindle gouge or for quicker bulk removal can use a skew or parting tool. Cut the length required for the first cup, continue until you get to the final diameter of the cup before start shaping the stem to avoid breaking the top off the cup! Once have shaped cup, stem and base – sand – very carefully.
Note: it is very important to have good light, contrasting colours on the lathe bed can be helpful.
Finish the top surface of the next section (closest to the headstock) before moving on to the next goblet.
Tilt the blank (tiny offset only). Where two “offsets” meet they will be angled at each other.
Use a pencil mark to work out approximately where centre is – needs to be under the existing cup. As with demo 1 – begin to cut but then check and reposition if necessary.
Tidy up the excess under the goblet foot with a skew or parting tool cutting in very carefully at an angle.
Aesthetically it is best to replicate the height of the goblets – could use a vernier to check.
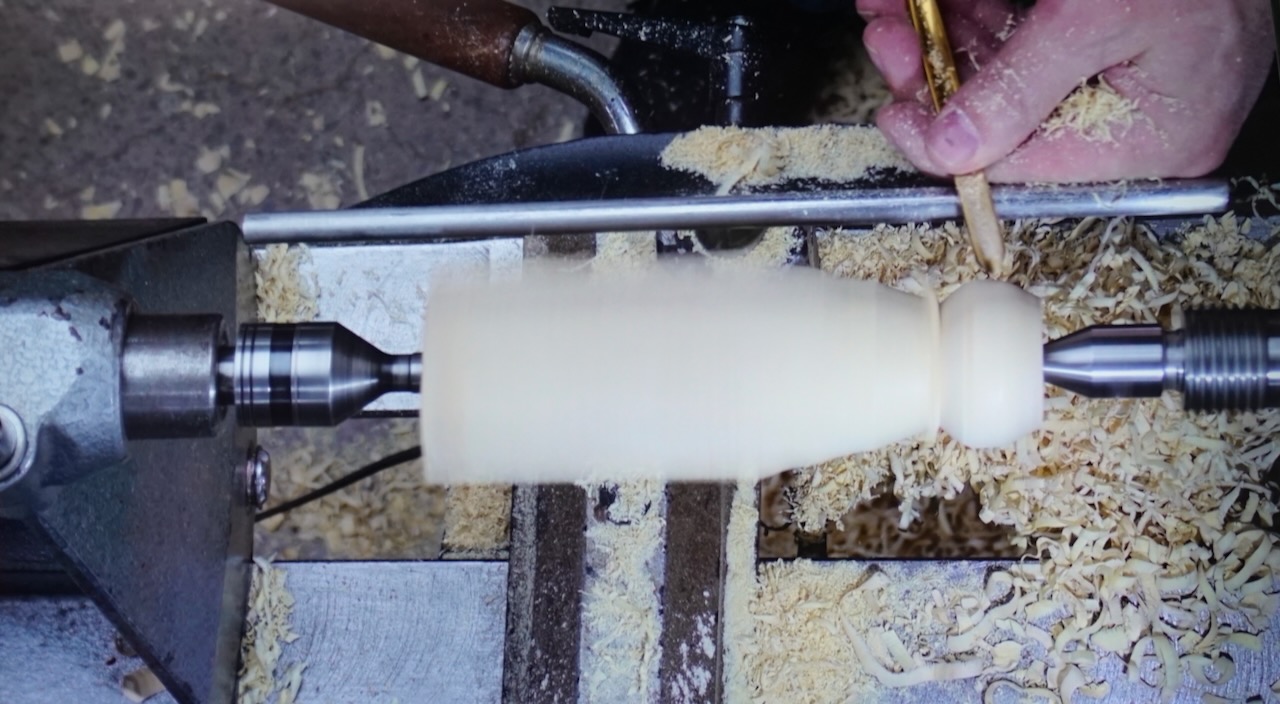
Round off the same length tip to base as the first goblet then with a small spindle gouge or thin parting tool, shape the next goblet. Sand before changing the offset.
Repeat until you run out of blank, it breaks or you’ve got a piece you like!
Club demonstration — Wednesday 12 August | Presenter: Julie Gannaway (North Shore Woodturners / NAW)
Overview
Julie ran through a range of simple, low-cost ways to fill cracks and voids and to add decorative inlay to turned pieces — from everyday coffee grounds through to metal powders, coloured micro-pigments, and inlaid wire. The session was explicitly framed as experimentation rather than a single “correct” method: several techniques shown had mixed results on the night, which Julie treated as useful material in its own right. Samples up to ten years old, including well-used cheese boards and outdoor pieces, were passed around to show how each technique holds up over time.
Materials & Tools
Material / Tool
Notes
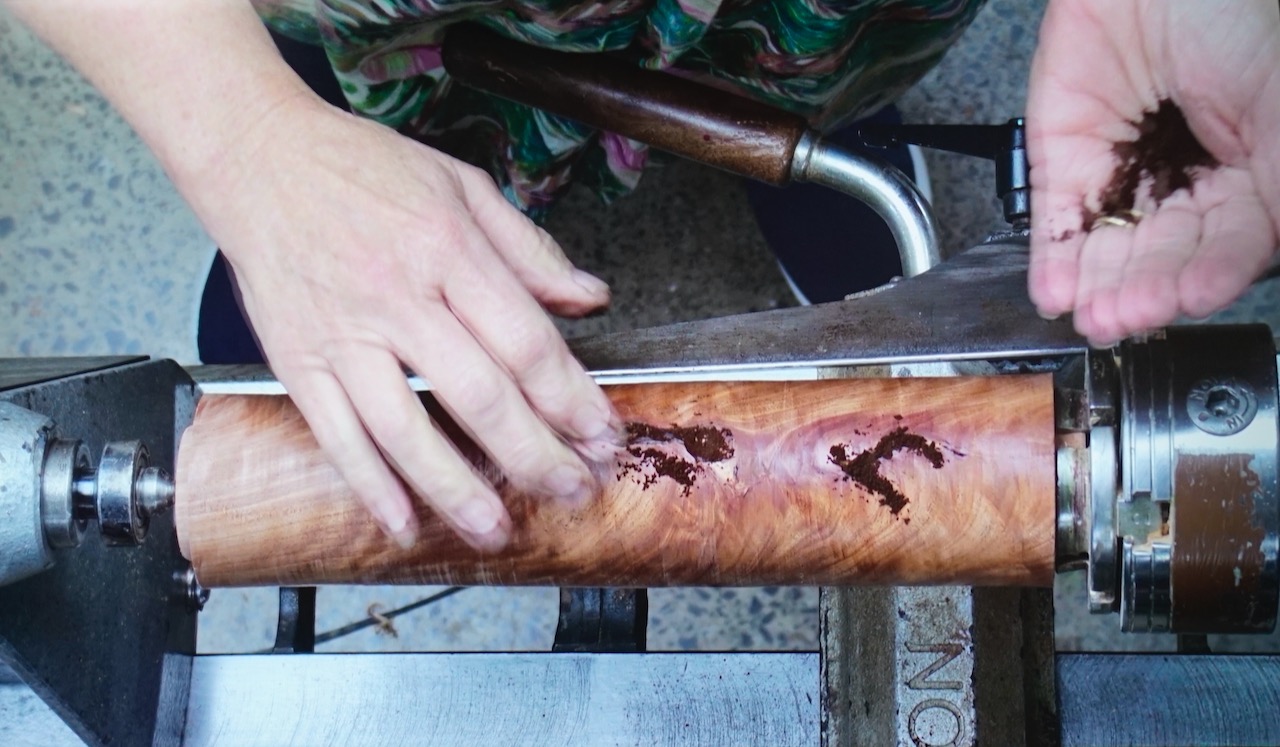
Ground coffee
Perked coffee, ground extra fine on a second pass — cheap, dark brown, works with most timbers
Cyanoacrylate (super glue)
Fast-curing; used to bind coffee, metal powders and wire; toxic fumes — ventilate and avoid sanding without a respirator
5-minute epoxy
Slower cure, doesn’t generate heat like super glue — better suited to heat-sensitive powders (e.g. aluminium) and bigger voids
Metal powders
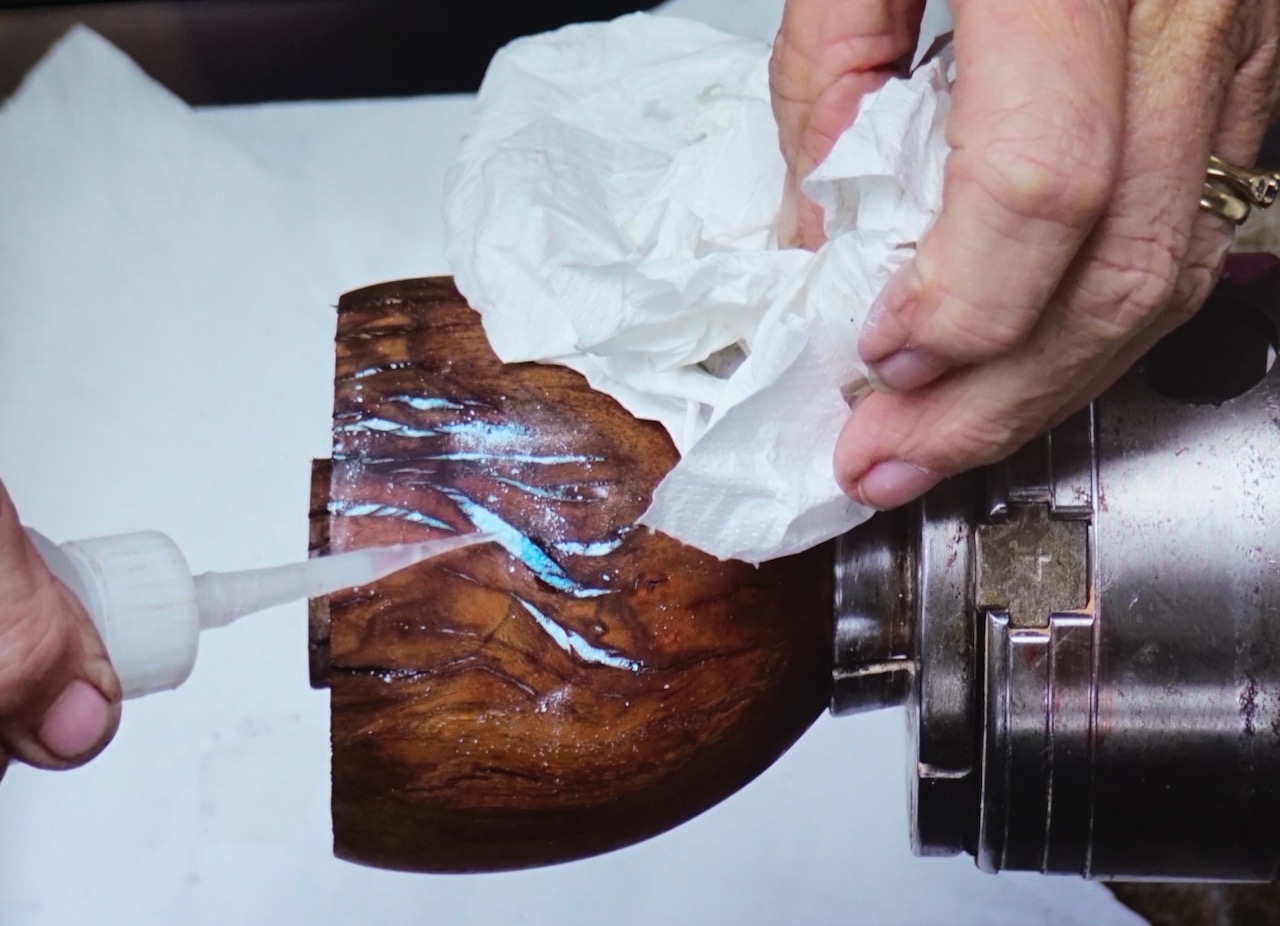
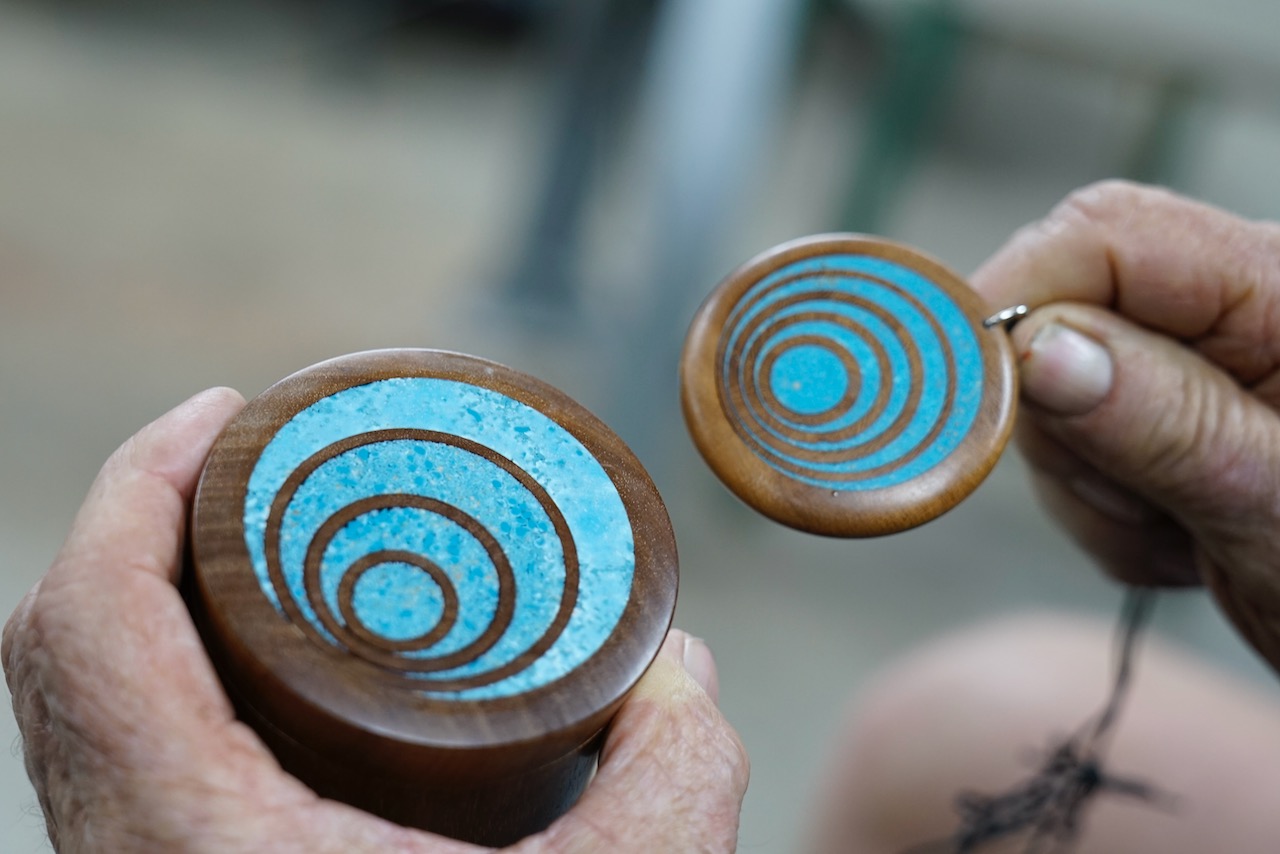
Brass, aluminium, copper and turquoise (turquoise available in a couple of grit sizes plus a fine powder)
Micro/mica powders
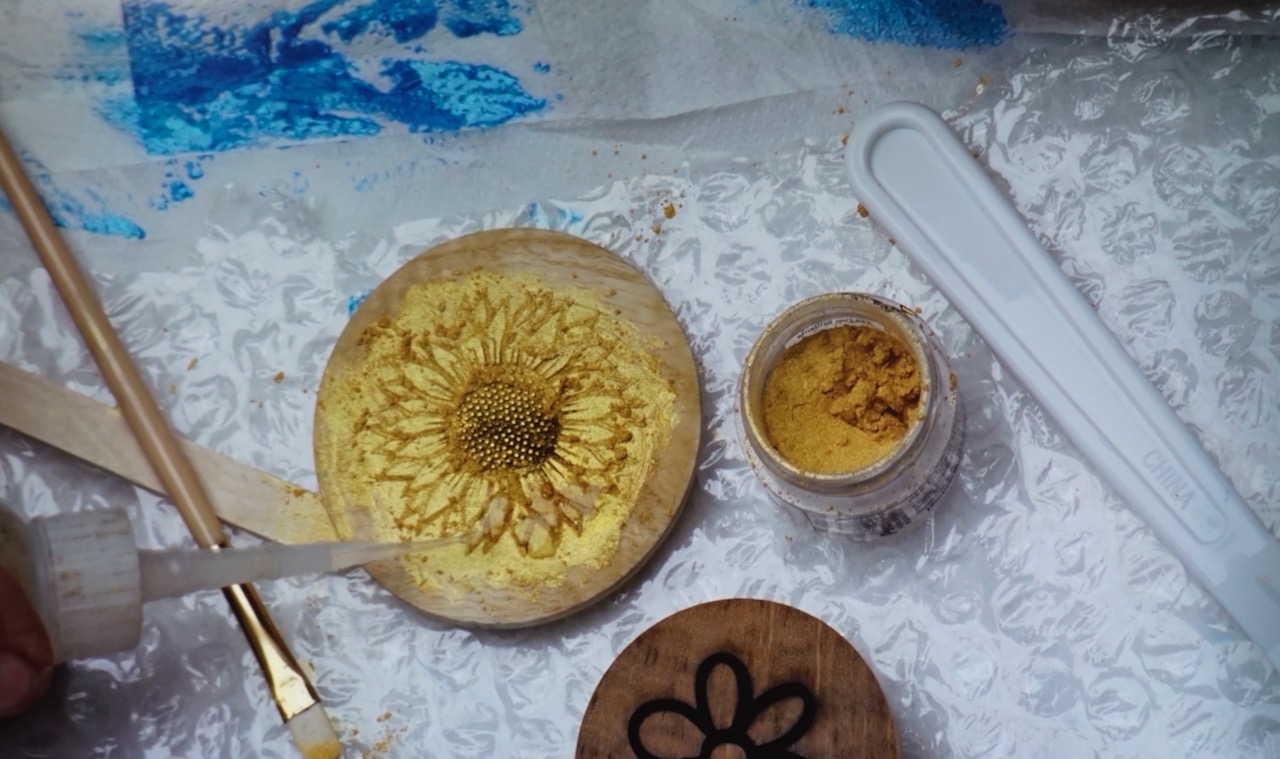
Fine-pigment powders (craft/hobby suppliers, e.g. Carbotex) in a wide colour range, used in pyrography or laser-engraved grooves
Acetone
Keep on hand as a safety item — releases super glue from skin/tools
Application tools
Fine-tip applicator nozzles that come with super glue bottles; a cocktail stick or similar for working powder in (not fingers); insulin-style syringes for very fine, controlled super glue application; a small paintbrush for moving micro-powder
Wire (for wire inlay)
Solder wire or copper wire, in a couple of thicknesses
Parting tool(s)
Sized to match the wire thickness being inlaid
General Safety Notes
Super glue fumes are toxic — work with adequate ventilation.
Wear a respirator when sanding filled/inlaid pieces, particularly with metal powders.
Use a stick or similar tool to work powder into glue — not fingers, both to avoid gluing yourself and due to toxicity.
Keep acetone close by to free glued fingers/tools if needed.
Seal the surrounding wood before applying super glue — unsealed grain will wick the glue and leave visible stain lines.
Technique 1 — Filling Cracks with Coffee
Seal the wood around the crack first — unsealed super glue will stain and telegraph through the surrounding grain.
Use finely ground coffee (perked coffee, run back through the grinder for an extra-fine grind). The dark brown tone suits most timbers.
Pack coffee grounds into the crack, then apply thin cyanoacrylate (super glue) through a fine applicator tip, letting it wick down into the grounds.
For bigger voids, pack with sawdust first, then coffee on top — coffee is cheap enough to use generously regardless.
Avoid accelerator sprays where possible — they can trap voids under the surface that only show up once you turn back into the fill.
Once cured, rub over with a finger — this grinds the coffee finer still and helps you feel out any remaining fine cracks.
Black-tinted super glue (available from club suppliers) is a simpler alternative to coffee on dark timbers and can read as natural grain. On lighter woods the coffee’s brown tone was generally preferred.
Longevity: samples shown included a cheese board with a ten-year-old coffee-filled crack, still sound after years of use and washing — provided the filled area isn’t load-bearing/structural, as timber movement can eventually reopen a crack regardless of fill.
Technique 2 — Metal Powder Inlay
Available powders: brass, aluminium, copper, and turquoise (turquoise comes in a coarser grit and a fine powder — grit can be used first to fill bulk, with powder used to fill remaining gaps).
Applied the same way as the coffee technique — pack the powder, then feed in thin super glue.
Apply in thin layers rather than all at once. Powder applied too thickly can leave a hardened surface film with loose, uncured powder still trapped underneath.
Caution with aluminium and pewter powders specifically: cyanoacrylate curing generates heat, and can exceed the melting point of these metals, leaving a dull, oxidised finish instead of a bright metallic one. Five-minute epoxy (which doesn’t generate heat) is a better binder for these two powders.
Copper and turquoise powders were shown as reliable, attractive fillers for burl voids and fissures — examples included a filled burl disc used as an inset panel and a decorative box lid using mixed turquoise grits.
Technique 3 — Micro-Powder (Mica) Inlay in Engraved Grooves
Cut fine decorative grooves using pyrography, or have a pattern cut with a laser engraver (settings — speed, heat, power — need adjusting per timber species).
Fill grooves with coloured micro/mica powder (a wide colour range is available from craft/hobby suppliers).
Bind with either super glue or 5-minute epoxy — both were demonstrated side by side for comparison. Epoxy was found generally easier to control and better suited to larger fills; super glue suited smaller, finer work.
A small paintbrush is useful for moving and placing micro-powder precisely, since it’s very fine and prone to going everywhere.
For very controlled, fine application of super glue (rather than a full applicator-tip stream), an insulin-style syringe gives much finer, drop-by-drop control — useful for filling narrow grooves one ring/section at a time without overflow.
Where a design has multiple colour zones, mask off completed sections before adding the next colour, or work from the centre outward, to avoid muddying colours together.
Once cured, sand back carefully — excess glue/epoxy on the surface cleans up easily, but avoid sanding through the full depth of shallow grooves.
Julie noted this technique is still a work in progress in her own practice — several samples shown had inconsistent results (air bubbles in epoxy fills, colours bleeding between sections), included deliberately to show realistic outcomes rather than only best-case results.
Technique 4 — Wire Inlay
Select wire (solder wire or copper wire both work; two thicknesses were shown).
Measure the wire’s thickness — this determines the groove size needed. Cut the groove slightly bigger and deeper than seems necessary, as it typically needs to be more generous than expected.
Cut the groove using a parting tool sized to suit — have a couple of parting tools of different widths on hand to match different wire gauges.
Seal the wood before gluing (as with the other techniques).
Lay the wire into the groove with super glue, working it in with patience — the first section takes a moment to tack down, after which the rest follows more easily.
Once glued, peen/hammer the wire to spread and flatten it into the groove, fully filling the channel; a smooth file can also be used instead of a hammer for a flatter, more finished face.
Trim any excess length once secure, then true up on the lathe.
Durability: Julie’s original outdoor coffee table inlay pieces lasted roughly eight years outside before the surrounding timber eventually cracked — notably, the wire itself stayed firmly in place the entire time.
Variations mentioned: twisted wire (by hand or with a drill for a tighter, more even twist) for a decorative pattern; aluminium powder can be used to dress/fill a slightly proud joint in the wire before final finishing.
Closing Notes
None of these techniques are presented as the only or “correct” way — Julie encouraged experimenting and adapting them to individual style and the piece at hand.
Keep a small dedicated box of filling/inlay supplies near the lathe so a crack encountered mid-turning can be dealt with immediately rather than becoming a separate trip/session.
Bringing imperfect or “failed” examples to a demo was called out as valuable — seeing what goes wrong is as instructive as seeing a finished piece.